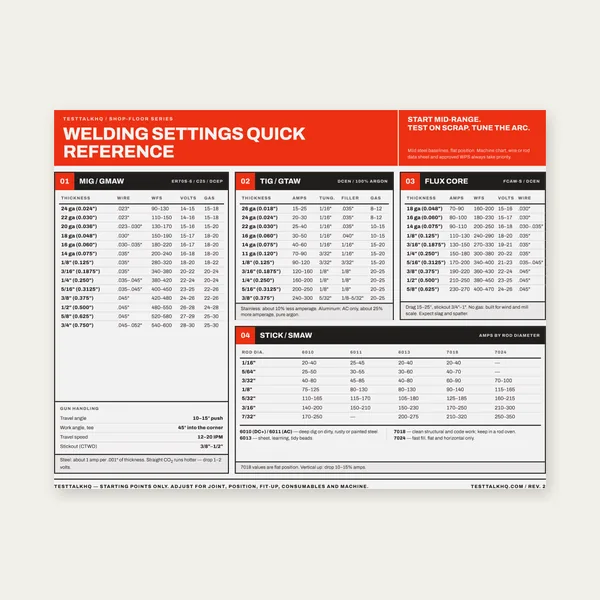
Welding Reference Card
One page. MIG, TIG, stick and flux core settings by thickness.
$3.99
BuyDiameter, tip prep & collet/cup by amperage
Match tungsten diameter to your amperage window and current type using AWS A5.12 published ranges — then get tip geometry and cup guidance. Companion: Tungsten Electrode Guide.
| Diameter | DCEN | DCEP | AC balanced |
|---|---|---|---|
| 0.040" (1.0 mm) | 15–80 A | N/A | 20–60 A |
| 1/16" (1.6 mm) | 70–150 A | 10–20 A | 60–120 A |
| 3/32" (2.4 mm) | 150–250 A | 15–30 A | 100–180 A |
| 1/8" (3.2 mm) | 250–400 A | 25–40 A | 160–250 A |
| 5/32" (4.0 mm) | 400–500 A | 40–55 A | 200–320 A |
| 3/16" (4.8 mm) | 500–750 A | 55–80 A | 290–390 A |
Source: AWS A5.12 typical ranges as published by electrode manufacturers for thoriated/ceriated/lanthanated (argon). Pure tungsten AC balanced windows are lower — the calculator applies that reduction when Pure is selected. Always verify against your electrode package chart.
One page. MIG, TIG, stick and flux core settings by thickness.
$3.99
Buy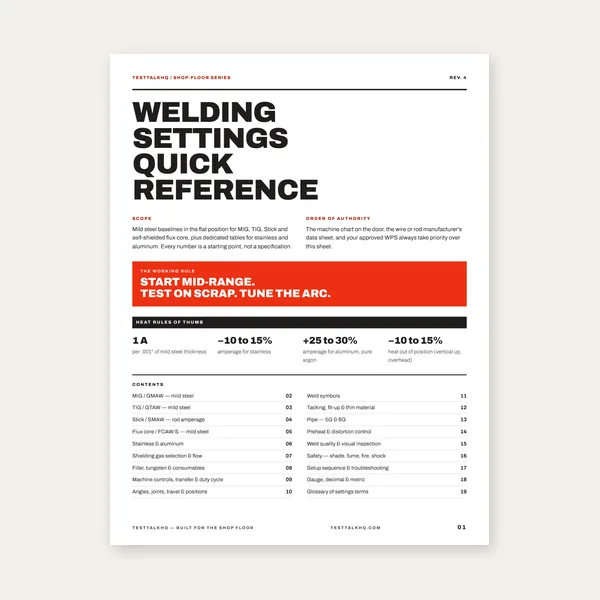
19 pages. Four processes, stainless and aluminum, symbols and inspection.
$12.99
Buy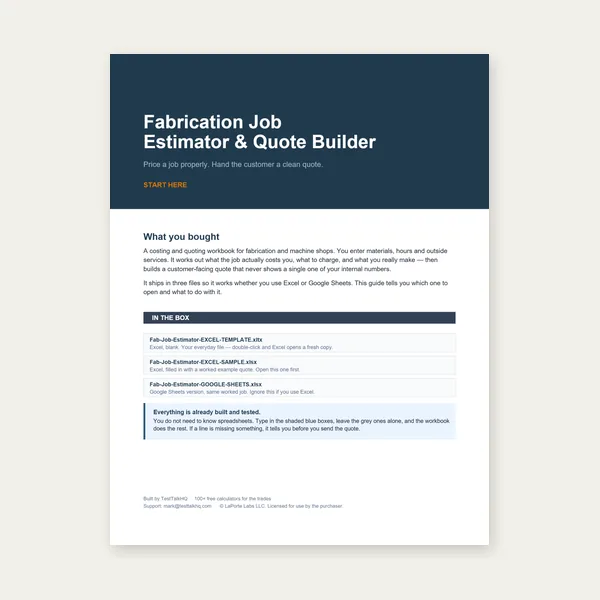
Price the job, then hand over a quote with no internal numbers.
Excel or Google Sheets. Best on a computer.
$29.00
Buy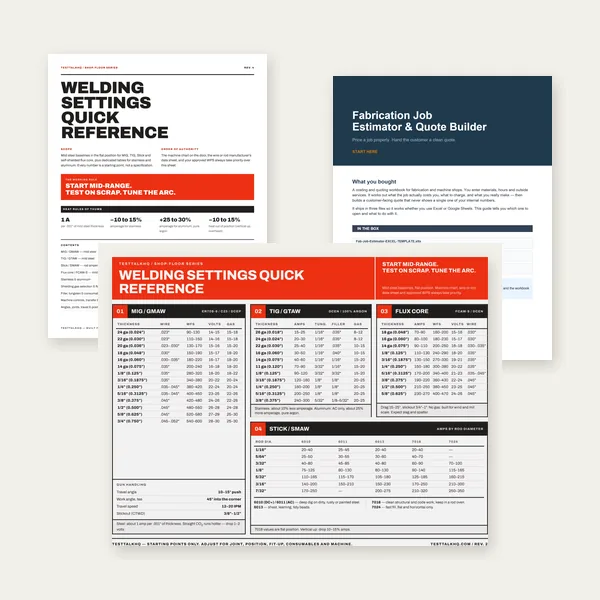
Card, 19-page guide and the estimator workbook. All six files.
Excel or Google Sheets. Best on a computer.
$34.99
$45.98 if bought separately — save $10.99
BuyCheckout opens here — you stay on this page.
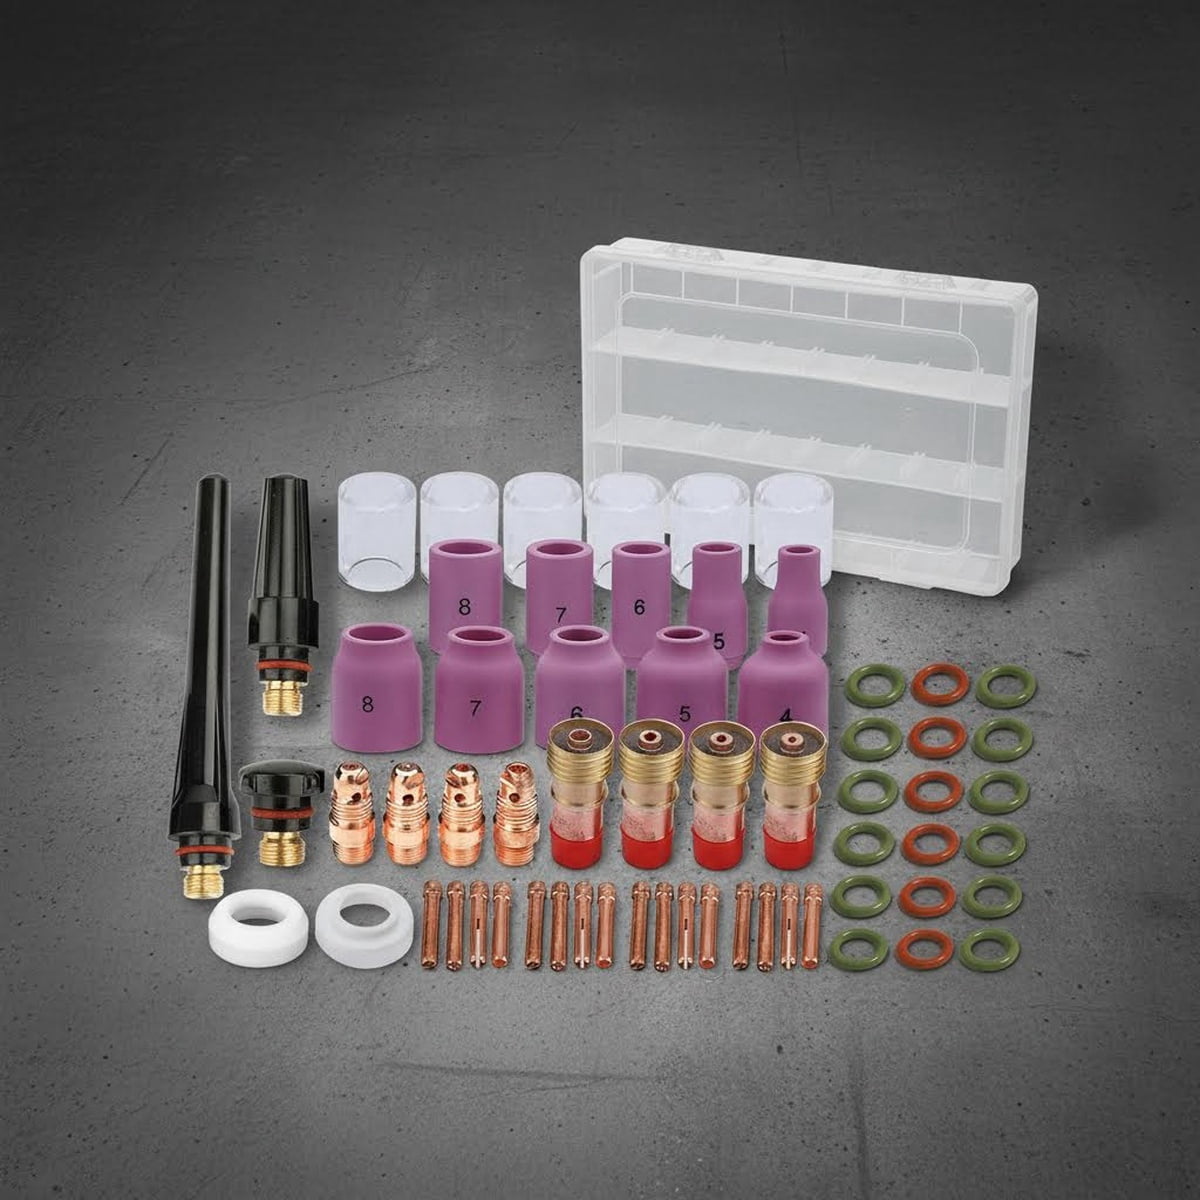
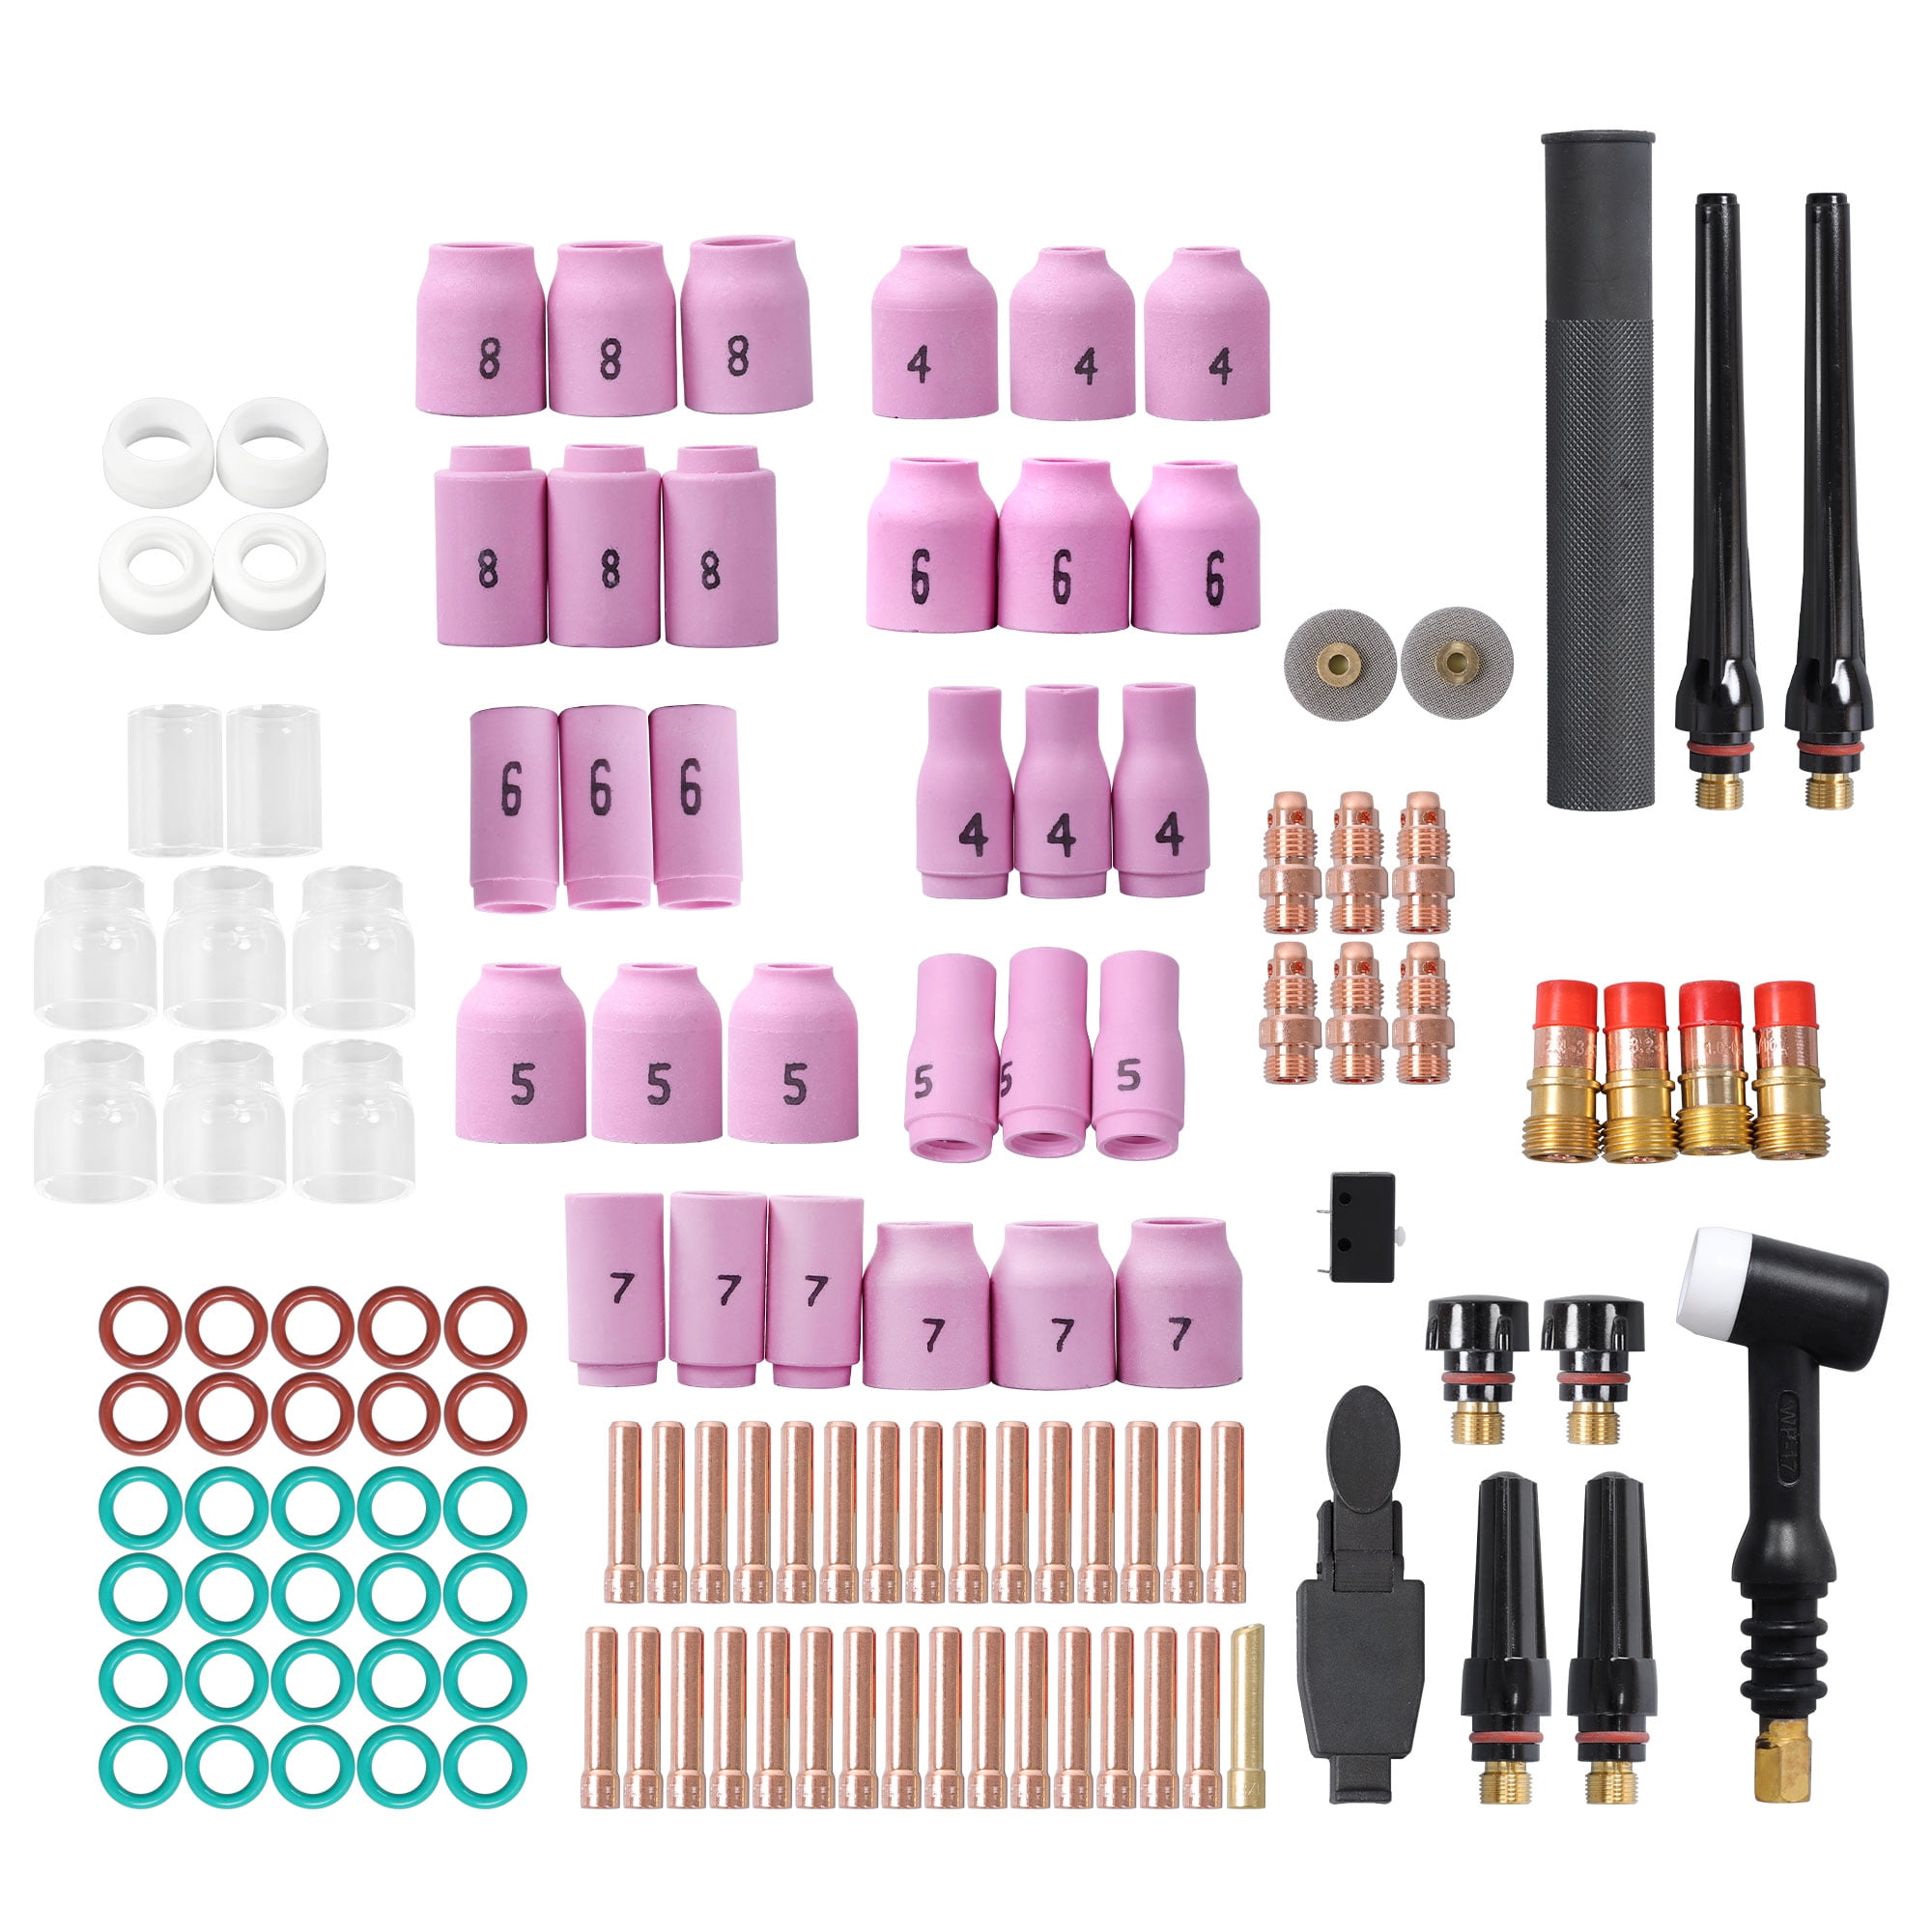
Five affiliate picks from Welding Consumables / Welding & Fab — electrodes, torch kits, and a tungsten sharpener for tip prep.
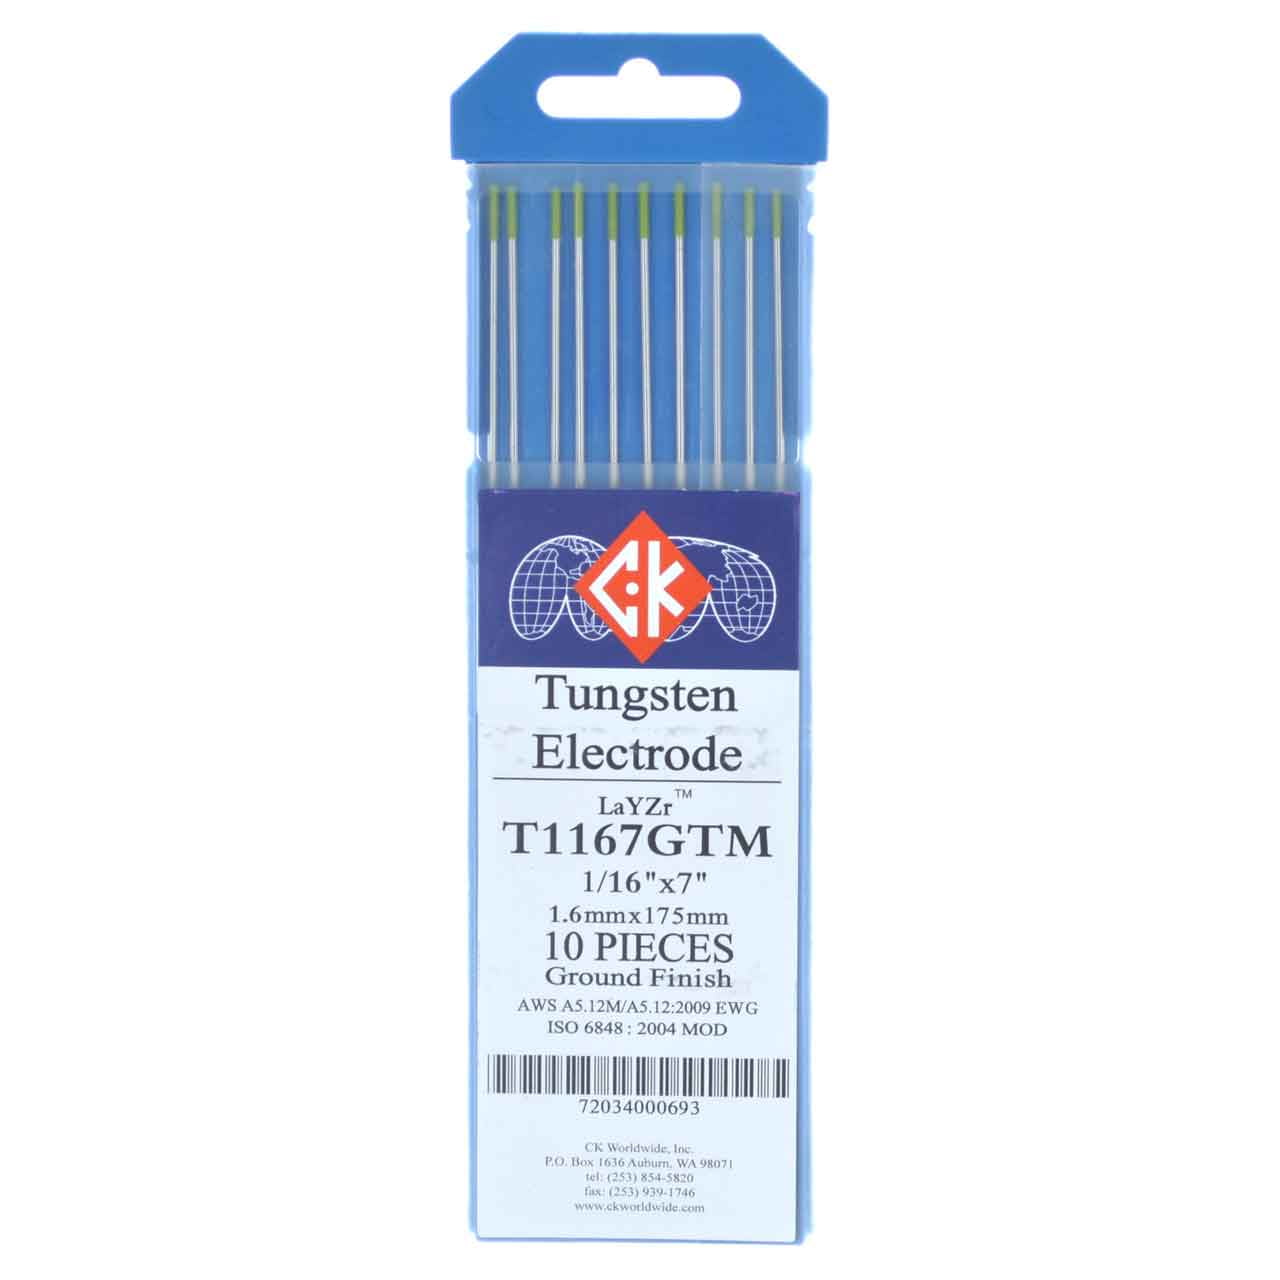
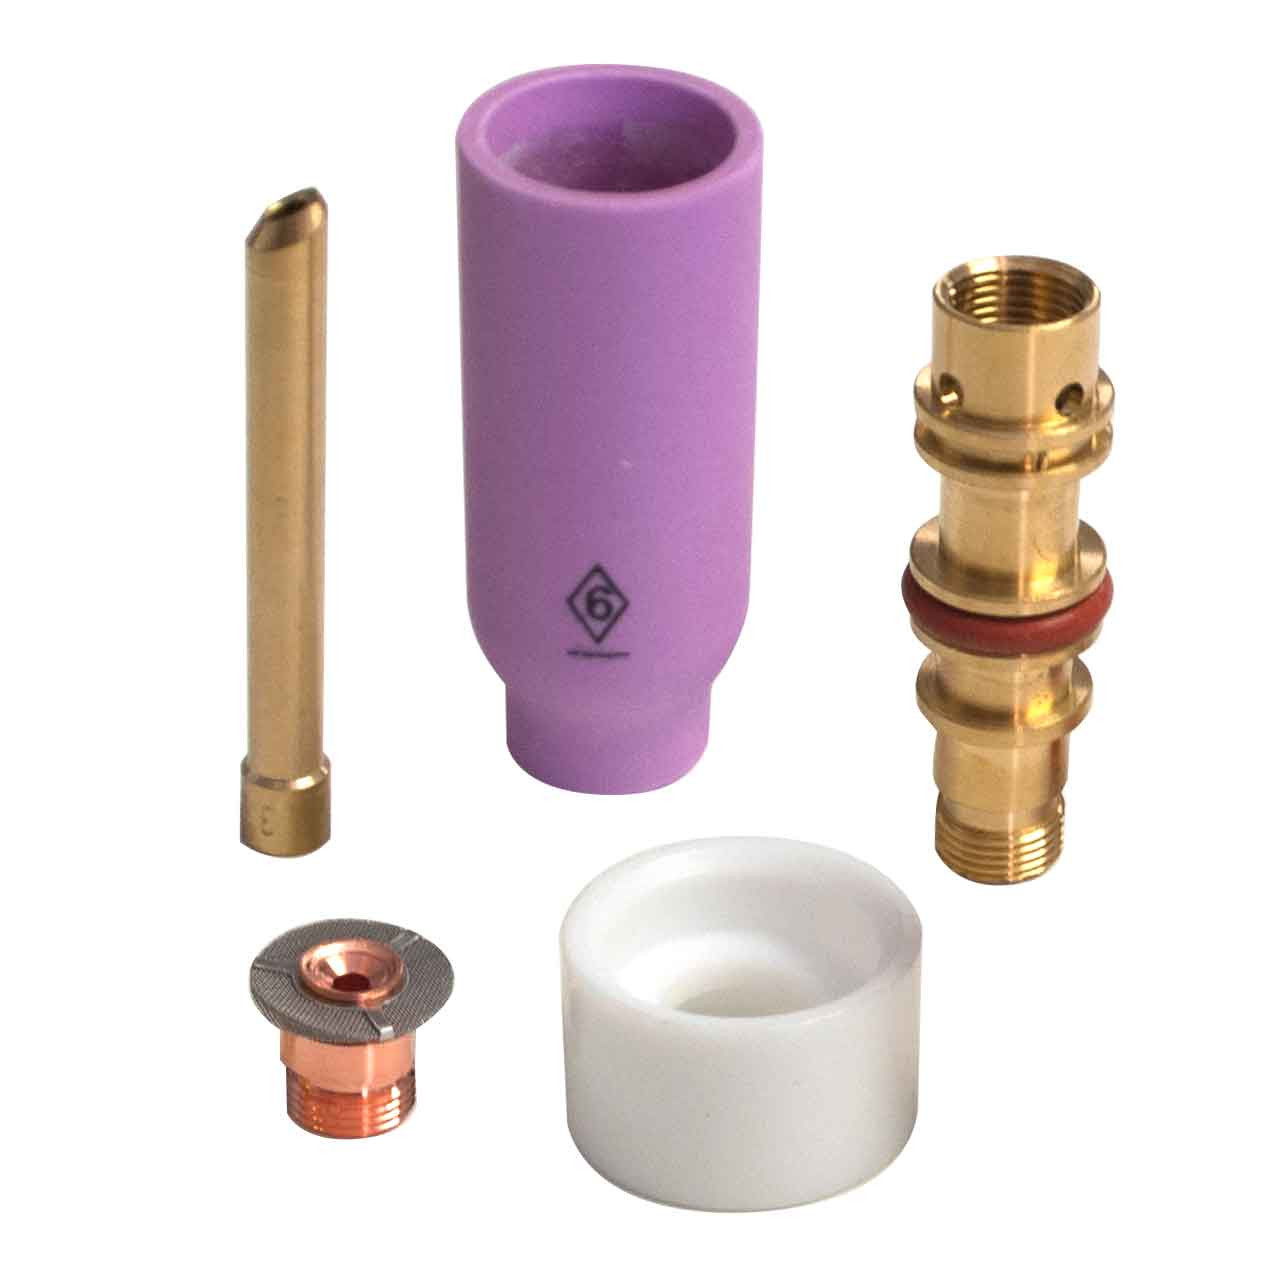
Enter the amperage window you will actually weld at (not the machine’s max dial), choose polarity, base metal, and the tungsten alloy you have (or plan to buy). The calculator returns the smallest standard diameter whose published AWS A5.12 capacity covers your maximum amps for that current type — plus tip prep and matching collet/cup guidance.
For thickness-based amps, filler, and gas flow, start with the TIG Welding Calculator, then come back here to lock electrode size and grind geometry. Type color codes and grinding technique live in the TIG Tungsten Electrode Guide. Home-shop vs production stocking decisions: Which Tungsten Type to Use.
DCEN (electrode negative) is the workhorse for steel and stainless — the tip runs cooler and carries the highest amps for a given size. AC sits between DCEN and DCEP because half the cycle heats the tip; aluminum cleaning needs that EP half-cycle. DCEP is rare in GTAW and only supports a fraction of DCEN current before the tip balloons.