Quick answer: stainless needs tighter heat control than mild steel. Run lower amps for thickness, use 100% argon with solid coverage, move with purpose, and back purge when backside quality matters. If the backside sugars or the face turns wide dull gray, heat input or shielding is wrong. You are TIG welding 304 stainless, the top looks okay, then the backside comes out dark and crusty. That is sugaring. It is not cosmetic – it hurts corrosion performance and can fail sanitary work. Stainless punishes sloppy shielding and excess dwell time faster than mild steel. This guide keeps it practical: amps by thickness, tungsten and filler picks, gas flow and cup sizing, back purge setup, and color feedback so you can adjust in real time. Use the TIG Welding Calculator and Gas Flow Calculator to sanity-check setup before wasting stainless. Starting points from the article values. Tune for joint fit-up, purge quality, and heat sink effects. Stainless usually wants less amp than mild steel for same thickness. For 316/316L base metal, move filler selection to ER316L. For dissimilar stainless-to-mild joints, ER309L is commonly used. Need the numbers, not the lecture? Use the calculators below when you want TIG settings, gas flow, heat input, or filler/wire usage without guessing. Stainless welding is touchy because heat piles up quickly and oxidation damage shows fast. It does not forgive slow travel and poor shielding. Joint type, gap, chill bars, and part temperature all move these values. Use these as start points, then tune with puddle behavior and color feedback. Stainless punishes slow travel and too much heat. If the weld gets wide, dull gray, or heavily colored, reduce heat input, move faster, pulse if useful, or improve fit-up/chill. Preferred type for DC stainless is 2% lanthanated. Keep grind lines lengthwise and point geometry consistent for clean arc starts. For TIG stainless, use 100% argon. Cup size and flow are huge on oxidation-sensitive work. If the back side turns crusty gray/black, that is sugaring. It is not just ugly – it hurts corrosion resistance and weld quality. Use back purge, backing gas, or proper shielding when the backside matters. Back purge is required for sanitary tubing and any full-penetration work where backside quality matters. Typical purge flow during welding is lower than initial purge flow; keep purge active through hot-cool phase, not just arc-on time. Target narrow HAZ and controlled tint. Stainless rewards fast, deliberate travel more than slow “pretty puddle” hovering. Heat-tint charts and amp tables will not fix a dipped tungsten, lost gas envelope, failed backpurge, or foot-pedal lag. Use TIG Welding Troubleshooting for those failure modes. id=”faq”>Frequently Asked Questions
100% argon is the standard for TIG stainless. If backside quality/corrosion/sanitation matters, yes. 2% lanthanated is a common modern default for DC stainless work. ER308L is standard for 304/304L. Usually oxidation from poor shielding, bad purge, or too much heat dwell. Backside oxygen exposure while the weld root is hot/molten. A common start range is about 80-110A, then tune by joint and fit-up. Yes on thin, tight-fit joints, but gap tolerance and strength goals decide if it is appropriate. Pulse can reduce average heat input and help thin material control. Control heat with travel speed, sequence, chill bars, and realistic amp settings. To TIG stainless cleanly: run lower amp than mild steel, protect the puddle with real gas coverage, and stay ahead of heat buildup. If color goes dark or backside sugars, stop and fix shielding/heat control before continuing. Also useful: Welding Gas Cost Calculator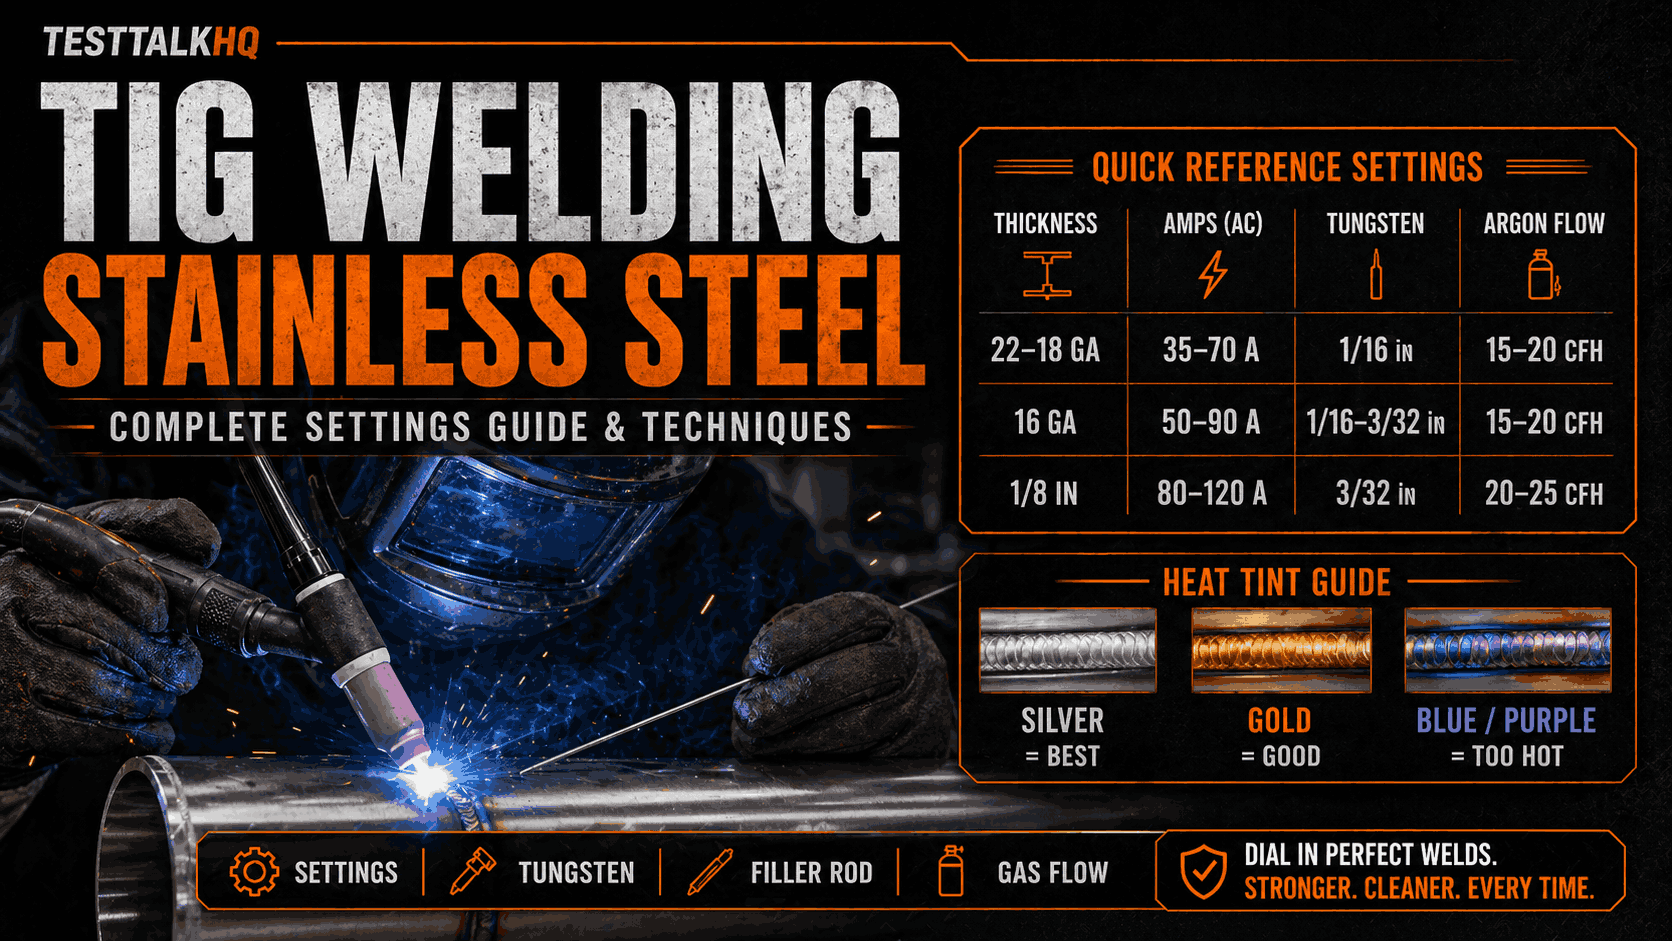
Shielding Gas Flow Rate Calculator
Heat Input Calculator
Electrode/Wire Consumption Calculator
Welding Gas Cost Calculator
TIG Stainless Steel Quick Answer
Stainless Thickness
Amps
Tungsten
Filler Rod
Argon Flow
Notes
22-20 ga
25-35A
0.040 or 1/16 in 2% lanthanated
.045 or 1/16 in ER308L
15-20 CFH (#6-8 cup)
Short arc, move fast, avoid overheating edge.
18 ga (0.048)
35-50A
1/16 in
1/16 in ER308L
18-25 CFH
Pulse can help reduce warp.
16 ga (0.060)
45-65A
1/16 in
1/16 in ER308L
20-30 CFH (#10-12)
Golden/straw tint is target.
1/8 in (0.125)
80-110A
1/16 or 3/32 in
1/16 or 3/32 in
20-30 CFH
Back purge if backside quality matters.
3/16 in
110-140A
3/32 in
3/32 or 1/8 in
25-35 CFH (#12-17)
Control heat buildup over long seams.
1/4 in
140-175A
3/32 or 1/8 in
1/8 in
25-35 CFH
Larger cup and steady travel improve consistency.
Why Stainless Is Different
Three differences that matter in the shop
Amperage by Thickness
Material Thickness
Gauge
Amperage Range
Filler Wire Size
0.035 in
20 ga
25-35A
1/16 in or .045
0.048 in
18 ga
35-50A
1/16 in
0.060 in
16 ga
45-65A
1/16 in
0.075 in
14 ga
55-75A
1/16 in
0.105 in
12 ga
70-95A
1/16 or 3/32 in
0.125 in
11 ga / 1/8 in
80-110A
1/16 or 3/32 in
0.1875 in
3/16 in
110-140A
3/32 or 1/8 in
0.250 in
1/4 in
140-175A
1/8 in
Heat control warning
Tungsten Selection
Tungsten Diameter
Amperage Capacity (DC)
Typical Application
0.040 in (1.0mm)
10-60A
Very thin stainless
1/16 in (1.6mm)
50-130A
Most stainless work
3/32 in (2.4mm)
120-210A
Thicker stainless
1/8 in (3.2mm)
200-300A
Heavy fabrication
Filler Rod Selection
Base Metal
Recommended Filler
Common Use
304 / 304L
ER308L
General stainless fabrication
316 / 316L
ER316L
Marine, chemical, chloride exposure
Dissimilar stainless to mild
ER309L
Dissimilar joints and transitions
321 / 347 service cases
ER347 (or per procedure)
High-temp stabilized applications
Argon Flow and Cup Size
Cup Size
Flow Rate (CFH)
Application
#6-8
15-20 CFH
Tight access, thin material
#10-12
20-30 CFH
General stainless
#15-17
30-40 CFH
Maximum coverage
Gas lens setups
20-35 CFH
Laminar flow, longer stickout
Back Purging Stainless
Backside oxidation warning
Heat Control and Color
Color
Meaning
Action
Silver / light straw
Very good shielding and heat control
Stay the course
Dark gold / bronze
Slightly elevated heat
Increase speed a little
Purple
Too much heat or marginal shielding
Move faster and verify gas
Blue
Excessive heat input
Reduce heat input and improve shielding
Gray / black
Oxidation failure
Fix shielding/back purge before continuing
Common TIG Stainless Mistakes
When Settings Still Do Not Fix the Bead
What gas do you use for TIG welding stainless?
Do you need to back purge stainless?
What tungsten should I use for stainless TIG?
What filler rod do I use for 304 stainless?
Why is my stainless TIG weld gray?
What causes sugaring on stainless?
How many amps for 1/8 inch stainless?
Can you TIG stainless without filler?
Is pulse TIG better for stainless?
How do you stop stainless from warping?
Conclusion
Shielding Gas Flow Rate Calculator
Heat Input Calculator
Electrode/Wire Consumption Calculator
Free Calculators & Tools
Match stainless DCEN amps to electrode diameter with the TIG Tungsten Electrode Selector.
Pointed-tip prep and lanthanated/ceriated color codes: TIG Tungsten Electrode Guide.
If tips discolor, crack, or burn away too fast on stainless DCEN: TIG Tungsten Electrode Troubleshooting.
Welding

Welding Reference Card
One page. MIG, TIG, stick and flux core settings by thickness.
$3.99
Buy
Complete Welding Settings Guide
19 pages. Four processes, stainless and aluminum, symbols and inspection.
$12.99
Buy
Welding Job Estimator
Price the job, then hand over a quote with no internal numbers.
Excel or Google Sheets. Best on a computer.
$29.00
Buy
Welding Complete Bundle
Card, 19-page guide and the estimator workbook. All six files.
Excel or Google Sheets. Best on a computer.
$34.99
$45.98 if bought separately — save $10.99
BuyCheckout opens in a new tab.