Oxy-Fuel vs Plasma Cutting — Which to Use
Thickness sweet spots, cost, portability, kerf quality, and material limits — pick the right thermal cutting process
Both processes cut ferrous plate, but they win in different shops. Use the decision fork below, then dial settings with the Oxy-Fuel Tip Calculator or Plasma Cutting Calculator.

The Decision Fork in One Minute
Choose oxy-fuel when…
- Cutting thick mild steel (roughly 1"–12"+) where speed per dollar favors gas
- No reliable electricity at the job (field, remote, demolition)
- You already run heating, gouging, or weld prep on the same rig
- Material is carbon steel that oxidizes cleanly
- Kerf width and HAZ are acceptable for the application
Choose plasma when…
- Cutting thin to medium plate (roughly gauge through ~1–1-1/2") with cleaner edges
- Stainless, aluminum, or galvanized need viable cuts
- Speed and squareness matter on intricate profiles
- Shop has compressed air (or machine gas) and power
- Minimal heat input reduces warping on thin sheet
Side-by-Side Comparison
| Factor | Oxy-Fuel | Plasma |
|---|---|---|
| Best thickness (mild steel) | 1/2"–12"+ sweet spot; capable below with small tips | Gauge–~1" typical; high-amp CNC to 2"+ |
| Stainless / aluminum | Poor — wrong chemistry | Good with correct gas and settings |
| Portability | No electricity; cylinders + torch | Needs power + air (or gas supply) |
| Cost per cut (thick plate) | Often lower consumable cost on heavy sections | Consumables + electricity; faster on thin |
| Kerf / edge quality | Wider kerf, more HAZ, more dross | Narrower kerf, squarer edge on thin/medium |
| Preheat / pierce | Slower start; large HAZ at start | Fast pierce; less distortion on thin |
| Secondary uses | Heating, bending, rosebud, gouging | Focused on cutting (+ marking on some units) |
Thickness Ranges — Practical Guidance
Thin sheet (under 1/8"): Plasma wins on speed and warp control. Oxy-fuel is possible with 000 tips but easy to overheat.
Structural plate (1/4"–1"): Overlap territory. Plasma gives cleaner fabrication edges; oxy-fuel is fine for roughing and demolition where edge finish is secondary.
Heavy plate (1"–6"+): Oxy-fuel remains the economical default in many steel service centers. Plasma needs high amperage and slow IPM on very thick stock.
Chart starting points: Oxy-Fuel Guide tables and Plasma Settings Guide.
Cost Per Cut — What Actually Drives It
Oxy-fuel: Cylinder rental/refill, tip life, and operator time. On 2" plate one tip may cut many feet — effective cost per inch can beat plasma if you already carry gas for heating.
Plasma: Consumables (electrode, nozzle, shield), electricity, and compressed air drying. On thin sheet, high IPM drives down cost per part even with frequent tip changes.
Neither wins universally — model your typical thickness mix and material types before buying new equipment.
Material Limits
Oxy-fuel requires an exothermic iron reaction. Stainless forms tight chrome oxide; aluminum oxide melts above the metal — both are poor oxy-fuel targets. Galvanized mild steel can be oxy-cut with heavy ventilation for zinc fumes, but plasma with proper air and PPE is often preferred in fab shops.
When material pushes you to plasma, continue with the plasma cluster: Troubleshooting, Compressor Sizing, and Cutting Speed Calculator.
Dial Settings for Your Choice
Oxy-Fuel Tip Calculator → Plasma Calculator → Oxy-Fuel Troubleshooting →
Shop Pick — Oxy-Fuel Hose (CSV Verified)
One genuine affiliate match for this cluster. Tips and regulators are catalog gaps.
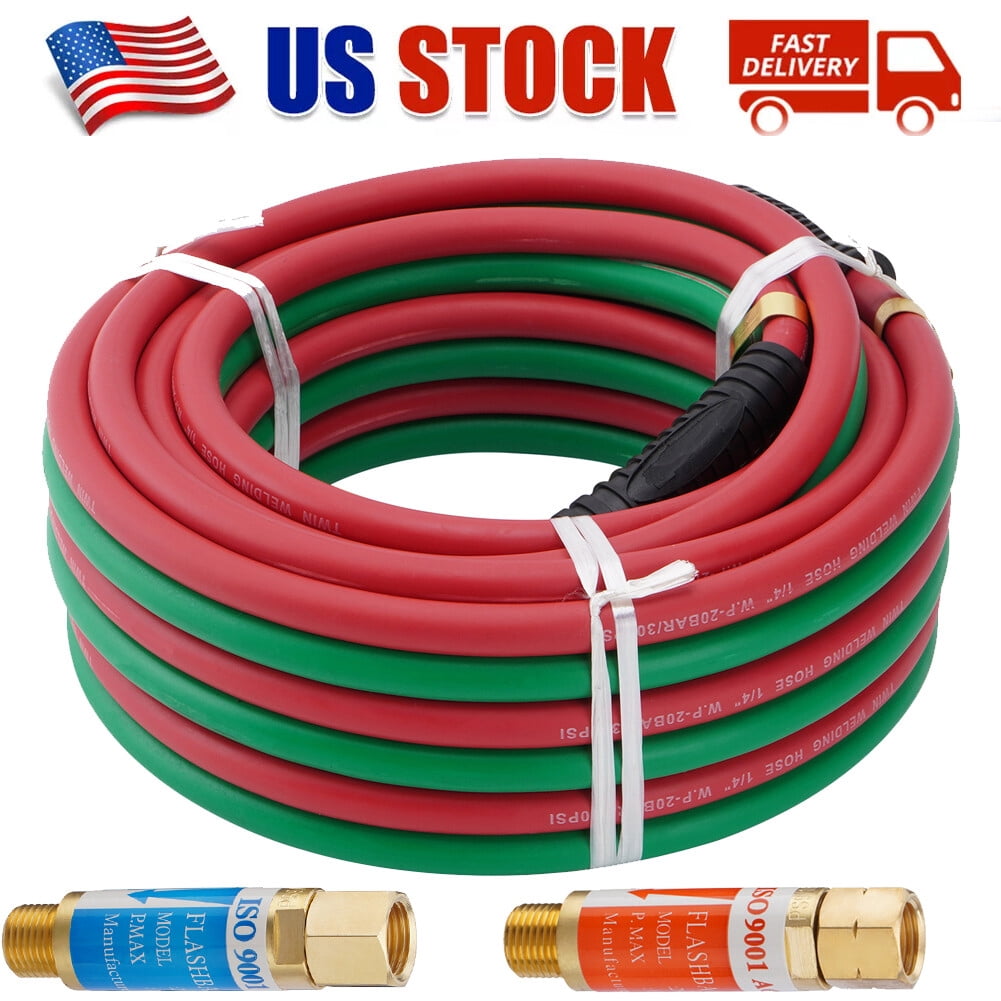
RX WELD Oxygen Acetylene Hose 1/4-Inch 50 Feet B Fittings
- Shared infrastructure for oxy-fuel cutting rigs
- Grade-T service for cutting and heating
- Not a substitute for cutting tips or regulators
As an Amazon Associate, TestTalkHQ earns from qualifying purchases.