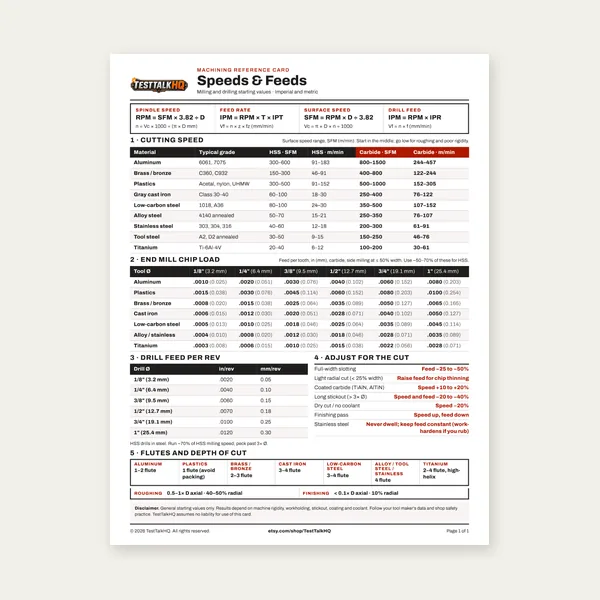
Machining Speeds & Feeds Card
One page. Speeds, chip load and drill feed, imperial and metric.
$3.99
BuySame plasma, two different control problems — programmed Z and IPM vs wrist, drag, and feel
A 65A air plasma cutting 1/4" mild steel is the same physics in a gantry and in a hand torch. The numbers on the console are not interchangeable. One process programs pierce height, delay, cut height, and feed. The other sets amps, guesses a standoff, and travels by eye. Copying handheld IPM into CAM — or copying a table pierce height onto a drag tip — is how shops blow consumables and still get dross.
On a table? Use the CNC calculator.Pierce height, delay, cut height, IPM band. Handheld amps stay on the other tool.
Open CNC Calculator →Use the CNC Pierce Height & Cut Speed Calculator when the torch is in a gantry, a track, or any machine that only knows Z and feed. That is this calculator, the dial-in guide, and table troubleshooting.
Use the Plasma Cutting Calculator when a person is holding the torch. Amps, travel speed, pierce time, gas pressure, torch angle. That is the handheld plasma calculator, the settings guide, and handheld troubleshooting.
| Variable | CNC / gantry | Handheld torch |
|---|---|---|
| Standoff | Pierce height then cut height (two programmed Z values, often with THC) | Drag tip, rolling the wrist, or a guessed 1/16–1/8" |
| Pierce | Delay in seconds at pierce height; motion forbidden until the hole is through | Linger, then pull; operator sees the spark change |
| Speed | IPM in the post / controller, repeatable to a tenth | Walking pace; “about 15 IPM” is a wish |
| Amps / voltage | Process amps selected for the consumable stack; arc voltage often used as THC feedback | Panel amps and a voltage the operator never programs as height |
| Lead-in | Geometry in CAM (line, arc, pierce offset) | A kick of the wrist at the edge |
| Air | Must hold PSI for the whole nest — long duty | Short cuts; a small compressor can fake it |
That is why this cluster does not reprint handheld amperage tables. Those tables already exist. This cluster only answers the four machine numbers.
A handheld chart might show a faster travel on 1/4" because the operator is dragging a shield (near-zero standoff) and can slow by feel at the end of the cut. A mechanized chart for the same amps assumes a 0.06" cut height and a constant feed. Constant feed at drag-tip speed will undercut or blow through corners. Constant feed at a too-high standoff will hard-dross.
Pierce time vs pierce delay is the other mix-up. Handheld “pierce time” is how long you stand there. CNC “pierce delay” is a dwell after transfer, at a height that is higher than the cut. If you type handheld pierce time into a control that already ramps Z, you double the heat in the hole and crater the nozzle.
Arc voltage on a table is often a height stand-in (THC). On a handheld it is a panel curiosity. Do not copy a handheld voltage into a THC set point unless the OEM chart says to — and that chart is still not this calculator’s job.
Gantry numbersStarting-point pierce, delay, height, and IPM range — not torch amps.
Open CNC Plasma Calculator →No honest constant. Standoff, lead-in, and constant vs variable travel change the heat. Start from the CNC calculator band and coupon it.
Use it for amps and air. Do not use its travel speed as gantry feed. Set heights from this tool, then coupon speed.
If there is a THC or a Z command, you are in this cluster. If there is a trigger and a ground clamp in the other hand, you are on the handheld cluster.
One page. Speeds, chip load and drill feed, imperial and metric.
$3.99
Buy
27 pages. Milling, drilling, tapping, turning and CNC routing.
$12.99
Buy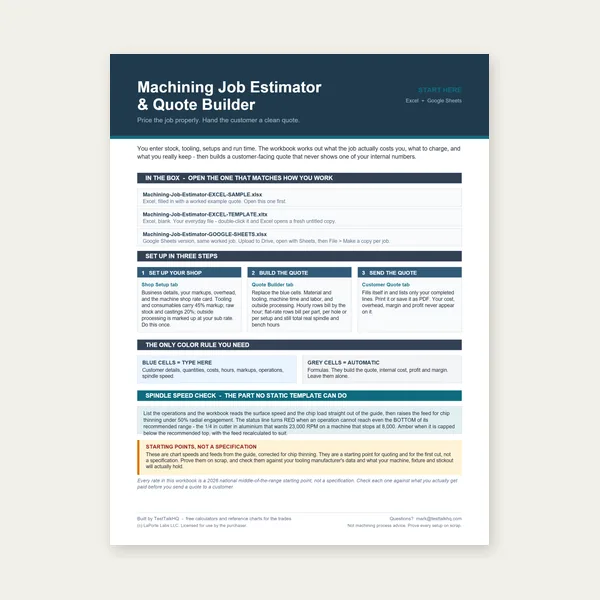
Quote shop work and check operations against your spindle's top speed.
Excel or Google Sheets. Best on a computer.
$29.00
Buy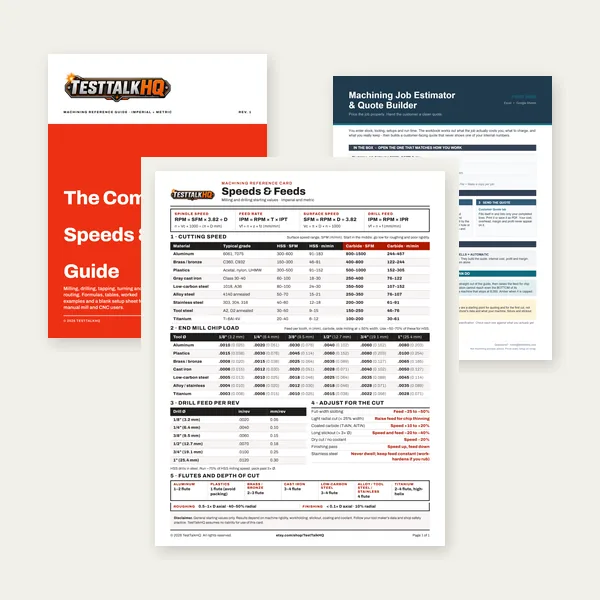
Card, 27-page guide and the estimator workbook. All six files.
Excel or Google Sheets. Best on a computer.
$34.99
$45.98 if bought separately — save $10.99
BuyCheckout opens here — you stay on this page.
From the TestTalkHQ plasma catalog — CNC-ready amperage, shop air that holds PSI under a long gantry cut, and spare consumables. Handheld torch amps still live on the handheld plasma calculator.
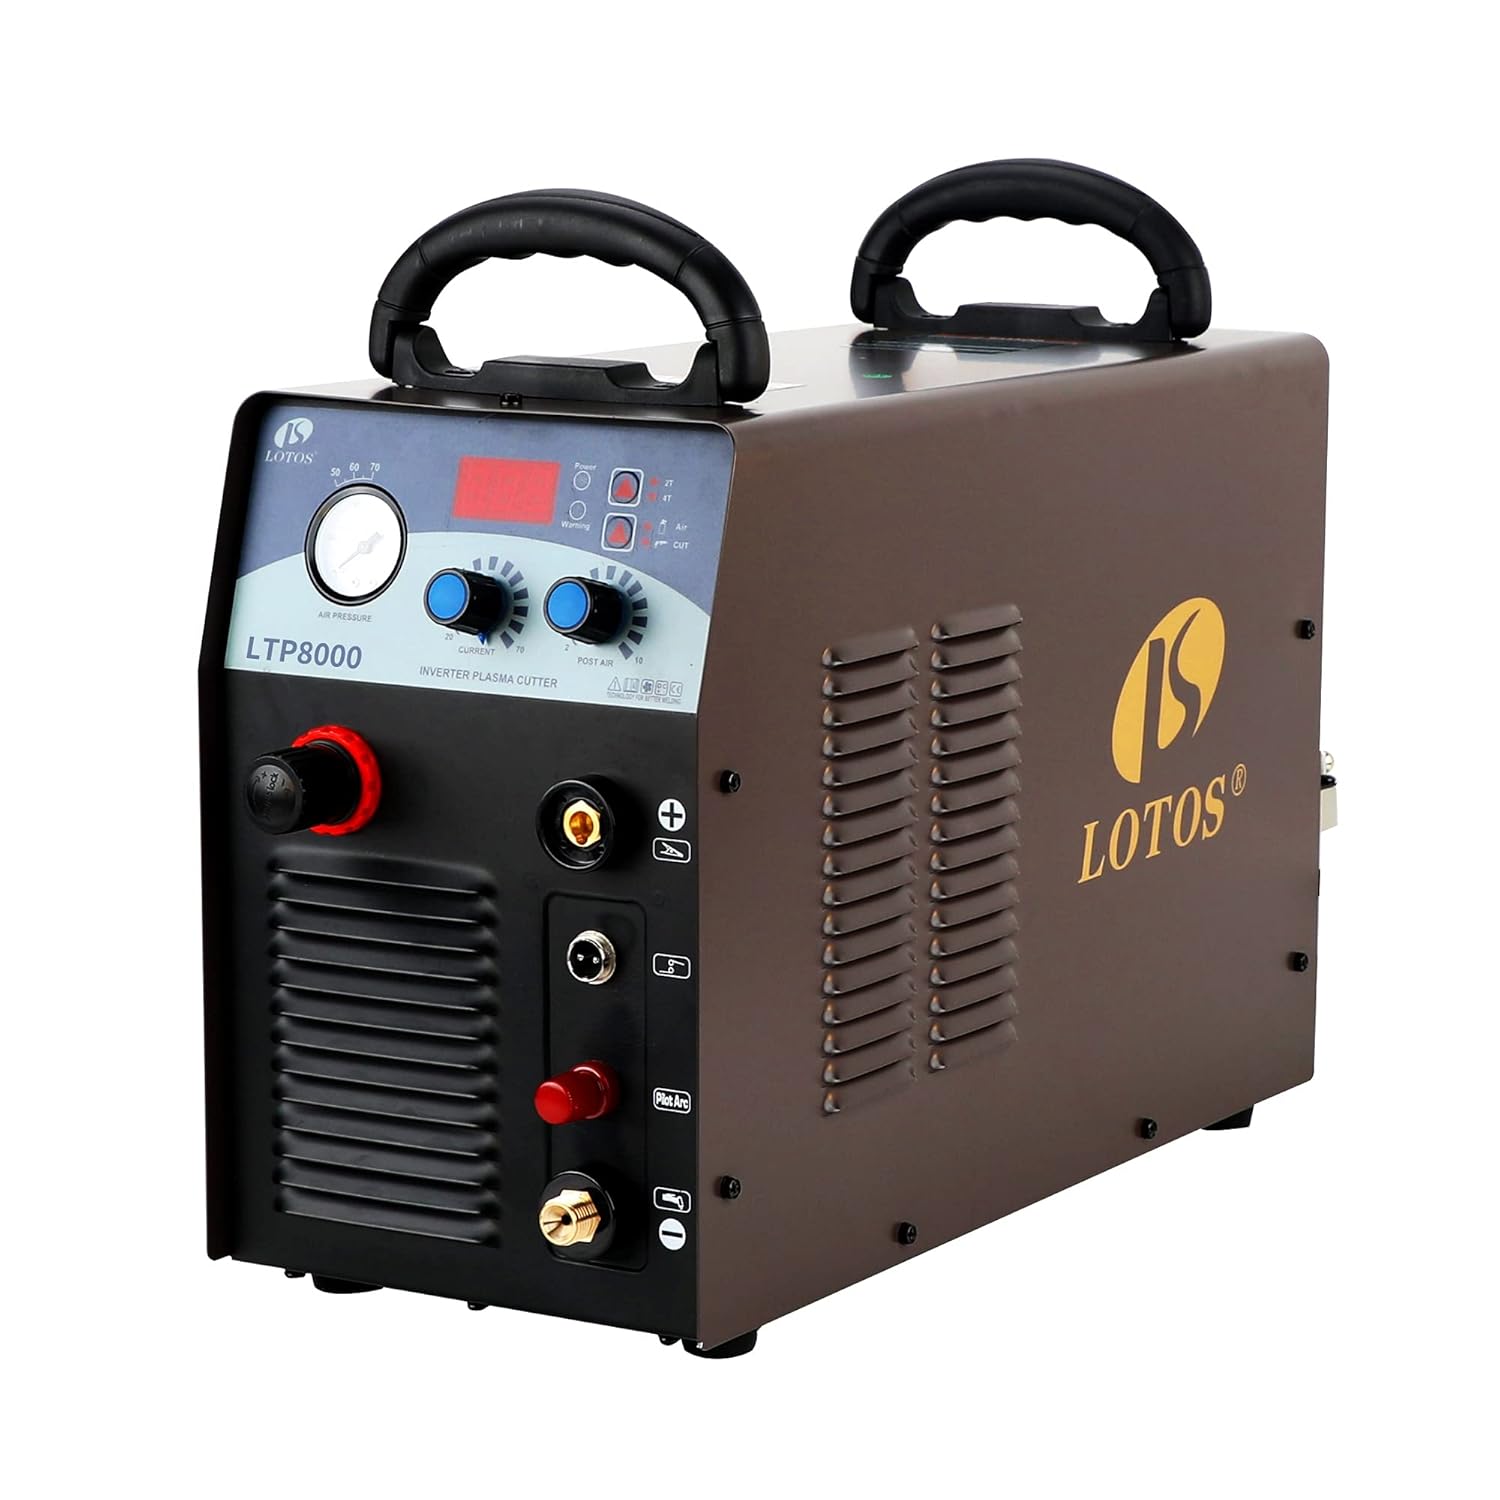
80A class with a CNC-ready torch lead. Matches the 85A column in this calculator for 1/4–1/2" mild steel on a small gantry.
View on Amazon →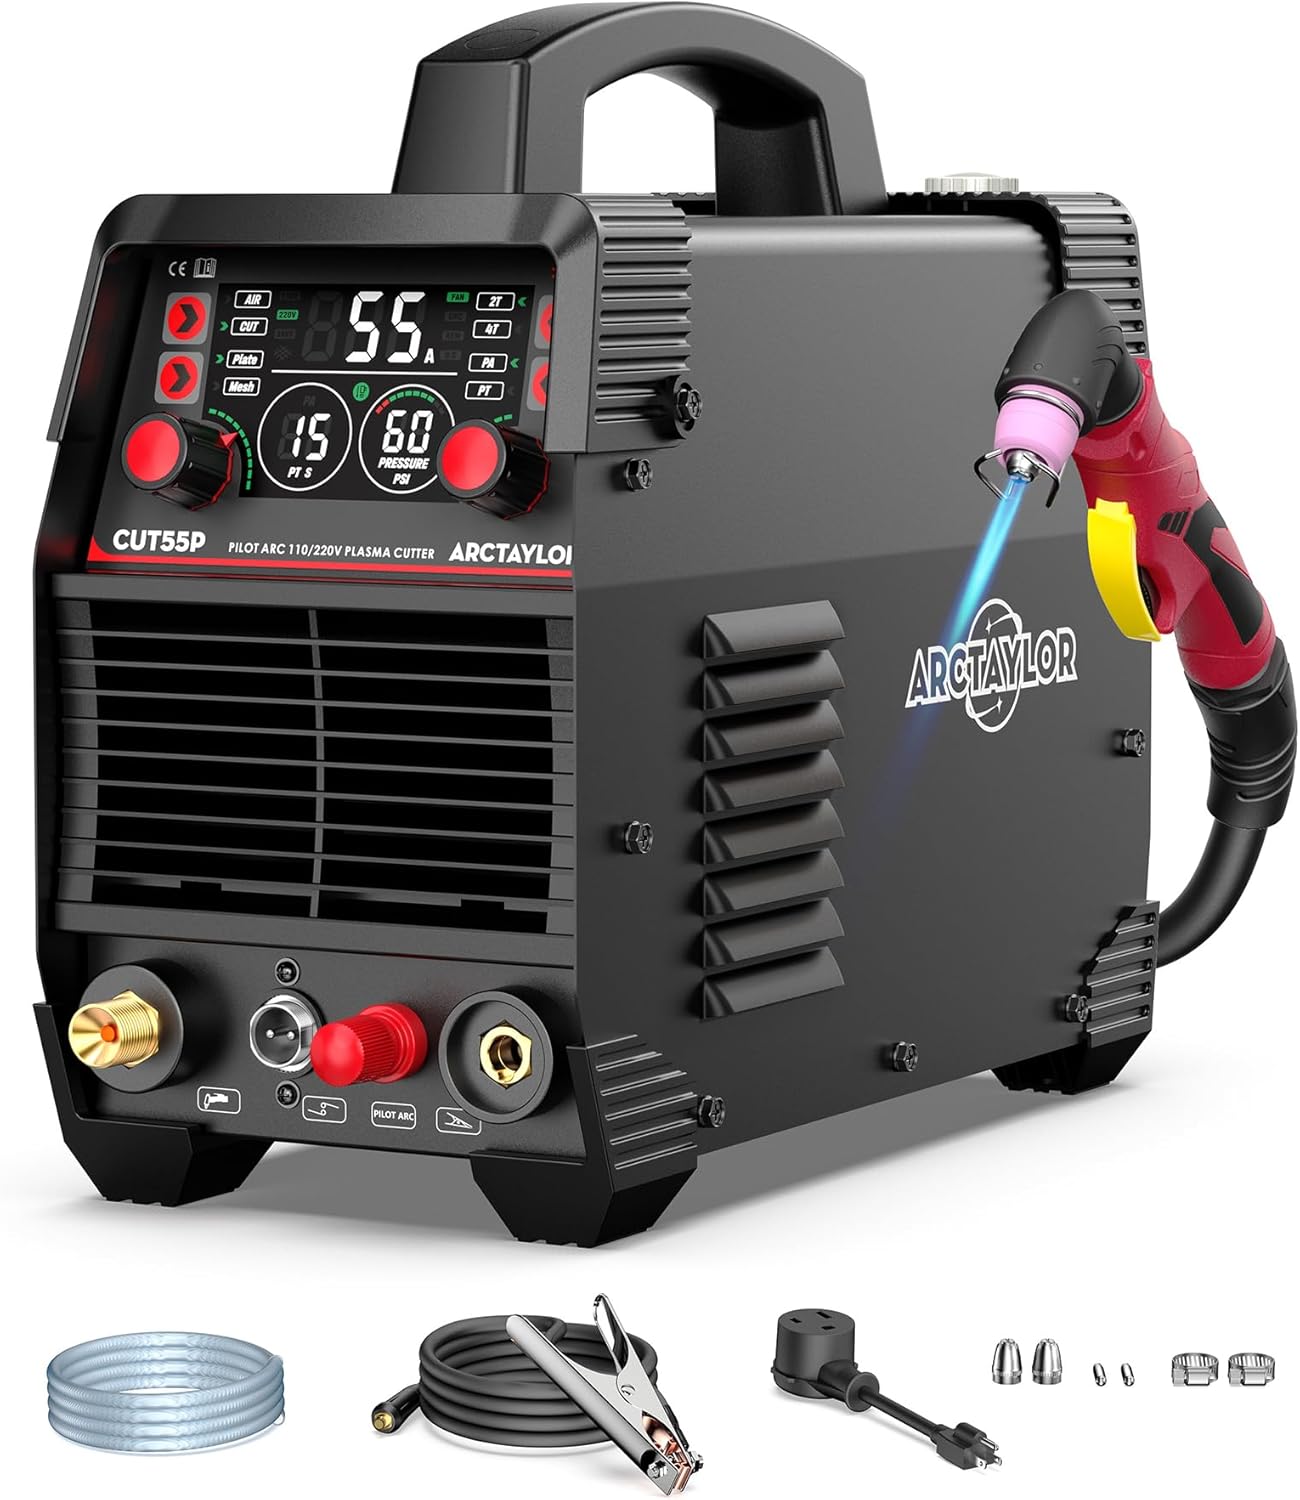
Hobby-table range. Use the 45A or 65A starting points here, then drop pierce delay if the stack is 16 ga, not 1/4".
View on Amazon →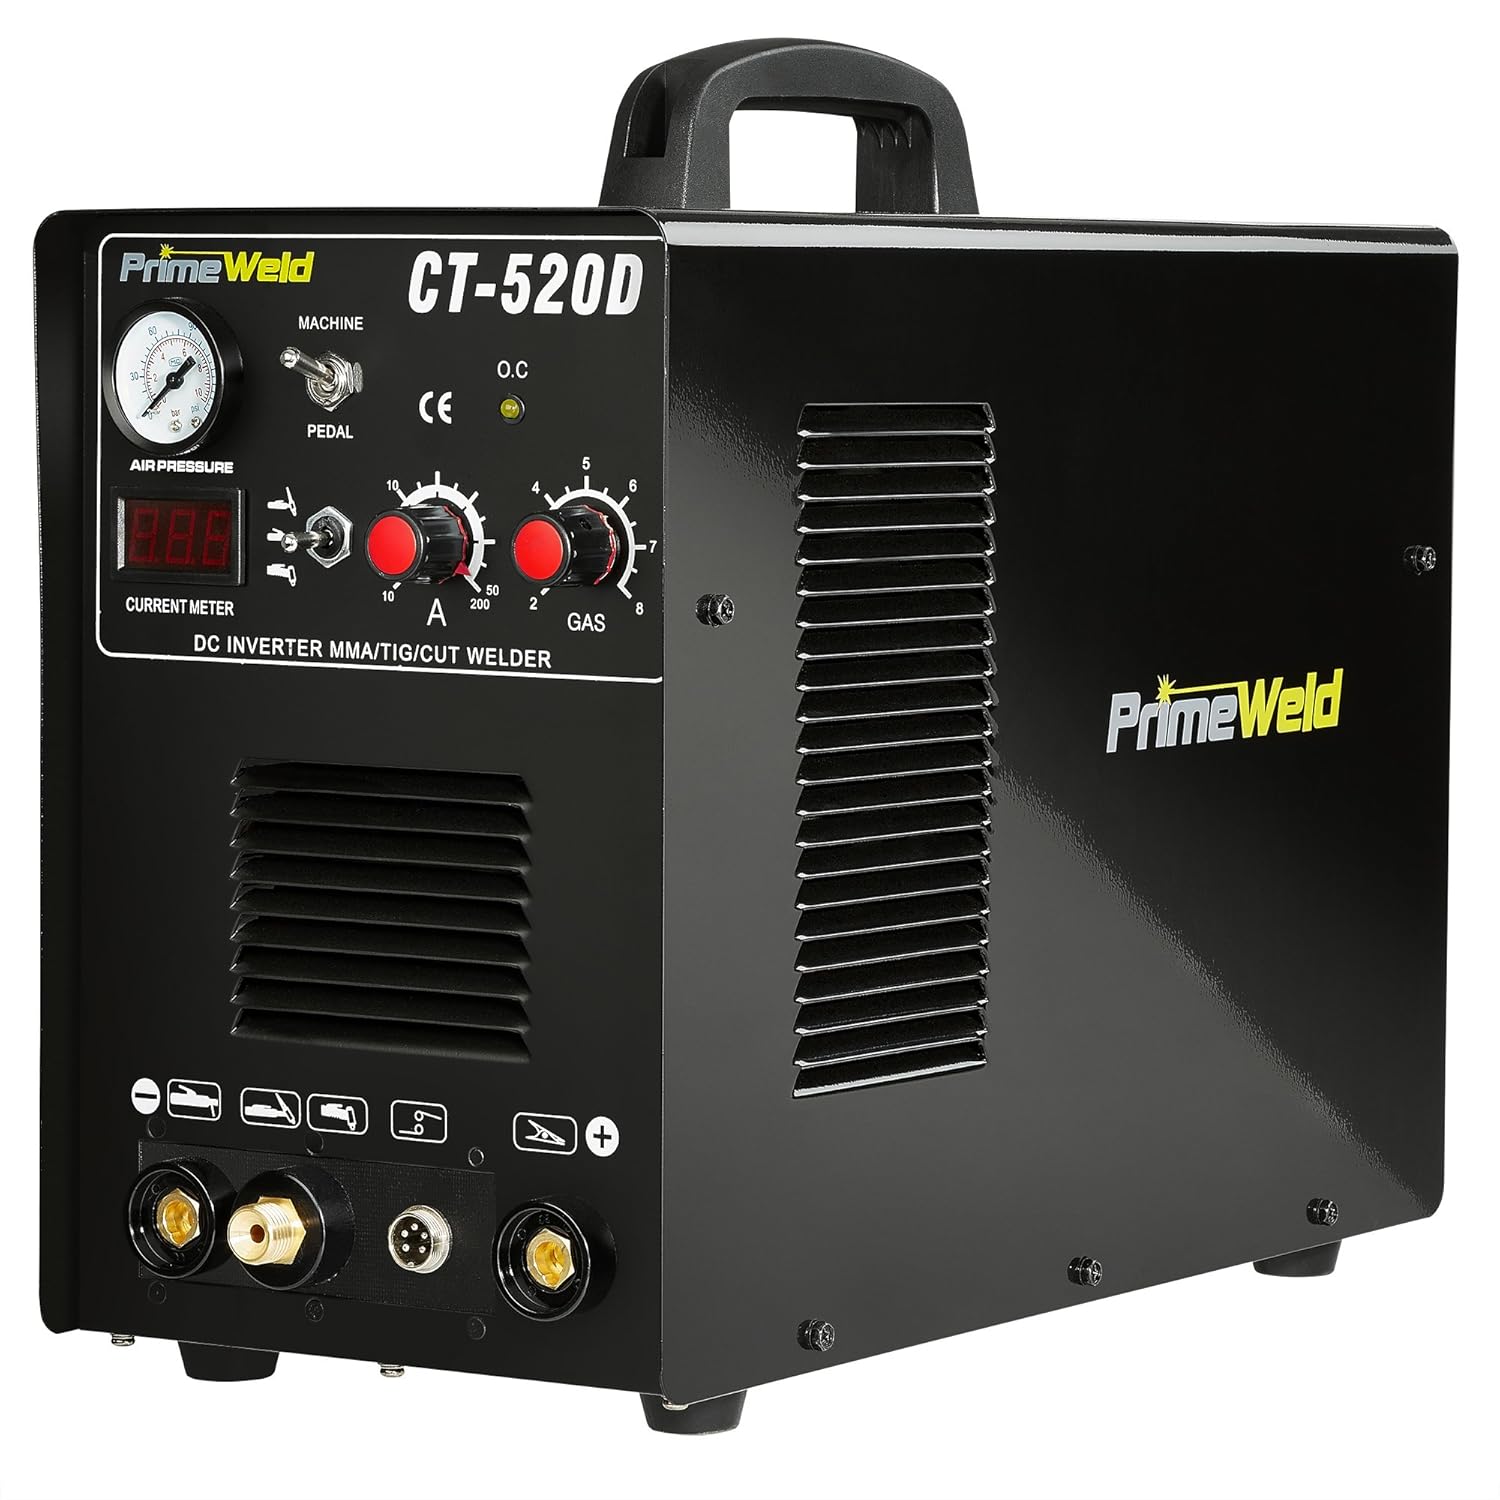
50A plasma on a combo box. Fine for a small CNC table on sheet; do not treat it as a 105A production chart.
View on Amazon →
Gantry cuts run longer than a handheld pass. If PSI sags, pierce delay and cut height will not save the edge. Sizing: plasma compressor guide.
View on Amazon →
Blown nozzles from a low pierce or a late motion command look like “wrong IPM.” Change tip and electrode as a pair before you rewrite the post processor.
View on Amazon →
Every new material lot gets a 2" test pierce and a 6" straight cut before the nest. This calculator is the starting point; the coupon is the lock-in.
Read the Dial-In Guide →As an Amazon Associate, TestTalkHQ earns from qualifying purchases.