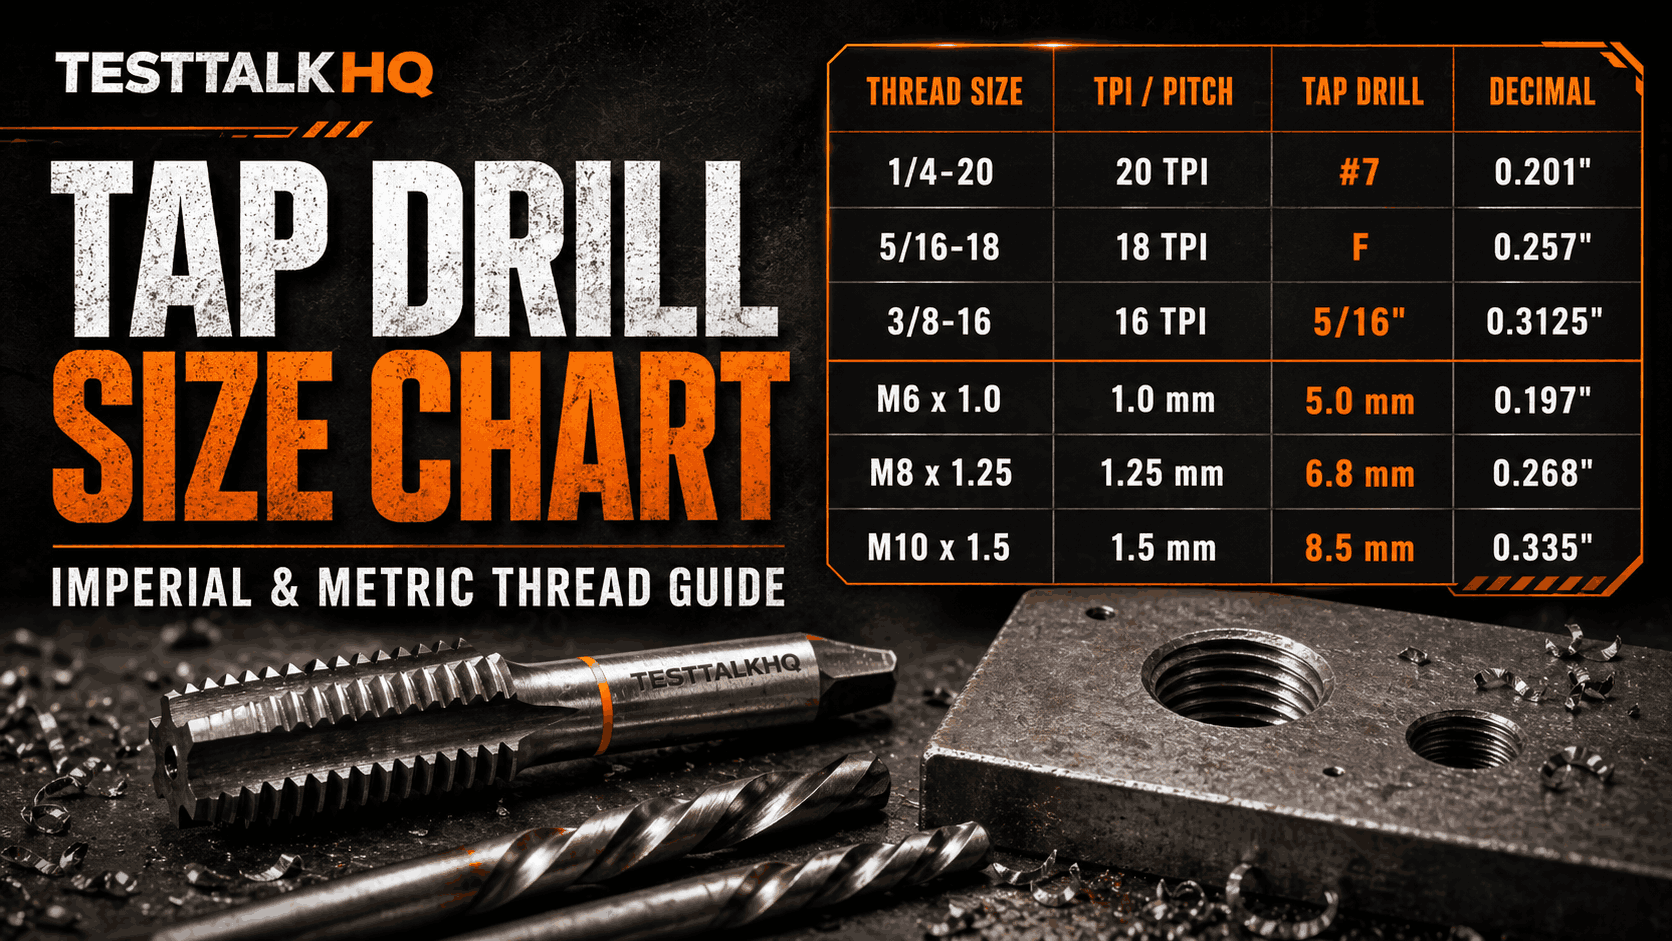
Fast answer: drill size before tapping depends on thread size and pitch. Coarse and fine threads do not use the same drill. Too small breaks taps. Too large gives weak threads. Use chart values first, then adjust carefully for material and hole type.
Imperial UNC and UNF plus metric ISO coarse and fine, with a tap drill and a clearance drill on every row. Decimal inches sit beside the named drill so you can match a bit you already have. Tap drills are sized for roughly 75% thread.
This is a chart-first reference for shop work: tap drill sizes, practical thread engagement guidance, blind-hole depth reminders, and the mistakes that snap taps. Use the Tap Drill Size Calculator with the Drill Speed Calculator and Cutting Speed / Feed Rate Calculator when you want repeatable results without guessing.
Drill Speed Calculator
Cutting Speed / Feed Rate Calculator
Bolt Torque Calculator
Free Calculators & Tools
Tap Drill Size Quick Answer
Exact values from the full charts below. Coarse and fine rows of the same nominal size share one close-fit clearance drill.
| Thread | Tap drill | Tap drill (in) | Clearance drill | Clearance (in) |
|---|---|---|---|---|
| 10-32 | #21 | .1590 | #9 | .1960 |
| 1/4-20 | #7 | .2010 | F | .2570 |
| 1/4-28 | #3 | .2130 | F | .2570 |
| 3/8-16 | 5/16 | .3125 | W | .3860 |
| 3/8-24 | Q | .3320 | W | .3860 |
| M8 × 1.25 | 6.8 | .2677 | 9.0 | .3543 |
| M8 × 1.0 | 7.0 | .2756 | 9.0 | .3543 |
Need the numbers, not the lecture?
Use the calculators below when you want tap drill size, drill RPM, cutting speed, feed rate, or bolt torque without guessing.
What Tap Drill Size Means
Tap drill size controls thread strength and tapping effort at the same time. A smaller hole gives higher thread engagement but raises cutting force and break risk. A larger hole cuts easier but weakens thread holding.
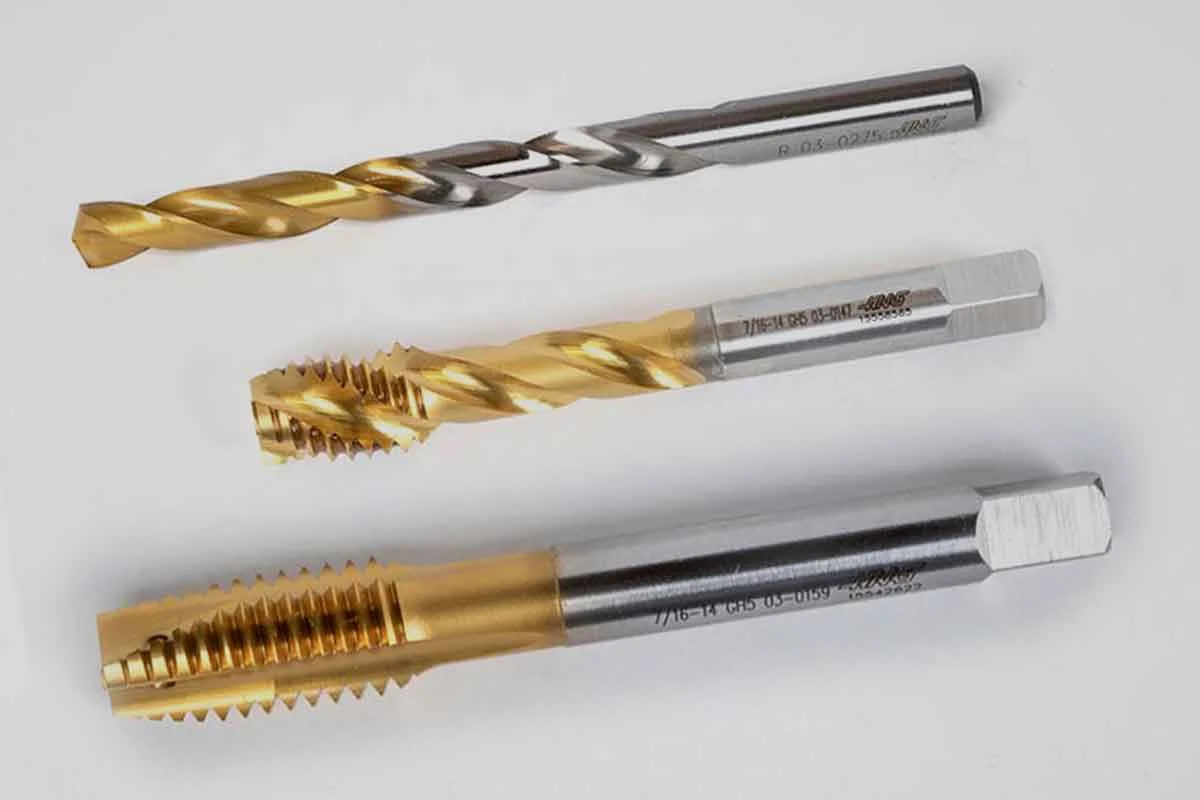
Imperial (UNC / UNF)
Coarse and fine rows for the same nominal size share one close-fit clearance drill. Tap drill decimals are inches.
| Thread | Tap drill | Tap drill (in) | Clearance drill | Clearance (in) |
|---|---|---|---|---|
| #0-80 | 3/64 | .0469 | #52 | .0635 |
| #1-64 | #53 | .0595 | #48 | .0760 |
| #1-72 | #53 | .0595 | #48 | .0760 |
| #2-56 | #50 | .0700 | #43 | .0890 |
| #2-64 | #50 | .0700 | #43 | .0890 |
| #3-48 | #47 | .0785 | #37 | .1040 |
| #3-56 | #45 | .0820 | #37 | .1040 |
| #4-40 | #43 | .0890 | #32 | .1160 |
| #4-48 | #42 | .0935 | #32 | .1160 |
| #5-40 | #38 | .1015 | #30 | .1285 |
| #5-44 | #37 | .1040 | #30 | .1285 |
| #6-32 | #36 | .1065 | #27 | .1440 |
| #6-40 | #33 | .1130 | #27 | .1440 |
| #8-32 | #29 | .1360 | #18 | .1695 |
| #8-36 | #29 | .1360 | #18 | .1695 |
| #10-24 | #25 | .1495 | #9 | .1960 |
| #10-32 | #21 | .1590 | #9 | .1960 |
| #12-24 | #16 | .1770 | #2 | .2210 |
| #12-28 | #14 | .1820 | #2 | .2210 |
| 1/4-20 | #7 | .2010 | F | .2570 |
| 1/4-28 | #3 | .2130 | F | .2570 |
| 5/16-18 | F | .2570 | P | .3230 |
| 5/16-24 | I | .2720 | P | .3230 |
| 3/8-16 | 5/16 | .3125 | W | .3860 |
| 3/8-24 | Q | .3320 | W | .3860 |
| 7/16-14 | U | .3680 | 29/64 | .4531 |
| 7/16-20 | 25/64 | .3906 | 29/64 | .4531 |
| 1/2-13 | 27/64 | .4219 | 33/64 | .5156 |
| 1/2-20 | 29/64 | .4531 | 33/64 | .5156 |
| 9/16-12 | 31/64 | .4844 | 37/64 | .5781 |
| 9/16-18 | 33/64 | .5156 | 37/64 | .5781 |
| 5/8-11 | 17/32 | .5312 | 41/64 | .6406 |
| 5/8-18 | 37/64 | .5781 | 41/64 | .6406 |
| 3/4-10 | 21/32 | .6562 | 49/64 | .7656 |
| 3/4-16 | 11/16 | .6875 | 49/64 | .7656 |
| 7/8-9 | 49/64 | .7656 | 57/64 | .8906 |
| 7/8-14 | 13/16 | .8125 | 57/64 | .8906 |
| 1-8 | 7/8 | .8750 | 1-1/64 | 1.0156 |
| 1-12 | 59/64 | .9219 | 1-1/64 | 1.0156 |
Metric (ISO coarse / fine)
Tap drill and clearance drill are millimeters. The inch columns are decimal equivalents. Clearance is the ISO 273 medium series.
| Thread | Tap drill | Tap drill (in) | Clearance drill | Clearance (in) |
|---|---|---|---|---|
| M1.6 × 0.35 | 1.25 | .0492 | 1.8 | .0709 |
| M2 × 0.4 | 1.6 | .0630 | 2.4 | .0945 |
| M2.5 × 0.45 | 2.05 | .0807 | 2.9 | .1142 |
| M3 × 0.5 | 2.5 | .0984 | 3.4 | .1339 |
| M3 × 0.35 | 2.65 | .1043 | 3.4 | .1339 |
| M3.5 × 0.6 | 2.9 | .1142 | 3.9 | .1535 |
| M4 × 0.7 | 3.3 | .1299 | 4.5 | .1772 |
| M4 × 0.5 | 3.5 | .1378 | 4.5 | .1772 |
| M5 × 0.8 | 4.2 | .1654 | 5.5 | .2165 |
| M5 × 0.5 | 4.5 | .1772 | 5.5 | .2165 |
| M6 × 1.0 | 5.0 | .1969 | 6.6 | .2598 |
| M6 × 0.75 | 5.25 | .2067 | 6.6 | .2598 |
| M7 × 1.0 | 6.0 | .2362 | 7.6 | .2992 |
| M8 × 1.25 | 6.8 | .2677 | 9.0 | .3543 |
| M8 × 1.0 | 7.0 | .2756 | 9.0 | .3543 |
| M10 × 1.5 | 8.5 | .3346 | 11.0 | .4331 |
| M10 × 1.25 | 8.8 | .3465 | 11.0 | .4331 |
| M10 × 1.0 | 9.0 | .3543 | 11.0 | .4331 |
| M12 × 1.75 | 10.2 | .4016 | 13.5 | .5315 |
| M12 × 1.5 | 10.5 | .4134 | 13.5 | .5315 |
| M12 × 1.25 | 10.8 | .4252 | 13.5 | .5315 |
| M14 × 2.0 | 12.0 | .4724 | 15.5 | .6102 |
| M14 × 1.5 | 12.5 | .4921 | 15.5 | .6102 |
| M16 × 2.0 | 14.0 | .5512 | 17.5 | .6890 |
| M16 × 1.5 | 14.5 | .5709 | 17.5 | .6890 |
| M18 × 2.5 | 15.5 | .6102 | 20.0 | .7874 |
| M20 × 2.5 | 17.5 | .6890 | 22.0 | .8661 |
| M20 × 1.5 | 18.5 | .7283 | 22.0 | .8661 |
| M22 × 2.5 | 19.5 | .7677 | 24.0 | .9449 |
| M24 × 3.0 | 21.0 | .8268 | 26.0 | 1.0236 |
| M24 × 2.0 | 22.0 | .8661 | 26.0 | 1.0236 |
How to use this chart
75% thread
75% thread is the default. Full strength for most work. In hard material, deep holes, or hand tapping, step up one drill size: less thread engagement, but the tap survives.
Clearance
Clearance values here are close fit. When holes won’t line up perfectly, go one drill size larger (free fit).
Metric shortcut
Tap drill equals major diameter minus pitch. M8 × 1.25 → 6.8 mm. That shortcut holds all the way down the column.
Need a different percent of thread, or a form tap, use the Tap Drill Size Calculator. Pipe threads are a different chart: NPT Tap Drill Size Chart.
Drill bits and taps
Index drills cover the number, letter, and fractional tap holes in the imperial chart. A tap-and-die set and cutting fluid cover the rest of the job.
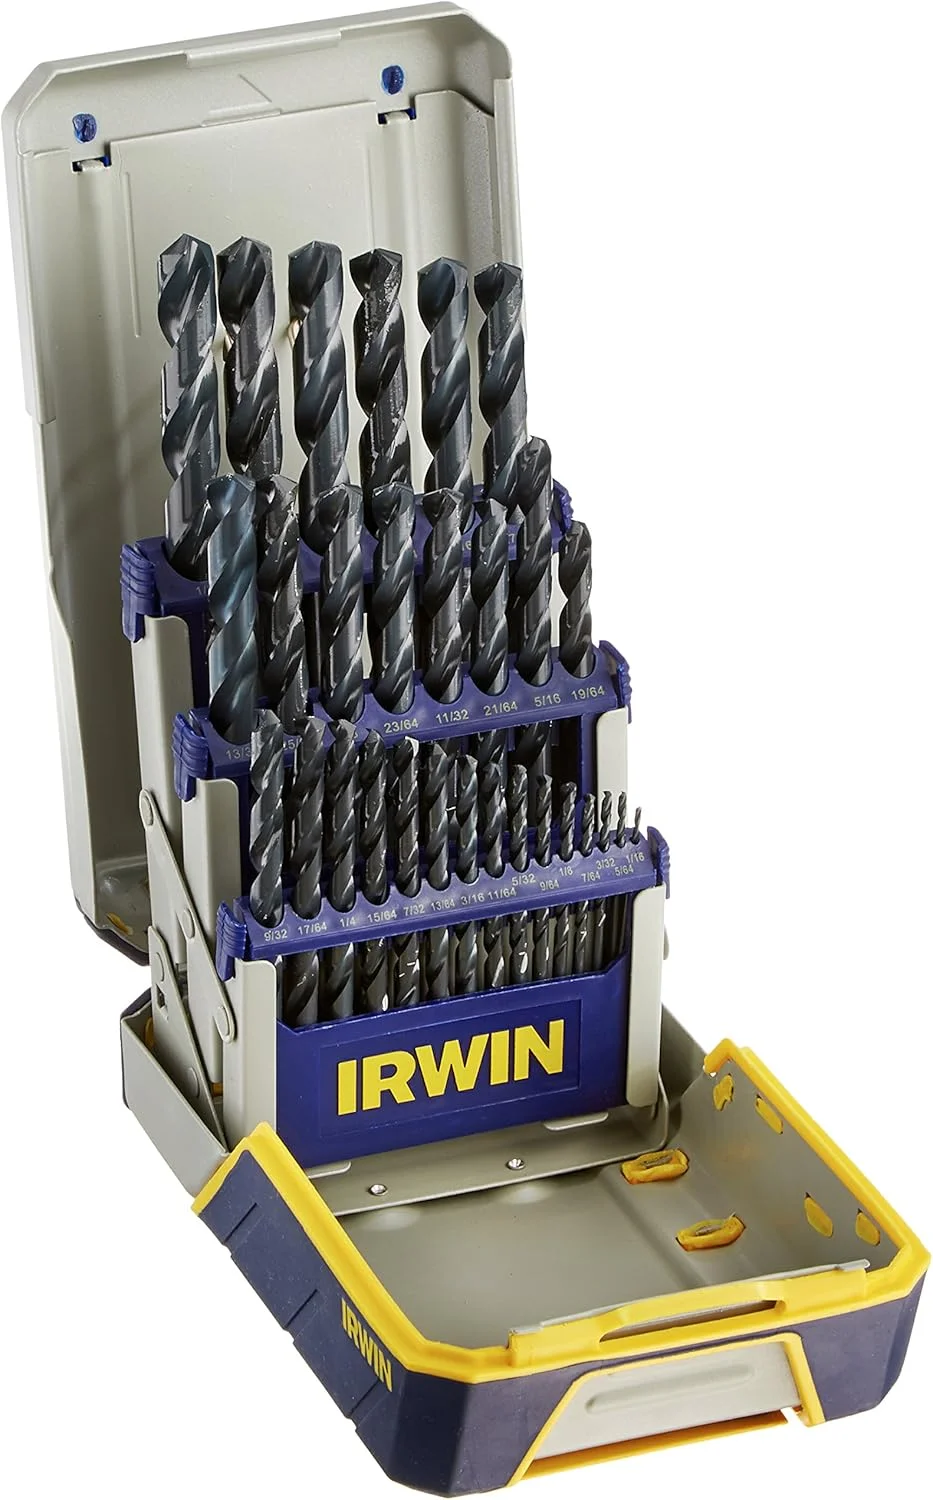
Irwin Metal Drill Bit Set (29 pc)
- Fractional, number, and letter sizes in one index
- Covers the common UNC and UNF tap drills
- Split-point tips for starting a tap hole
Hi-Spec SAE and Metric Tap and Die Set
- Coarse and fine taps for both charts
- Matching dies for chase and repair work
- Shop set for the sizes on this page
Tap Magic EP-Xtra Cutting Fluid
- Cutting fluid for steel and stainless taps
- Helps a 75% hole finish without a broken tap
- 16 oz bottle for the bench
As an Amazon Associate, TestTalkHQ earns from qualifying purchases. Prices and availability may change.

Coarse vs Fine Threads
Coarse and fine threads do not share the same tap drill. The diameter can match while pitch changes the required hole size. Always size from thread and pitch, not diameter alone.
Thread Percentage (50% vs 75% vs 100%)
75% engagement is the practical default for strength and tap life. Higher engagement increases tapping torque sharply and drives more breakage risk.
| Thread Engagement | Strength | Tapping Effort | Typical Use |
|---|---|---|---|
| 50% | Lower | Easy | Soft materials, light duty |
| 75% | High (shop standard) | Moderate | General fabrication and repair |
| 100% | Maximum theoretical | Very high | Special cases, high breakage risk |
Blind Holes, Through Holes, and Tap Type
Blind holes need extra depth for tap lead, chip room, and full thread depth. Through holes are more forgiving for chip evacuation.

Tap Drill Formula
For metric threads, this rule-of-thumb is commonly used directly in mm. For imperial threads, chart values remain the safest shop reference because standard drill increments and engagement targets vary.
Common Tap Drill Mistakes
- Using diameter only and ignoring pitch
- Forcing a tight tap instead of backing out and clearing chips
- No cutting fluid in steel/stainless work
- Starting blind holes with plug or bottoming tap
- Skipping hole chamfer and starting crooked
- Running worn/dull taps too long

When the chart size looked right but the tap still snaps or binds, see Why Is My Tap Breaking? — shared diagnosis for the tapping calculator family.
FAQ
What drill bit do I use for a 1/4-20 tap?
#7, .2010"
What size drill for an M8 tap?
6.8 mm for M8 × 1.25 coarse, 7.0 mm for M8 × 1.0 fine.
What drill bit for a 10-32 tap?
#21, .1590"
What is the tap drill for 3/8-16?
5/16", .3125"
What’s the difference between a tap drill and a clearance drill?
A tap drill is the hole you drill before cutting the thread, sized here for about 75% thread. A clearance drill is the through-hole the screw passes through. Clearance sizes on this chart are close fit.
What does 75% thread mean?
75% thread is the default. It is full strength for most work. In hard material, deep holes, or hand tapping, step up one drill size: less thread engagement, but the tap survives.
How do I calculate metric tap drill size?
Tap drill equals major diameter minus pitch. M8 × 1.25 → 6.8 mm. That shortcut holds all the way down the metric column.
What happens if the tap drill hole is too small?
Tapping torque climbs quickly and tap break risk goes way up.
What happens if the tap drill hole is too large?
Threads can form easily but may strip under load due to lower engagement.
Are tap drill sizes different for stainless steel?
The chart is your baseline. In hard material, deep holes, or hand tapping, step up one drill size so the tap survives.
How deep should I drill for a blind tapped hole?
Deeper than final thread depth to allow for tap lead-in and chip space.
Should I use cutting oil when tapping?
Yes for most metals, especially steel and stainless. Cast iron is often tapped dry.
Conclusion: Drill It Right Before You Tap It
Bolt circles and hole patterns after the tap-drill is chosen: Bolt-Circle / Hole-Pattern Generator.
Tap drill size is the make-or-break step before threading. Use the right chart value for thread and pitch, leave room for chips in blind holes, and do not force taps when resistance spikes.
Machining

Machining Speeds & Feeds Card
One page. Speeds, chip load and drill feed, imperial and metric.
$3.99
Buy
Complete Machining Speeds & Feeds Guide
27 pages. Milling, drilling, tapping, turning and CNC routing.
$12.99
Buy
Machining Job Estimator
Quote shop work and check operations against your spindle's top speed.
Excel or Google Sheets. Best on a computer.
$29.00
Buy
Machining Complete Bundle
Card, 27-page guide and the estimator workbook. All six files.
Excel or Google Sheets. Best on a computer.
$34.99
$45.98 if bought separately — save $10.99
BuyCheckout opens in a new tab.