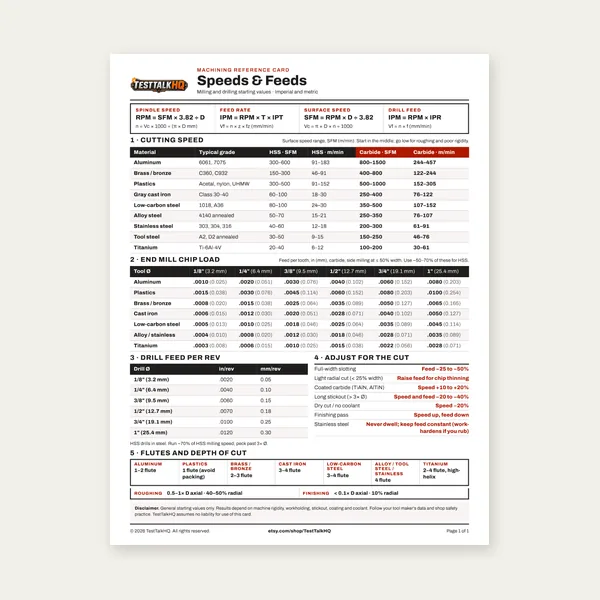
Machining Speeds & Feeds Card
One page. Speeds, chip load and drill feed, imperial and metric.
$3.99
BuyField differentials for oversized and bell-mouthed holes, undersize, chatter, reamer breakage, stock-allowance errors, and material/coolant mismatches — when calculator SFM and feed already looked right
Not a restatement of the guide's speed/feed tables. Pair this with the Reaming Speed and Feed Calculator when RPM, IPR, and stock allowance matched the chart but the hole still failed inspection. For SFM ranges, feed tables, hand vs machine reaming, SFM/RPM lookup, and stock-allowance defaults, use the live Reaming Guide. This page stays on reaming-specific diagnosis forks the guide only sketches.

Use this when predrill looked clean, calculator SFM/IPR were in range, and the reamed hole still failed pin fit, finish spec, or go/no-go. The guide lists fixes; this table splits which failure you have before you change the wrong variable.
| Problem | Field tell | First fix | Next tool |
|---|---|---|---|
| Oversized vs bell-mouthed | Oversized: pin slips, hole mic reads +0.001 to +0.005 over. Bell-mouth: entrance larger than mid-bore; pin binds deep | Oversized → check alignment, dull reamer, excess stock. Bell-mouth → floating holder, reduce feed at entry, square spindle to hole | Reaming Calculator |
| Undersized / tight | Pin won't start; reamer felt "glazed"; witness marks from drill still visible | Too little stock → drill undersized one step, second ream pass. Dull reamer → replace. Low feed rub → increase IPR slightly | Reaming Guide |
| Chatter / poor finish | Helical witness lines, squeal, Ra fails but size may be OK | Drop SFM 15–20%, tighten workholding, verify feed not too low. Check spindle runout before blaming speed | Cutting Speed Troubleshooting |
| Reamer breakage / chipped teeth | Teeth missing at chamfer; sudden stop; reamer stuck in blind hole | Excess stock → smaller predrill. Interrupted cut → spiral flute, slow feed through break. Never peck a chucking reamer like a drill | Drill Speed Troubleshooting |
| SFM looked right, hole still bad | Calculator mid-range but stainless work-hardens, cast scale, or blind chips pack | Verify actual hardness vs chart mild steel. Flood coolant on SS. Blind → spiral flute + withdraw every 0.25–0.5 in | Chip Load Troubleshooting |
| Wrong drill / stock allowance | Used letter drill "close enough"; stock on diameter outside 0.010–0.040 band for size | Recompute predrill = reamer dia − stock mid from calculator. Go smaller on predrill, never larger | Reaming Calculator |
What oversized looks like: Hole mic or pin gauge reads consistently above nominal — often +0.001 to +0.005 in on precision reamers, worse if the reamer is worn. Pin slip fit becomes clearance; press fit won't hold. Surface finish may look acceptable even while size is out.
What bell-mouth looks like: Entrance diameter is larger than mid-bore — common when the reamer enters misaligned or when excess stock forces the chamfer to "dig" at entry. Pin starts easy then binds deep. Bore may still be on size mid-length while failing at the face — a different fix than uniform oversize.
Field differential — oversized causes:
Field differential — bell-mouth causes: Misaligned entry (no float), feed too aggressive first 0.125 in, or pilot hole not deep enough — reamer chamfer cuts only at the face. Fix: reduce feed 30–50% for first half diameter of engagement, use floating holder, ensure predrill depth ≥ reamer length + clearance.
What it looks like: Pin won't enter or needs excessive force. Reamer felt smooth but drill witness marks remain visible in the bore. Go/no-go plug gauge: NO-GO passes but GO won't — or bore reads 0.0005–0.002 in under nominal.
Likely causes:
First fix order: (1) Mic predrill diameter vs required stock. (2) Inspect reamer for BUE or chipped chamfer. (3) Confirm feed isn't below calculator minimum. (4) Only then adjust SFM down 10% steps on scrap.
Undersize after "correct" predrill? Measure stock on diameter, not "felt close" with calipers on the drill shank.
Reaming CalculatorWhat it looks like: Helical or axial witness marks, squeal during cut, surface finish fails Ra spec while diameter may still be in tolerance. On lathe reaming, chatter often shows at the exit where overhang is worst.
Diagnose the cause fork:
Spindle runout and loose Morse taper also masquerade as "speed too high." Indicate the reamer tip at working stick-out before rewriting SFM — overlap with Cutting Speed Troubleshooting for rigidity checks.
What it looks like: Chipped chamfer teeth, reamer seized in blind hole, shank twisted in drill chuck, or carbide flute shattered at keyway cross. Often sudden — no gradual squeal like chatter.
Likely causes:
Predrill quality matters: crooked pilot loads one flute. Check predrill with edge finder or wobble test before blaming feed from the calculator.
What it looks like: Reaming Speed Calculator mid-range SFM and feed, same material name as last good job, but this batch shows work-hardening, torn finish, or size drift. No obvious alignment or stock error.
Material hardness mismatch: "Mild steel" bar from a new supplier at higher CE or cold-drawn skin; 304 vs 316 stainless; heat-treated plate sold as annealed. Chart SFM assumes nominal hardness — actual Brinell 30% higher needs 15–25% lower SFM. Fix: file-test or portable hardness check on scrap; drop to next material tier in calculator.
Coolant / cutting fluid gap: Dry reaming in stainless or tool steel work-hardens within one pass. Aluminum without fluid builds BUE → tight hole. Cast iron often runs dry — oil on CI can cause wheel marks. Match fluid to material per Reaming Guide — calculator shows tips but shop must actually flood the zone.
Peck vs continuous on blind holes: Calculator assumes steady feed. Peck-stop-Peck on manual feed causes work-hardening ring in stainless and chip packing in deep blind holes. Fix: spiral flute, continuous rotation, withdraw every 0.25–0.5 in without stopping spindle; compressed air after withdraw. Chip evacuation issues overlap Chip Load Troubleshooting.
Machine vs hand reamer type: Calculator warns on hand reamer selection — running hand-reamer SFM on a chucking reamer in power equipment destroys the hole and tool even when "RPM was in range."
What it looks like: Operator picked "one drill smaller than reamer" from habit, used a tap-drill chart, or letter/fractional drill "close enough." Stock on diameter lands outside the 0.010–0.040 in band (size-dependent). Either breakage/oversize (too much stock) or tight/witness marks (too little).
Stock allowance rules (on diameter — not radius):
| Reamer diameter | Stock on diameter | Predrill ≈ |
|---|---|---|
| Under 1/4 in | 0.010–0.015 in | Reamer dia − 0.012 in |
| 1/4 to 1/2 in | 0.015–0.020 in | Reamer dia − 0.018 in |
| 1/2 to 1 in | 0.020–0.030 in | Reamer dia − 0.025 in |
| Over 1 in | 0.030–0.040 in | Reamer dia − 0.035 in |
Full tables and feed IPR by diameter live in the Reaming Guide — not duplicated here. Use the Reaming Speed Calculator for exact predrill on your diameter.
Common drill-size mistakes:
Predrill accuracy ties to Drill Speed Troubleshooting when the pilot itself is oversize or crooked before reaming starts.
Article 3 live: Hand Reaming vs Machine Reaming — Which to Use — field one-offs vs production chucking, flute choice, and wrong-tool failure modes. This troubleshooting page stays on diagnosis when calculator numbers already matched. Speed/feed tables: Reaming Guide.
Hand vs Machine Reaming → Reaming Speed Calculator → Reaming Guide → Drill Speed Troubleshooting → Cutting Speed Troubleshooting →
One page. Speeds, chip load and drill feed, imperial and metric.
$3.99
Buy
27 pages. Milling, drilling, tapping, turning and CNC routing.
$12.99
Buy
Quote shop work and check operations against your spindle's top speed.
Excel or Google Sheets. Best on a computer.
$29.00
Buy
Card, 27-page guide and the estimator workbook. All six files.
Excel or Google Sheets. Best on a computer.
$34.99
$45.98 if bought separately — save $10.99
BuyCheckout opens in a new tab.
Five CSV catalog picks with verified Product Image URLs — measure, align, fluid, and shop safety
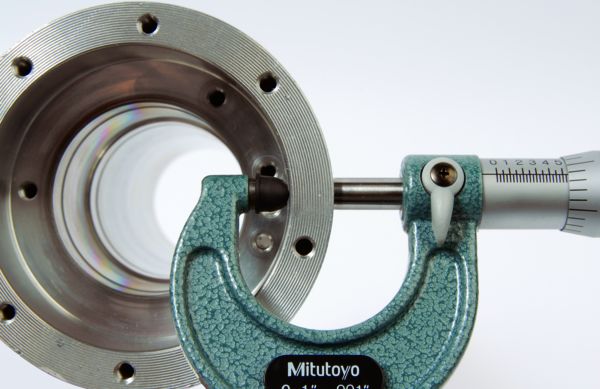
As an Amazon Associate, TestTalkHQ earns from qualifying purchases. All five cards are sourced only from the affiliate CSV with verified Product Image URLs. Catalog gaps flagged by name: HSS chucking reamers; adjustable hand reamer sets; machine reamer sets; drill chucks; floating reamer holders; dial bore gauges; telescoping pin gauges; SHARS wiggler sets (no image in CSV); Klein Tools 60171 Safety Glasses (CSV Geniuslink URL returns 404).
The guide lists likely cause and fix in one row each. This page splits failures by field presentation — bell-mouth vs uniform oversize, rub-induced undersize vs dull tool, rigidity vs SFM on chatter — and ties them to measurement and alignment checks when calculator numbers already matched.
Alignment (floating holder), worn reamer diameter, excess stock, and spindle runout override chart SFM. Measure entrance vs mid-bore and mic the predrill before changing RPM.
Not first. Confirm stick-out, workholding, and feed — then drop SFM 15–20%. Chatter with on-size bore is often rigidity, not speed.
Best catalog matches (HSS chucking reamers, adjustable hand sets, spiral-flute carbide) lack Product Image URLs in the affiliate CSV — flagged as catalog gaps instead of mismatched photos.
Hand vs machine decision: Hand Reaming vs Machine Reaming — Which to Use. Stock/SFM/IPR tables: Reaming Guide. Starting numbers: Reaming Speed Calculator.