
Machining Speeds & Feeds Card
One page. Speeds, chip load and drill feed, imperial and metric.
$3.99
BuyEstimated threading torque by size, material, and tap style
Plan how much twist your tap needs — separate from tap drill diameter and tapping RPM. Useful for choosing a tap wrench, setting a drill-press clutch, or sizing a tapping attachment. Results are planning estimates, not precision engineering values.

One page. Speeds, chip load and drill feed, imperial and metric.
$3.99
Buy
27 pages. Milling, drilling, tapping, turning and CNC routing.
$12.99
Buy
Quote shop work and check operations against your spindle's top speed.
Excel or Google Sheets. Best on a computer.
$29.00
Buy
Card, 27-page guide and the estimator workbook. All six files.
Excel or Google Sheets. Best on a computer.
$34.99
$45.98 if bought separately — save $10.99
BuyCheckout opens in a new tab.
Hole prep, cutting fluid, and torque-rated wrenches for hand tapping and drill-press work.

As an Amazon Associate, TestTalkHQ earns from qualifying purchases. Prices and availability subject to change.
This tool estimates cutting torque at the tap — how much twist the tap needs to form threads. That is separate from the Tap Drill Size Calculator (correct hole diameter before tapping) and the Tapping Speed Calculator (RPM and SFM). Use all three: drill the right hole, run the right speed, and know whether your tap wrench, drill-press clutch, or tapping head can handle the expected torque.
Real tapping torque swings with tap sharpness, coating, hole depth, thread percentage, cutting fluid, and whether chips pack in a blind hole. Treat the result as a planning band for selecting a tap wrench size, setting a drill-press clutch, or comparing materials — not a torque wrench setpoint for production QC.
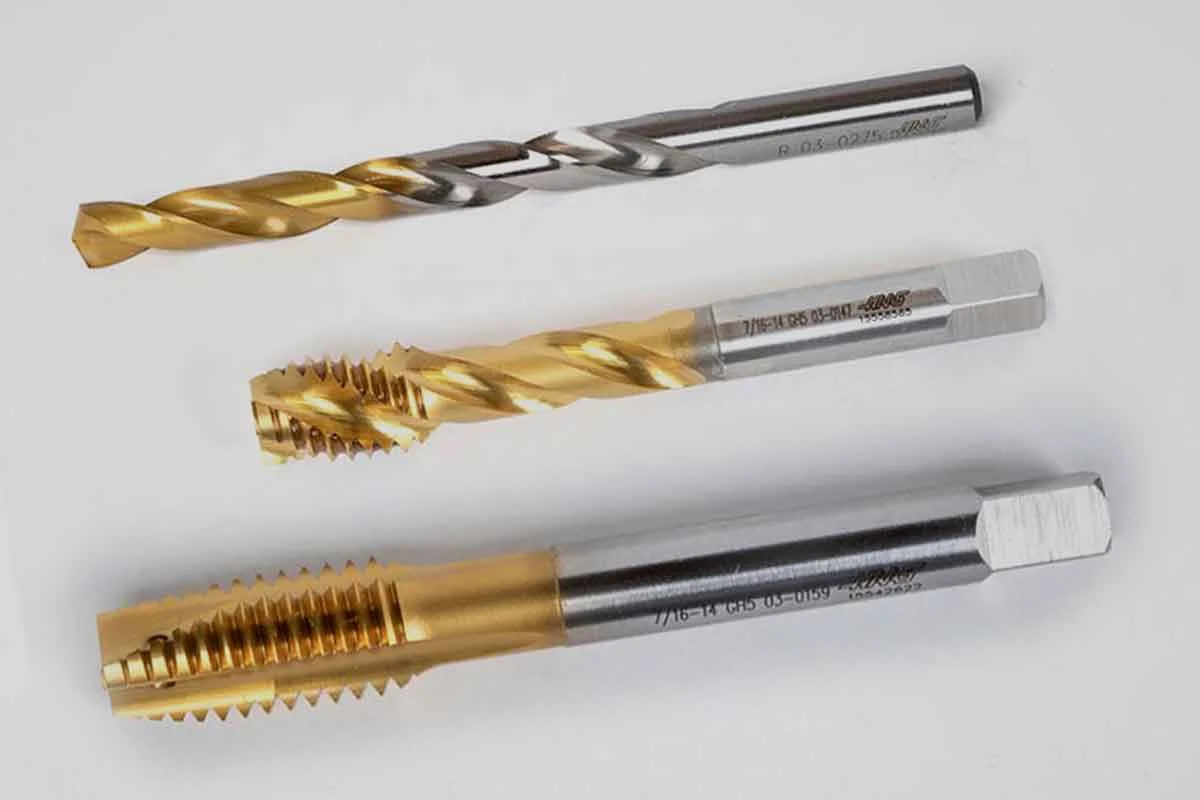
Spiral point (gun) taps push chips forward and usually need less torque in through holes. Spiral flute taps pull chips out of blind holes — baseline torque in the model. Straight flute hand taps pack chips more easily and often feel tighter, especially deep or in blind holes. Match tap geometry to the hole before you worry about the last 10 in-lb on the wrench.