A two-stage method straight out of the Copper Tube Handbook — what the run actually moves, what has to be in the way to absorb it, and the anchor decision that makes or wastes the whole thing
It is two calculations, and they use different inputs
Almost every argument about expansion loops is really two questions mashed together. Separate them and the whole subject gets straightforward:
- How far does this run move? That depends on the length of the run and the temperature change. It does not depend on the diameter at all.
- What has to be in the way to absorb that movement? That depends on the diameter, the stiffness of the material and how hard you are willing to bend it. It does not depend on the length of the run except through the answer to question one.
The Copper Development Association gives you a published method for both halves, in the same two pages of the Copper Tube Handbook. The handbook is also blunt about what happens if you skip them: “in a copper tube system subjected to excessive temperature changes, a long line tends to buckle or bend when it expands unless compensation is built into the system. Severe stresses on the joints may also occur.”
Buckle, bend, or stress the joints. Those are the three failure modes, and they are exactly what the troubleshooting companion to this article works backwards from.
Stage one: how far the run moves
The handbook writes it as a chain of multiplications rather than as an equation, which is actually how you use it on site:
The coefficient is the only thing you have to look up, and the handbook gives it plainly: “calculation for expansion and contraction should be based on the average coefficient of expansion of copper which is 0.0000094 inch per inch per degree F, between 70°F and 212°F.” Note the window on the end of that sentence — it is an average over 70 to 212°F, and below or above that range you are extending a figure beyond what was published.
The handbook then works its own example, which is the one worth memorising: “the expansion of each 100 feet of length of any size tube heated from room temperature (70°F) to 170°F (a 100°F rise) is 1.128 inches.”
100 × 100 × 12 × 0.0000094 = 1.128. That is the whole of stage one.
What that looks like on real runs
| Temperature change | Typical job | Per 25 ft | Per 50 ft | Per 100 ft |
|---|---|---|---|---|
| 50°F | Cold main warming to room temperature | 0.141 in | 0.282 in | 0.564 in |
| 70°F | 70 to 140°F domestic hot water | 0.197 in | 0.395 in | 0.790 in |
| 85°F | 55°F crawl space to a 140°F recirculation return | 0.240 in | 0.479 in | 0.959 in |
| 110°F | 70 to 180°F hydronic heating | 0.310 in | 0.620 in | 1.241 in |
| 130°F | 70 to 200°F heating main | 0.367 in | 0.733 in | 1.466 in |
Two readings worth taking from that table. First, a 50-foot hydronic main moves about five eighths of an inch, which is far more than any solder joint wants to absorb in bending. Second, the most dangerous row is not the hottest one — it is the recirculation row, because that is the case people do not think of as a heating system at all.
Why diameter is missing from stage one and central to stage two
The handbook says the expansion is the same “for any size tube”, and that is worth sitting with for a second because it contradicts most people’s intuition. A ½ in branch and a 4 in main running side by side in the same ceiling, over the same length, on the same temperature swing, grow by exactly the same number of inches.
What changes with diameter is how hard the tube is to bend out of the way. Forcing a quarter inch of deflection into ½ in tube is easy; forcing it into 4 in tube puts an enormous bending stress into the wall. That is the entire content of stage two: how long a piece of tube do you need so that the deflection you are forcing on it stays inside an allowable bending stress.
Stage two: the loop formula, and where 7.68 comes from
The handbook gives the loop formula in general form, with no copper in it:
L = (1/12) √( 3 E (do e) / P )
with the handbook’s own definitions: L is the developed length in feet in the expansion loop or offset, E the modulus of elasticity in psi, P the design allowable fiber stress of the material in flexure in psi, do the outside diameter in inches, and e the amount of expansion to be absorbed in inches.
Then it substitutes copper: “For annealed copper tube: E = 17,000,000 psi, P = 6,000 psi. Thus, the developed length L is simply: L = 7.68 (do e)½”
That shortcut is worth checking once, because once you have checked it you know that those two constants are the only copper-specific content in the formula:
√(3 × 17,000,000 ÷ 6,000) = √8,500 = 92.195, and 92.195 ÷ 12 = 7.6830.
Outside diameter, not nominal size
The do in that formula is the real outside diameter, and copper water tube is the classic case where the nominal size is not a dimension of anything. Copper tube outside diameter is the nominal size plus ⅛ inch: ½ in tube is 0.625 in outside, ¾ in is 0.875 in, 2 in is 2.125 in. Types K, L and M all share that outside diameter at each size — which is why the same fittings fit all three — and since wall thickness never appears in the loop formula, the tube type makes no difference to the loop length at all. It makes a great deal of difference to the pressure rating, which is a separate calculation.
Any trade
Contractor Job Estimator
Price remodels and GC work, then send a quote with no internal numbers.
Excel or Google Sheets. Best on a computer.
$29.00
BuyCheckout opens in a new tab.
The two inputs people guess, and the tools that stop them guessing
Of the four things that set the movement, two are temperatures, and on most jobs both are assumed rather than measured. An assumed 140°F against an actual 180°F is a third more movement, which is a third more loop. These are the instruments that replace the assumption, and the tools for the physical half of the work.
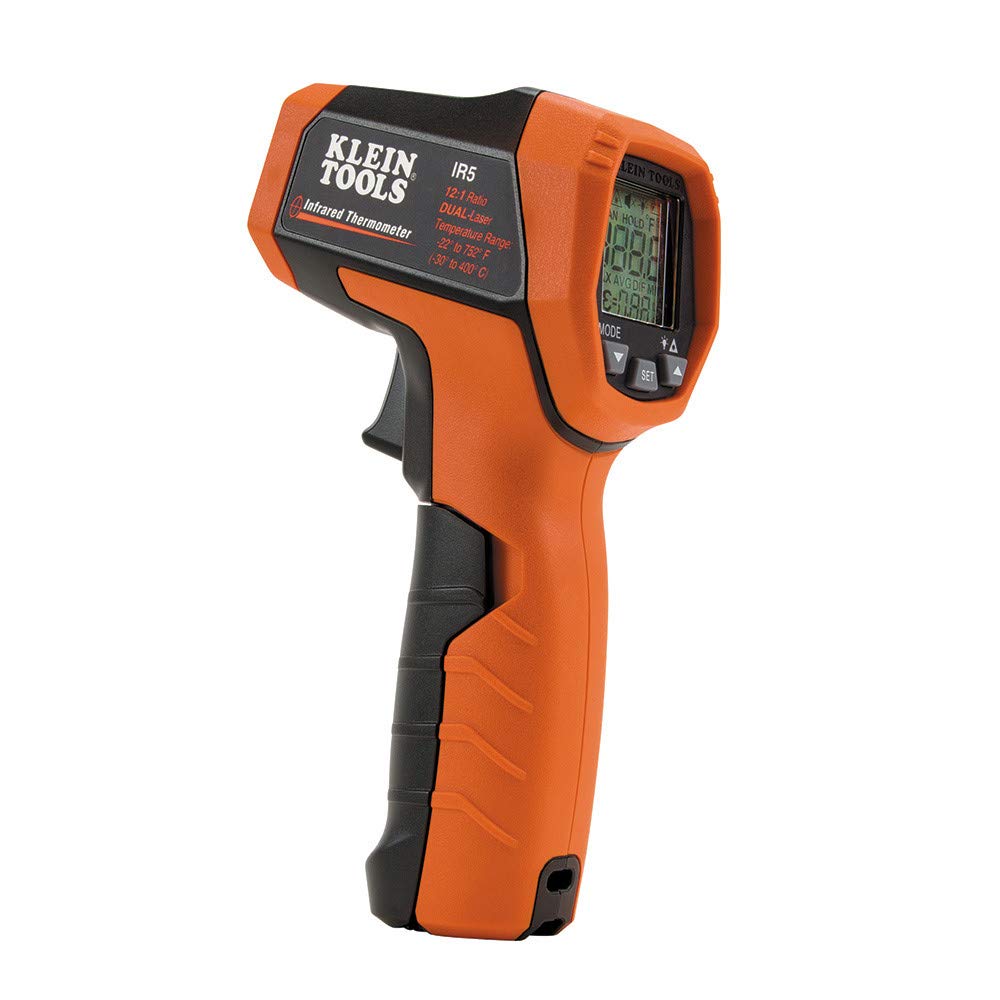
Klein Tools IR5 Dual‑Laser Infrared Thermometer
- Reads the tube surface, which is the number the calculation wants
- Dual laser frames the spot, so you measure pipe and not insulation
- Catches the case people miss: a recirculation return near supply temperature all day
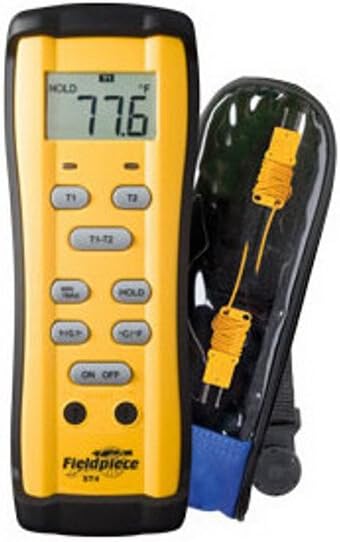
Fieldpiece ST4 Dual Temperature Meter
- Two clamp probes give the real swing across a run, not one snapshot
- Log the cold start and the hot running condition on the same line
- The honest way to replace an assumed 70°F installation temperature
RIDGID 32573 Model 118 Close‑Quarters Tubing Cutter
- Square cuts on the legs of an offset, in the joist bay where it has to go
- Built-in reamer, because a burr inside a bend is a velocity problem later
- Close-quarters body for the tight retrofit a loop always turns into
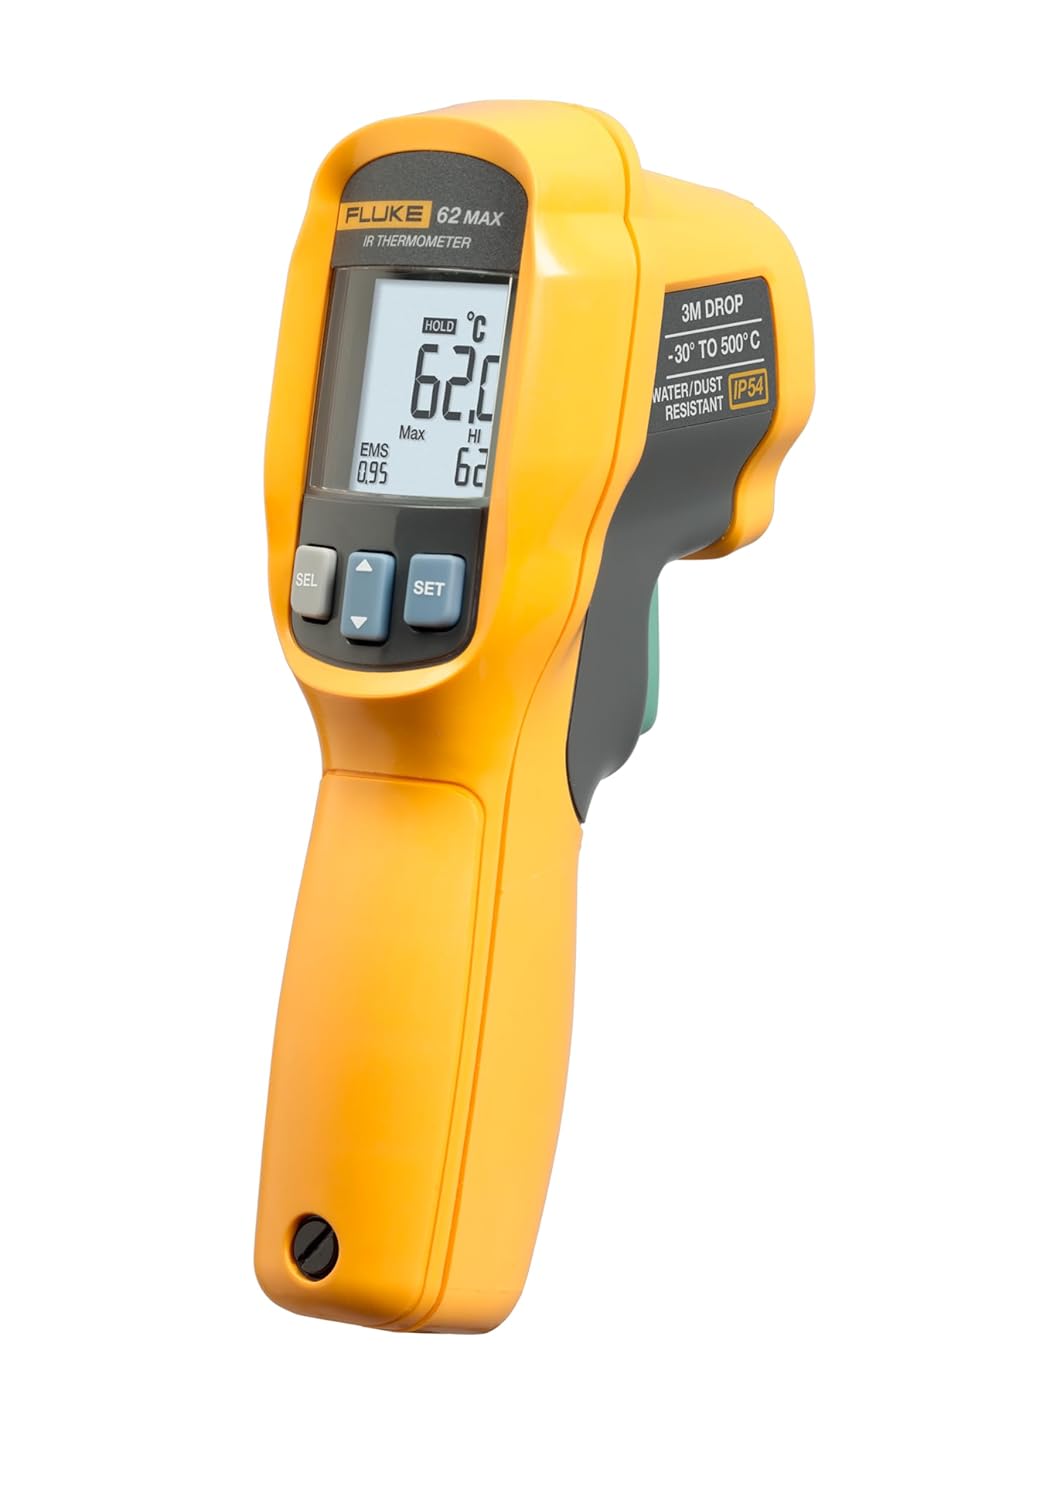
Fluke 62 Max Industrial Infrared Thermometer
- Range and accuracy for the 180°F+ mains where movement gets serious
- Drop rated for the plant room rather than the job box
- Narrow spot ratio, so you read the tube and not the lagging beside it
Oatey 29024 Safe‑Flo Lead‑Free Solder
- Lead-free, for the elbows an offset adds to a potable line
- Fewer and better joints inside a loop: every one is a stress riser
- The alloy the published potable joint ratings assume
As an Amazon Associate, TestTalkHQ earns from qualifying purchases. Prices and availability can change.
Coil or offset: Table 14.8 gives you the same number twice
Alongside the formula the handbook publishes Table 14.8, Radii of Coiled Expansion Loops and Developed Lengths of Expansion Offsets: eight rows of expected expansion from ½ in to 4 in, against thirteen nominal sizes from ¼ in to 5 in. Each cell gives a radius R and a developed length L. The surrounding text explains which is which: “Tables 14.8 gives the radii necessary for coiled expansion loops, described in Figure 14.3. Expansion offset lengths may be estimated from Tables 14.8.”
So: if you are rolling a coiled loop, read the radius. If you are building an expansion offset — a U-bend, a dogleg, two 90s with a leg between them — read the developed length and distribute it over your geometry.
Here is the part that is not written down anywhere in the handbook but falls straight out of the table: those two numbers are the same number in two forms. The coiled loop is a complete circle, so its circumference is the developed length, which means
R = L ÷ 2π
Check it on any cell. For 1 in tube at the 1 in expansion step the table gives L = 94 in and R = 15 in; 94 ÷ 6.283 = 14.96. Check it on all 104 cells and no pair is out by more than the rounding of R to the nearest whole inch. That relationship is how you convert a developed length from the formula into a radius you can actually roll a coil to.
The formula and the table disagree by about 4 percent, always the same way
The handbook presents the formula as the alternative to the table — “alternatively, the necessary length of tube in an expansion loop or offset can be calculated using the formula” — which implies they should agree. Run both at every one of the 104 published cells and they do not, quite:
| Nominal size | Expansion | Table 14.8 L | Formula L | Formula is |
|---|---|---|---|---|
| ½ in | 1 in | 70 in | 72.9 in | +4.1% |
| 1 in | 1 in | 94 in | 97.8 in | +4.0% |
| 2 in | 2 in | 183 in | 190.1 in | +3.9% |
| 4 in | 4 in | 361 in | 374.5 in | +3.7% |
Across all 104 cells the formula asks for between 3.1 and 5.1 percent more tube than the table, averaging 3.9 percent, and it is never shorter. Solve the formula backwards for the fiber stress the table cells imply and the reason appears: the table behaves as though P ≈ 6,480 psi — a narrow band from 6,375 to 6,622 across every cell — rather than the 6,000 psi printed with the formula. Put 6480 into the allowable fiber stress field on the calculator and the two routes land within a tenth of a percent of each other.
What to do about it: build to the longer figure. The difference is a couple of inches on a domestic branch and about a foot on a large main, and nobody has ever been called back because a loop had four percent more tube in it than it strictly needed.
Run your own numbers. The copper pipe expansion loop calculator takes the size, the run between anchors and the two temperatures, and returns the movement, the developed length the CDA formula requires, the coil radius to roll it to, the published Table 14.8 figure beside it and the support spacing for the run.
The anchor decision is the real input, and it is usually never made
Every number above describes a length of tube held at both ends. Which means the single most consequential thing on the job is where those two ends are, and on a great many installations nobody ever decided.
| Component | What it does | Effect on the calculation |
|---|---|---|
| Anchor | Clamps the tube and transfers the load into the structure. Stops it dead. | Defines the ends of the run. All movement between two anchors must be absorbed between them. |
| Guide / support | Carries the weight and keeps the line straight while letting it slide lengthways. | None, as long as it really does let the tube slide. |
| Accidental anchor | A strap pulled tight, a pipe grouted into a wall, a hole the same size as the tube, a fitting hard against a joist. | Behaves exactly like a designed anchor, except nobody calculated for it. Usually the cause of the failure. |
The handbook’s support intervals are intervals for guides: “unless otherwise stated in plumbing codes, drawn temper tube requires support for horizontal lines at about 8-foot intervals for sizes of 1-inch and smaller, and at about 10-foot intervals for larger sizes. Vertical lines are usually supported at every story or at about 10-foot intervals.” Annealed coil gets support at least every 8 feet horizontally and 10 feet vertically.
On tall buildings the handbook adds the detail that actually matters: “for long lines where there are the usual provisions for expansion and contraction, anchors may be several stories apart, provided there are sleeves or similar devices at all intermediate floors to restrain lateral movement.” Sleeves restrain the pipe sideways without gripping it lengthways. That is the distinction in one sentence.
Six runs worked from end to end
All six use the published coefficient and the published formula with the handbook’s annealed constants, and each shows the Table 14.8 cell at the step the movement lands on.
| Run | ΔT | Movement | Formula L | Coil R | Table 14.8 step | Table L / R |
|---|---|---|---|---|---|---|
| ½ in hot branch, 25 ft, 70→140°F | 70°F | 0.197 in | 2.70 ft | 5.2 in | ½ in | 50 in / 8 in |
| ¾ in hot main, 40 ft, 70→140°F | 70°F | 0.316 in | 4.04 ft | 7.7 in | ½ in | 59 in / 9 in |
| ¾ in recirc return, 60 ft, 55→140°F | 85°F | 0.575 in | 5.45 ft | 10.4 in | 1 in | 83 in / 13 in |
| 1 in hydronic main, 60 ft, 70→180°F | 110°F | 0.744 in | 7.03 ft | 13.4 in | 1 in | 94 in / 15 in |
| 1½ in hydronic main, 90 ft, 70→180°F | 110°F | 1.117 in | 10.35 ft | 19.8 in | 1½ in | 138 in / 22 in |
| 2 in heating main, 100 ft, 70→200°F | 130°F | 1.466 in | 13.56 ft | 25.9 in | 1½ in | 158 in / 25 in |
Things to notice walking down that table. The ½ in branch at the top needs under three feet of developed length, which a single change of direction in the run may already provide — that is a case where you look at the layout before you build anything. The two ¾ in rows differ only in run length and ambient temperature, and the recirculation return needs 35 percent more loop than the hot main above it. By the time you reach the 2 in commercial run at the bottom, the answer is thirteen and a half feet of tube, and the honest reaction to that number is to go back and ask whether the run can be anchored in the middle instead.
Four things this method deliberately does not tell you
- There is no threshold below which you can skip compensation, because the handbook publishes none. No run length, no temperature rise, no amount of movement. Several genuinely different cases exist — a run anchored at one end and free at the other simply moves and needs nothing, and a run with changes of direction already in it may have adequate natural flexibility — and deciding which case you are in belongs to the designer and the authority having jurisdiction. Any web page that gives you a confident “under 20 feet you are fine” rule is making it up.
- It is not a force calculation. How much thrust a restrained run puts into an anchor is a restraint analysis, and it is the number a structural engineer wants before you bolt a 4 in main to a block wall. The handbook does not provide it and neither does this method.
- It is copper only. PEX, CPVC, PVC and PE all move several times as far per degree, so the very first multiplication would be wrong, let alone the constants in the loop formula. Those manufacturers publish their own expansion and offset data for their own products, and that is what you use.
- Pipe movement is not water expansion. Heating trapped water in a closed system raises pressure rather than length — that is an expansion tank and relief valve question. The two get confused constantly because they share a word, and a system can easily have one problem without the other.
If what you actually have is a line that is already making noise, bowing, or weeping at a fitting, the diagnostic path is in when a copper line ticks, bows or splits a joint. If you have the movement figure and now need to choose the hardware, that is loop, offset, expansion joint or swing arm.