Drill Bit Size Conversion Chart
Fractional · Number · Letter · Metric — decimal and mm equivalents
Four naming systems, one reference. Convert fractional, number, letter, and metric drill bits so you can match the size on the print to the bit in your set.

How to Use This Chart
Drill bits are sold in four naming systems: fractional inch, number (wire gauge), letter, and metric millimeters. This page converts between them so you can pick the closest bit you actually have in the drawer. Nearest-size columns show the closest match within about 0.0025 in — a dash means nothing in that system is that close.
For tap pilot holes, start with the Tap Drill Size Calculator, then confirm the named bit here. For RPM once you know diameter, use the Drill Speed Calculator.
After you pick the size, set RPM — and if the hole still fails at “correct” speed, use Drill Speed Troubleshooting.
Fractional Inch Drill Bit Chart
Standard fractional sizes from 1/64 through 1 inch, with decimal, metric, and nearest number/letter equivalents.
| Fractional | Decimal (in) | Metric (mm) | Nearest Number | Nearest Letter |
|---|---|---|---|---|
| 1/64 | 0.0156 | 0.397 | #78 | — |
| 1/32 | 0.0312 | 0.794 | #68 | — |
| 3/64 | 0.0469 | 1.191 | #56 | — |
| 1/16 | 0.0625 | 1.587 | #52 | — |
| 5/64 | 0.0781 | 1.984 | #47 | — |
| 3/32 | 0.0938 | 2.381 | #42 | — |
| 7/64 | 0.1094 | 2.778 | #35 | — |
| 1/8 | 0.1250 | 3.175 | — | — |
| 9/64 | 0.1406 | 3.572 | #28 | — |
| 5/32 | 0.1562 | 3.969 | #22 | — |
| 11/64 | 0.1719 | 4.366 | #17 | — |
| 3/16 | 0.1875 | 4.762 | #12 | — |
| 13/64 | 0.2031 | 5.159 | #6 | — |
| 7/32 | 0.2188 | 5.556 | #2 | — |
| 15/64 | 0.2344 | 5.953 | — | A |
| 1/4 | 0.2500 | 6.350 | — | E |
| 17/64 | 0.2656 | 6.747 | — | H |
| 9/32 | 0.2812 | 7.144 | — | K |
| 19/64 | 0.2969 | 7.541 | — | M |
| 5/16 | 0.3125 | 7.938 | — | — |
| 21/64 | 0.3281 | 8.334 | — | — |
| 11/32 | 0.3438 | 8.731 | — | — |
| 23/64 | 0.3594 | 9.128 | — | T |
| 3/8 | 0.3750 | 9.525 | — | V |
| 25/64 | 0.3906 | 9.922 | — | — |
| 13/32 | 0.4062 | 10.319 | — | Y |
| 27/64 | 0.4219 | 10.716 | — | — |
| 7/16 | 0.4375 | 11.112 | — | — |
| 29/64 | 0.4531 | 11.509 | — | — |
| 15/32 | 0.4688 | 11.906 | — | — |
| 31/64 | 0.4844 | 12.303 | — | — |
| 1/2 | 0.5000 | 12.700 | — | — |
| 33/64 | 0.5156 | 13.097 | — | — |
| 17/32 | 0.5312 | 13.494 | — | — |
| 35/64 | 0.5469 | 13.891 | — | — |
| 9/16 | 0.5625 | 14.287 | — | — |
| 37/64 | 0.5781 | 14.684 | — | — |
| 19/32 | 0.5938 | 15.081 | — | — |
| 39/64 | 0.6094 | 15.478 | — | — |
| 5/8 | 0.6250 | 15.875 | — | — |
| 41/64 | 0.6406 | 16.272 | — | — |
| 21/32 | 0.6562 | 16.669 | — | — |
| 43/64 | 0.6719 | 17.066 | — | — |
| 11/16 | 0.6875 | 17.462 | — | — |
| 45/64 | 0.7031 | 17.859 | — | — |
| 23/32 | 0.7188 | 18.256 | — | — |
| 47/64 | 0.7344 | 18.653 | — | — |
| 3/4 | 0.7500 | 19.050 | — | — |
| 49/64 | 0.7656 | 19.447 | — | — |
| 25/32 | 0.7812 | 19.844 | — | — |
| 51/64 | 0.7969 | 20.241 | — | — |
| 13/16 | 0.8125 | 20.637 | — | — |
| 53/64 | 0.8281 | 21.034 | — | — |
| 27/32 | 0.8438 | 21.431 | — | — |
| 55/64 | 0.8594 | 21.828 | — | — |
| 7/8 | 0.8750 | 22.225 | — | — |
| 57/64 | 0.8906 | 22.622 | — | — |
| 29/32 | 0.9062 | 23.019 | — | — |
| 59/64 | 0.9219 | 23.416 | — | — |
| 15/16 | 0.9375 | 23.812 | — | — |
| 61/64 | 0.9531 | 24.209 | — | — |
| 31/32 | 0.9688 | 24.606 | — | — |
| 63/64 | 0.9844 | 25.003 | — | — |
| 1/1 | 1.0000 | 25.400 | — | — |
Fractional sets are the most common in North American fab shops. Many “29-piece” sets cover 1/16 through 1/2 by 64ths.
Number (Wire Gauge) Drill Bit Chart
Number drills #80 (smallest) through #1. These fill the gaps between fractional sizes and are critical for tap drill work.
| Number | Decimal (in) | Metric (mm) | Nearest Fractional | Nearest Letter |
|---|---|---|---|---|
| #80 | 0.0135 | 0.343 | 1/64 | — |
| #79 | 0.0145 | 0.368 | 1/64 | — |
| #78 | 0.0160 | 0.406 | 1/64 | — |
| #77 | 0.0180 | 0.457 | 1/64 | — |
| #76 | 0.0200 | 0.508 | — | — |
| #75 | 0.0210 | 0.533 | — | — |
| #74 | 0.0225 | 0.571 | — | — |
| #73 | 0.0240 | 0.610 | — | — |
| #72 | 0.0250 | 0.635 | — | — |
| #71 | 0.0260 | 0.660 | — | — |
| #70 | 0.0280 | 0.711 | — | — |
| #69 | 0.0292 | 0.742 | 1/32 | — |
| #68 | 0.0310 | 0.787 | 1/32 | — |
| #67 | 0.0320 | 0.813 | 1/32 | — |
| #66 | 0.0330 | 0.838 | 1/32 | — |
| #65 | 0.0350 | 0.889 | — | — |
| #64 | 0.0360 | 0.914 | — | — |
| #63 | 0.0370 | 0.940 | — | — |
| #62 | 0.0380 | 0.965 | — | — |
| #61 | 0.0390 | 0.991 | — | — |
| #60 | 0.0400 | 1.016 | — | — |
| #59 | 0.0410 | 1.041 | — | — |
| #58 | 0.0420 | 1.067 | — | — |
| #57 | 0.0430 | 1.092 | — | — |
| #56 | 0.0465 | 1.181 | 3/64 | — |
| #55 | 0.0520 | 1.321 | — | — |
| #54 | 0.0550 | 1.397 | — | — |
| #53 | 0.0595 | 1.511 | — | — |
| #52 | 0.0635 | 1.613 | 1/16 | — |
| #51 | 0.0670 | 1.702 | — | — |
| #50 | 0.0700 | 1.778 | — | — |
| #49 | 0.0730 | 1.854 | — | — |
| #48 | 0.0760 | 1.930 | 5/64 | — |
| #47 | 0.0785 | 1.994 | 5/64 | — |
| #46 | 0.0810 | 2.057 | — | — |
| #45 | 0.0820 | 2.083 | — | — |
| #44 | 0.0860 | 2.184 | — | — |
| #43 | 0.0890 | 2.261 | — | — |
| #42 | 0.0935 | 2.375 | 3/32 | — |
| #41 | 0.0960 | 2.438 | 3/32 | — |
| #40 | 0.0980 | 2.489 | — | — |
| #39 | 0.0995 | 2.527 | — | — |
| #38 | 0.1015 | 2.578 | — | — |
| #37 | 0.1040 | 2.642 | — | — |
| #36 | 0.1065 | 2.705 | — | — |
| #35 | 0.1100 | 2.794 | 7/64 | — |
| #34 | 0.1110 | 2.819 | 7/64 | — |
| #33 | 0.1130 | 2.870 | — | — |
| #32 | 0.1160 | 2.946 | — | — |
| #31 | 0.1200 | 3.048 | — | — |
| #30 | 0.1285 | 3.264 | — | — |
| #29 | 0.1360 | 3.454 | — | — |
| #28 | 0.1405 | 3.569 | 9/64 | — |
| #27 | 0.1440 | 3.658 | — | — |
| #26 | 0.1470 | 3.734 | — | — |
| #25 | 0.1495 | 3.797 | — | — |
| #24 | 0.1520 | 3.861 | — | — |
| #23 | 0.1540 | 3.912 | 5/32 | — |
| #22 | 0.1570 | 3.988 | 5/32 | — |
| #21 | 0.1590 | 4.039 | — | — |
| #20 | 0.1610 | 4.089 | — | — |
| #19 | 0.1660 | 4.216 | — | — |
| #18 | 0.1695 | 4.305 | 11/64 | — |
| #17 | 0.1730 | 4.394 | 11/64 | — |
| #16 | 0.1770 | 4.496 | — | — |
| #15 | 0.1800 | 4.572 | — | — |
| #14 | 0.1820 | 4.623 | — | — |
| #13 | 0.1850 | 4.699 | — | — |
| #12 | 0.1890 | 4.801 | 3/16 | — |
| #11 | 0.1910 | 4.851 | — | — |
| #10 | 0.1935 | 4.915 | — | — |
| #9 | 0.1960 | 4.978 | — | — |
| #8 | 0.1990 | 5.055 | — | — |
| #7 | 0.2010 | 5.105 | 13/64 | — |
| #6 | 0.2040 | 5.182 | 13/64 | — |
| #5 | 0.2055 | 5.220 | 13/64 | — |
| #4 | 0.2090 | 5.309 | — | — |
| #3 | 0.2130 | 5.410 | — | — |
| #2 | 0.2210 | 5.613 | 7/32 | — |
| #1 | 0.2280 | 5.791 | — | — |
#7 (0.2010 in) and #21 (0.1590 in) are among the most-used tap-drill sizes for UNC/UNF work.
Recommended Drill Bits & Shop Tools
Fractional, number, and letter sets for matching the sizes in this chart.
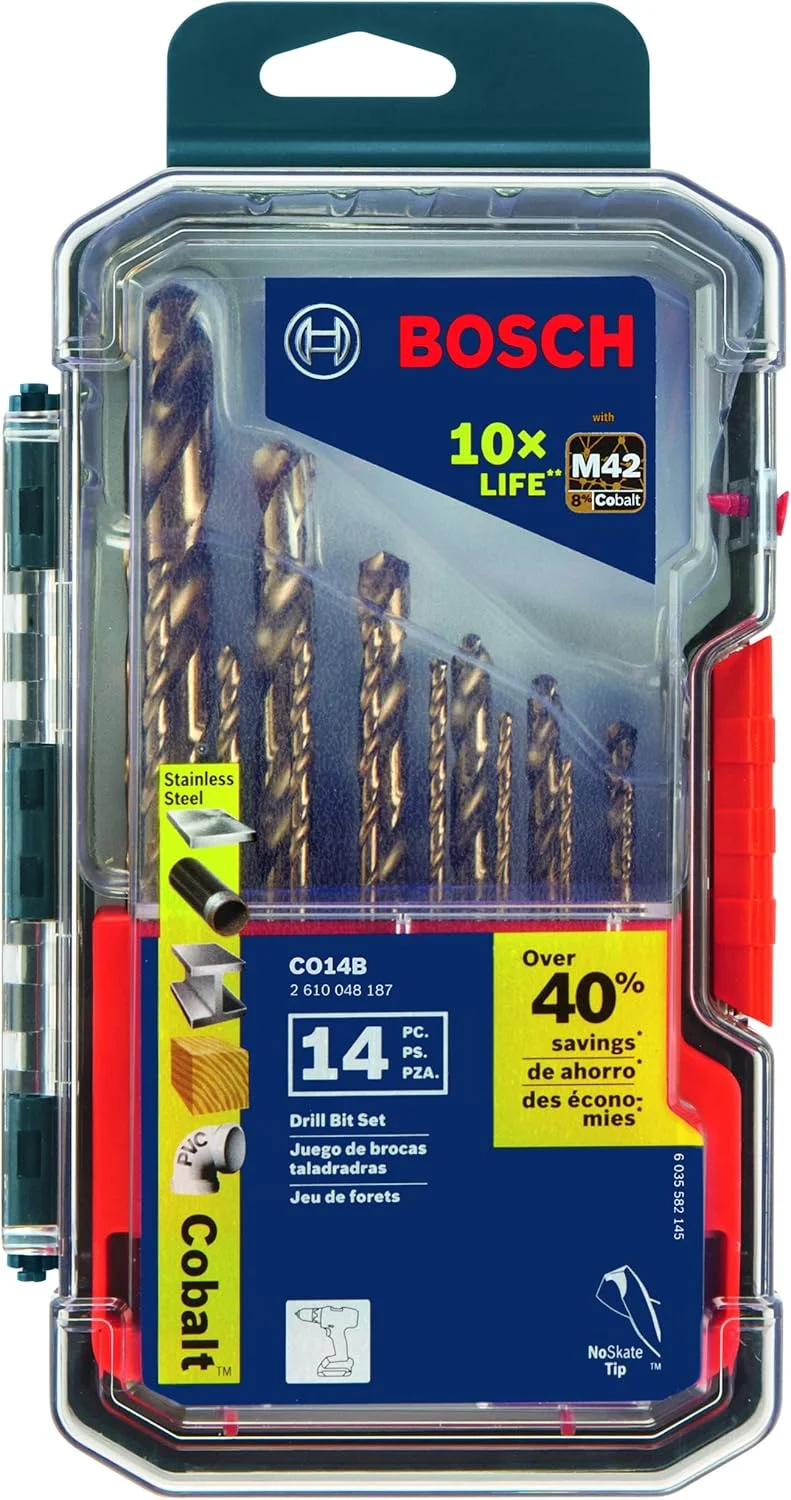
BOSCH CO14B 14-Piece Cobalt M42 Drill Bit Set
- M42 cobalt for stainless and hard alloys
- Three-flat shanks reduce chuck slip
- Split-point tips start on center
- Wide fractional coverage for fab work
- Heat tolerance above standard HSS
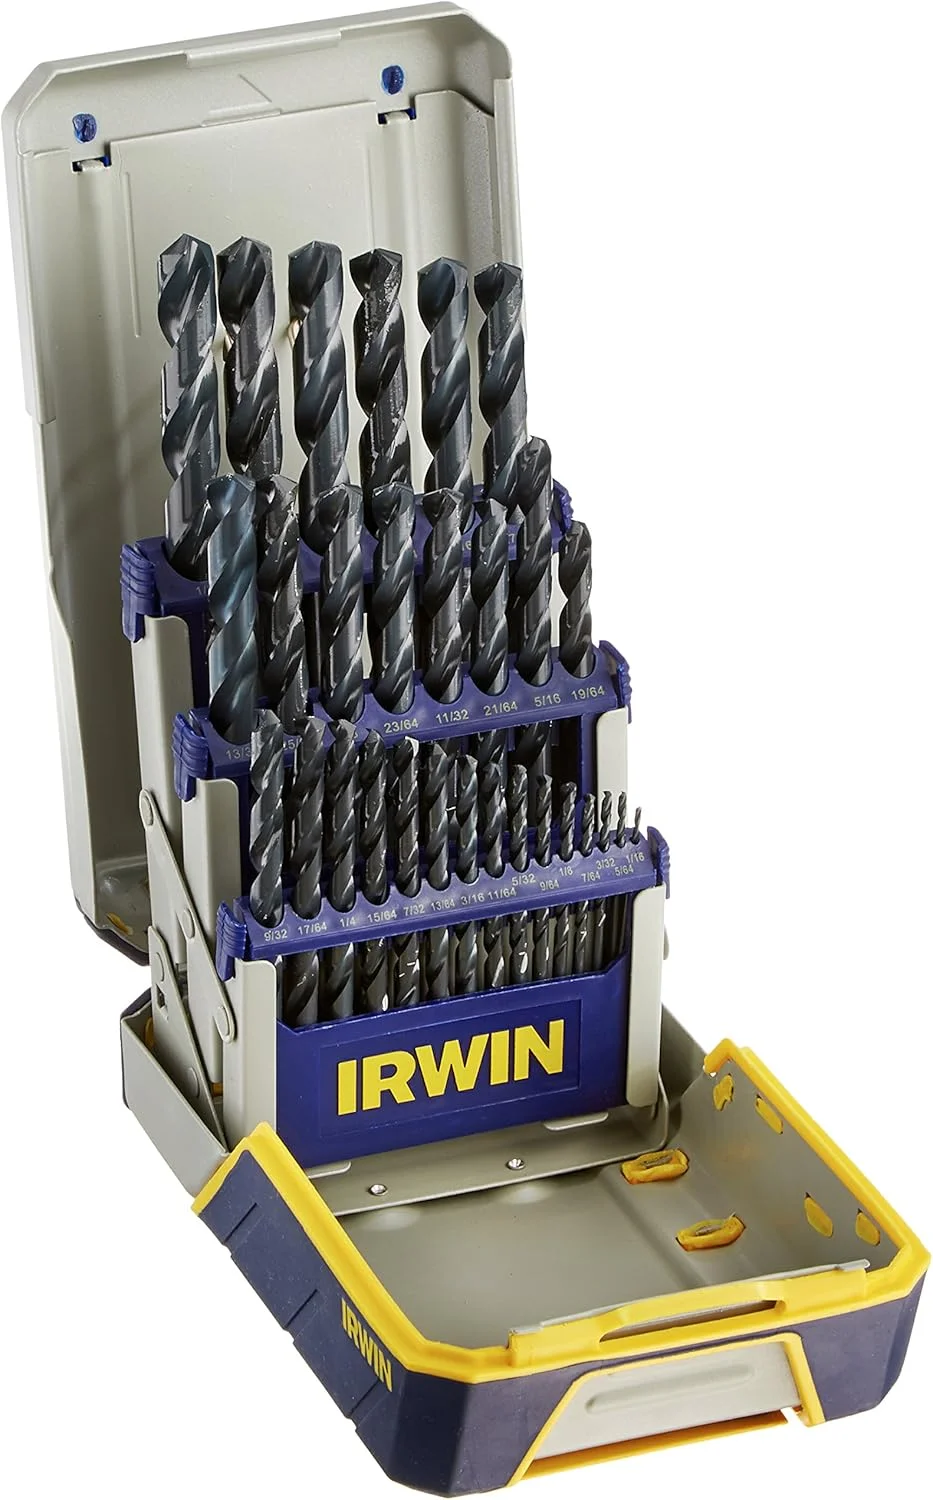
IRWIN 29-Piece Black Oxide Drill Bit Set
- Full fractional, number, and letter range
- Black oxide finish for mild steel
- Split-point geometry reduces walking
- Shop staple for everyday holes
- Strong value for general fabrication
Ironant Step Drill Bit Set
- Multiple diameters in one bit
- Ideal for sheet metal and thin plate
- Reduces bit changes on layout work
- Clean steps for burr-free holes
- Fast hole sizing in the shop
Neiko Transfer Punch Set
- Transfer hole locations accurately
- Match drill centers across plates
- Essential for layout and fit-up
- Hardened punches for repeat use
- Pairs with size conversion work

Tap Magic Cutting Fluid
- Reduces heat at the cutting edge
- Mandatory for stainless and tool steel
- Extends cobalt and HSS bit life
- Flushes chips from deep holes
- Shop standard for tough alloys
As an Amazon Associate, TestTalkHQ earns from qualifying purchases.
Letter Gauge Drill Bit Chart
Letter drills A through Z cover sizes just above the number series — from 0.2340 in (A) to 0.4130 in (Z).
| Letter | Decimal (in) | Metric (mm) | Nearest Fractional | Nearest Number |
|---|---|---|---|---|
| A | 0.2340 | 5.944 | 15/64 | — |
| B | 0.2380 | 6.045 | — | — |
| C | 0.2420 | 6.147 | — | — |
| D | 0.2460 | 6.248 | — | — |
| E | 0.2500 | 6.350 | 1/4 | — |
| F | 0.2570 | 6.528 | — | — |
| G | 0.2610 | 6.629 | — | — |
| H | 0.2660 | 6.756 | 17/64 | — |
| I | 0.2720 | 6.909 | — | — |
| J | 0.2770 | 7.036 | — | — |
| K | 0.2810 | 7.137 | 9/32 | — |
| L | 0.2900 | 7.366 | — | — |
| M | 0.2950 | 7.493 | 19/64 | — |
| N | 0.3020 | 7.671 | — | — |
| O | 0.3160 | 8.026 | — | — |
| P | 0.3230 | 8.204 | — | — |
| Q | 0.3320 | 8.433 | — | — |
| R | 0.3390 | 8.611 | — | — |
| S | 0.3480 | 8.839 | — | — |
| T | 0.3580 | 9.093 | 23/64 | — |
| U | 0.3680 | 9.347 | — | — |
| V | 0.3770 | 9.576 | 3/8 | — |
| W | 0.3860 | 9.804 | — | — |
| X | 0.3970 | 10.084 | — | — |
| Y | 0.4040 | 10.262 | 13/32 | — |
| Z | 0.4130 | 10.490 | — | — |
Metric Drill Bit Chart
Common metric diameters with inch equivalents and nearest imperial named bits. Use true metric bits when the print is in millimeters — do not force a fractional substitute on critical fits.
| Metric (mm) | Decimal (in) | Nearest Fractional | Nearest Number | Nearest Letter |
|---|---|---|---|---|
| 0.5 | 0.0197 | — | #76 | — |
| 0.6 | 0.0236 | — | #73 | — |
| 0.7 | 0.0276 | — | #70 | — |
| 0.8 | 0.0315 | 1/32 | #68 | — |
| 0.9 | 0.0354 | — | #65 | — |
| 1.0 | 0.0394 | — | #61 | — |
| 1.1 | 0.0433 | — | #57 | — |
| 1.2 | 0.0472 | 3/64 | #56 | — |
| 1.3 | 0.0512 | — | #55 | — |
| 1.4 | 0.0551 | — | #54 | — |
| 1.5 | 0.0591 | — | #53 | — |
| 1.6 | 0.0630 | 1/16 | #52 | — |
| 1.7 | 0.0669 | — | #51 | — |
| 1.8 | 0.0709 | — | #50 | — |
| 1.9 | 0.0748 | — | #48 | — |
| 2.0 | 0.0787 | 5/64 | #47 | — |
| 2.1 | 0.0827 | — | #45 | — |
| 2.2 | 0.0866 | — | #44 | — |
| 2.3 | 0.0906 | — | #43 | — |
| 2.4 | 0.0945 | 3/32 | #42 | — |
| 2.5 | 0.0984 | — | #40 | — |
| 2.6 | 0.1024 | — | #38 | — |
| 2.7 | 0.1063 | — | #36 | — |
| 2.8 | 0.1102 | 7/64 | #35 | — |
| 2.9 | 0.1142 | — | #33 | — |
| 3.0 | 0.1181 | — | #31 | — |
| 3.2 | 0.1260 | 1/8 | — | — |
| 3.3 | 0.1299 | — | #30 | — |
| 3.4 | 0.1339 | — | #29 | — |
| 3.5 | 0.1378 | — | #29 | — |
| 3.6 | 0.1417 | 9/64 | #28 | — |
| 3.7 | 0.1457 | — | #26 | — |
| 3.8 | 0.1496 | — | #25 | — |
| 3.9 | 0.1535 | — | #23 | — |
| 4.0 | 0.1575 | 5/32 | #22 | — |
| 4.2 | 0.1654 | — | #19 | — |
| 4.5 | 0.1772 | — | #16 | — |
| 4.8 | 0.1890 | 3/16 | #12 | — |
| 5.0 | 0.1969 | — | #9 | — |
| 5.2 | 0.2047 | 13/64 | #6 | — |
| 5.5 | 0.2165 | 7/32 | — | — |
| 5.8 | 0.2283 | — | #1 | — |
| 6.0 | 0.2362 | 15/64 | — | B |
| 6.5 | 0.2559 | — | — | F |
| 7.0 | 0.2756 | — | — | J |
| 7.5 | 0.2953 | 19/64 | — | M |
| 8.0 | 0.3150 | 5/16 | — | O |
| 8.5 | 0.3346 | — | — | — |
| 9.0 | 0.3543 | — | — | — |
| 9.5 | 0.3740 | 3/8 | — | — |
| 10.0 | 0.3937 | — | — | — |
| 10.5 | 0.4134 | — | — | Z |
| 11.0 | 0.4331 | — | — | — |
| 11.5 | 0.4528 | 29/64 | — | — |
| 12.0 | 0.4724 | — | — | — |
| 12.5 | 0.4921 | — | — | — |
| 13.0 | 0.5118 | — | — | — |
When Exact Size Matters
For clearance holes and general fab work, the nearest bit within a few thousandths is usually fine. For tap pilots, reamed holes, press fits, and dowel pins, use the exact decimal or named size. If your set is missing a number or letter bit, step to the next smaller size for taps (more thread engagement) rather than going oversize.
Related Calculators
Run the numbers, then come back here to pick the bit from your set: Tap Drill Size Calculator, Drill Speed Calculator, Drill Speeds by Material Chart, and Tap Drill Size Chart Guide.