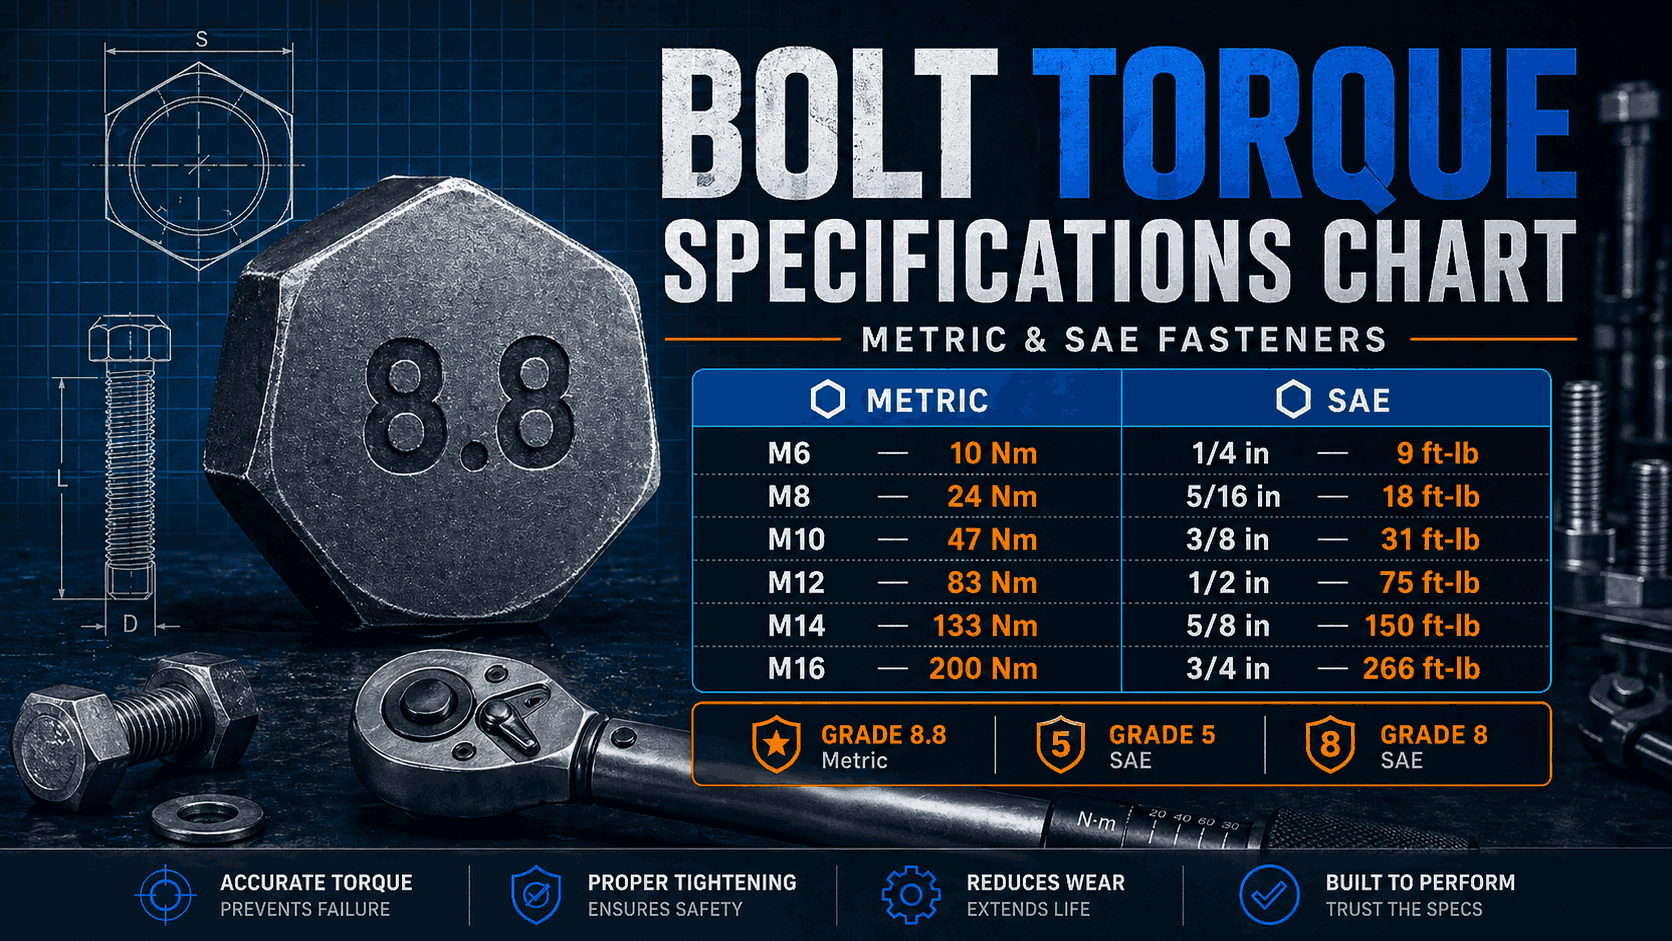
Need a fast shop answer? Match bolt size + grade/class + thread condition, then choose the dry or lubed torque row. Grade 8 / 10.9 can take more preload than Grade 5 / 8.8, and anti-seize can demand a real torque reduction. A single M10 Grade 8.8 bolt properly torqued to 22 Nm generates serious clamp load. Push torque ~30% too high and you can yield the bolt, lose preload over time, or snap it during install. This is why torque charts matter: right preload keeps joints tight under vibration; wrong preload causes leaks, loosening, or broken hardware. This guide provides complete torque specifications for metric ISO 898-1 and SAE fasteners, explains grade/class differences, and shows where calculation helps vs where proven chart values are the practical move. Use the Bolt Torque Calculator when you need a fast preload check. Quick field-reference rows. Use manufacturer/equipment spec first on safety-critical work. Lubed values are reduced from dry to account for lower friction. Values are pulled from the full tables below. For lubricated threads, a common field reduction is 20-30%, but always follow equipment/manual data when available. Need the numbers, not the lecture? Use the calculators below when you want torque, tap drill size, thread prep, or shop math without guessing. In machine work, most joints are repetitive and chart-driven. If a component manufacturer gives size/spec, use it. But for safety-critical, dynamic, vibration-heavy, or high-load joints, do the math and verify preload, thread condition, and tightening method. Torque specs are starting points. Final torque depends on material, thread condition, lubrication, bolt grade/class, washer use, joint design, and manufacturer specs. For safety-critical work, always follow the equipment/manual specification. These chart values are preserved from the original article and represent dry, standard assumptions unless noted. Practical tools for accurate tightening and thread prep As an Amazon Associate, TestTalkHQ earns from qualifying purchases. Metric classes (8.8, 10.9, 12.9) and SAE grades (2, 5, 8) are strength systems, not cosmetic labels. Correct class/grade selection is as important as torque number. Always verify actual spec from OEM or engineering standard for critical joints. Torque stretches the bolt like a spring; that tension clamps the joint. Most applied torque is lost to friction, which is why lube state changes preload so dramatically. Lower friction (oil/anti-seize) means more preload for same torque—reduce torque accordingly. Where T=torque, F=preload force, d=nominal diameter, K=nut factor. Original example preserved: M16x2.0, Grade 4.8, permanent joint, dry K=0.20. That aligns with common chart windows for this condition. Use size-specific Grade 8 table values (e.g. 1/2 in ~ 110 ft-lb dry), then adjust if lubricated per your spec. Lubrication lowers friction, so the same torque creates higher preload. Torque must usually be reduced. Common field reduction is roughly 20-30%, but use the lubricant or OEM guidance when available. They are broadly comparable high-strength classes, but not interchangeable without checking exact spec/application. Yes. Stainless fasteners are gall-prone and often installed with anti-seize at reduced torque values. Torque to the condition specified by the manual/spec and keep thread condition consistent across the joint. Common causes: wrong bolt grade, over-lubed threads with dry spec, damaged threads, or poor wrench calibration/range. Full symptom diagnosis: Bolt Torque Troubleshooting. No. Joint design, gasket/compression needs, lube state, washers, and material stack all change required preload. Use the chart for the right size and grade/class, match dry vs lubed condition, and apply torque with a calibrated wrench and proper sequence. That gets you reliable preload instead of broken bolts or loose joints. Also useful: Bolt Torque Troubleshooting · Torque Spec vs Torque-to-Yield · Metal Weight Calculator · Tap Drill Size Chart Guide · Angle Grinder Disc Speed Calculator Disclaimer: For critical applications, always follow manufacturer and engineering specifications. Price remodels and GC work, then send a quote with no internal numbers. Excel or Google Sheets. Best on a computer. $29.00 Checkout opens in a new tab.
Bolt Torque Quick Answer
Fastener Type
Common Grade/Class
Dry Torque
Lubed Torque
Notes
SAE hex bolt
Grade 5 (3 lines)
3/8 in = 30 ft-lb; 1/2 in = 75 ft-lb
~70-80% of dry
General machinery and automotive service
SAE hex bolt
Grade 8 (6 lines)
3/8 in = 44 ft-lb; 1/2 in = 110 ft-lb
~70-80% of dry
Higher preload and fatigue margin
Metric coarse
Class 8.8
M10 = 22 Nm; M12 = 38 Nm; M16 = 95 Nm
~0.75x dry typical
Common fab/shop baseline class
Metric coarse
Class 10.9
M10 = 32 Nm; M12 = 55 Nm; M16 = 140 Nm
~0.75x dry typical
Roughly Grade 8 territory in practice
Stainless bolt
A2/A4 class
Often not recommended dry
Use anti-seize + reduced torque
High galling risk if installed dry
When to Calculate Torque vs When to Use Thumb Rules
You must calculate when
Thumb rules are acceptable when
Critical warning
Complete Metric & SAE Torque Charts
Metric Grade 8.8 Torque Specifications
Bolt Size
Pitch (mm)
Torque (Nm)
Torque (ft-lb)
M6
1.0
4.5
3.3
M8
1.25
11
8.1
M10
1.5
22
16
M12
1.75
38
28
M14
2.0
61
45
M16
2.0
95
70
M20
2.5
190
140
M24
3.0
330
243
Metric Grade 10.9 Torque Specifications
Bolt Size
Pitch (mm)
Torque (Nm)
Torque (ft-lb)
M6
1.0
6.5
4.8
M8
1.25
16
12
M10
1.5
32
24
M12
1.75
55
41
M16
2.0
140
103
M20
2.5
280
207
SAE Grade 5 & Grade 8 Torque Specifications
Bolt Size
Grade 5 (ft-lb)
Grade 8 (ft-lb)
1/4 in
8
12
5/16 in
17
25
3/8 in
30
44
1/2 in
75
110
5/8 in
150
220
3/4 in
270
390
Dry vs lubricated adjustment
Thread Condition
Typical K factor
Typical torque adjustment
Dry unlubricated steel
0.20
Use published dry spec
Lightly oiled
0.15
~80-85% of dry
Anti-seize / well lubricated
0.12
~70-80% of dry
Stainless with anti-seize
~0.15
Reduced torque required
Recommended Torque Tools & Equipment
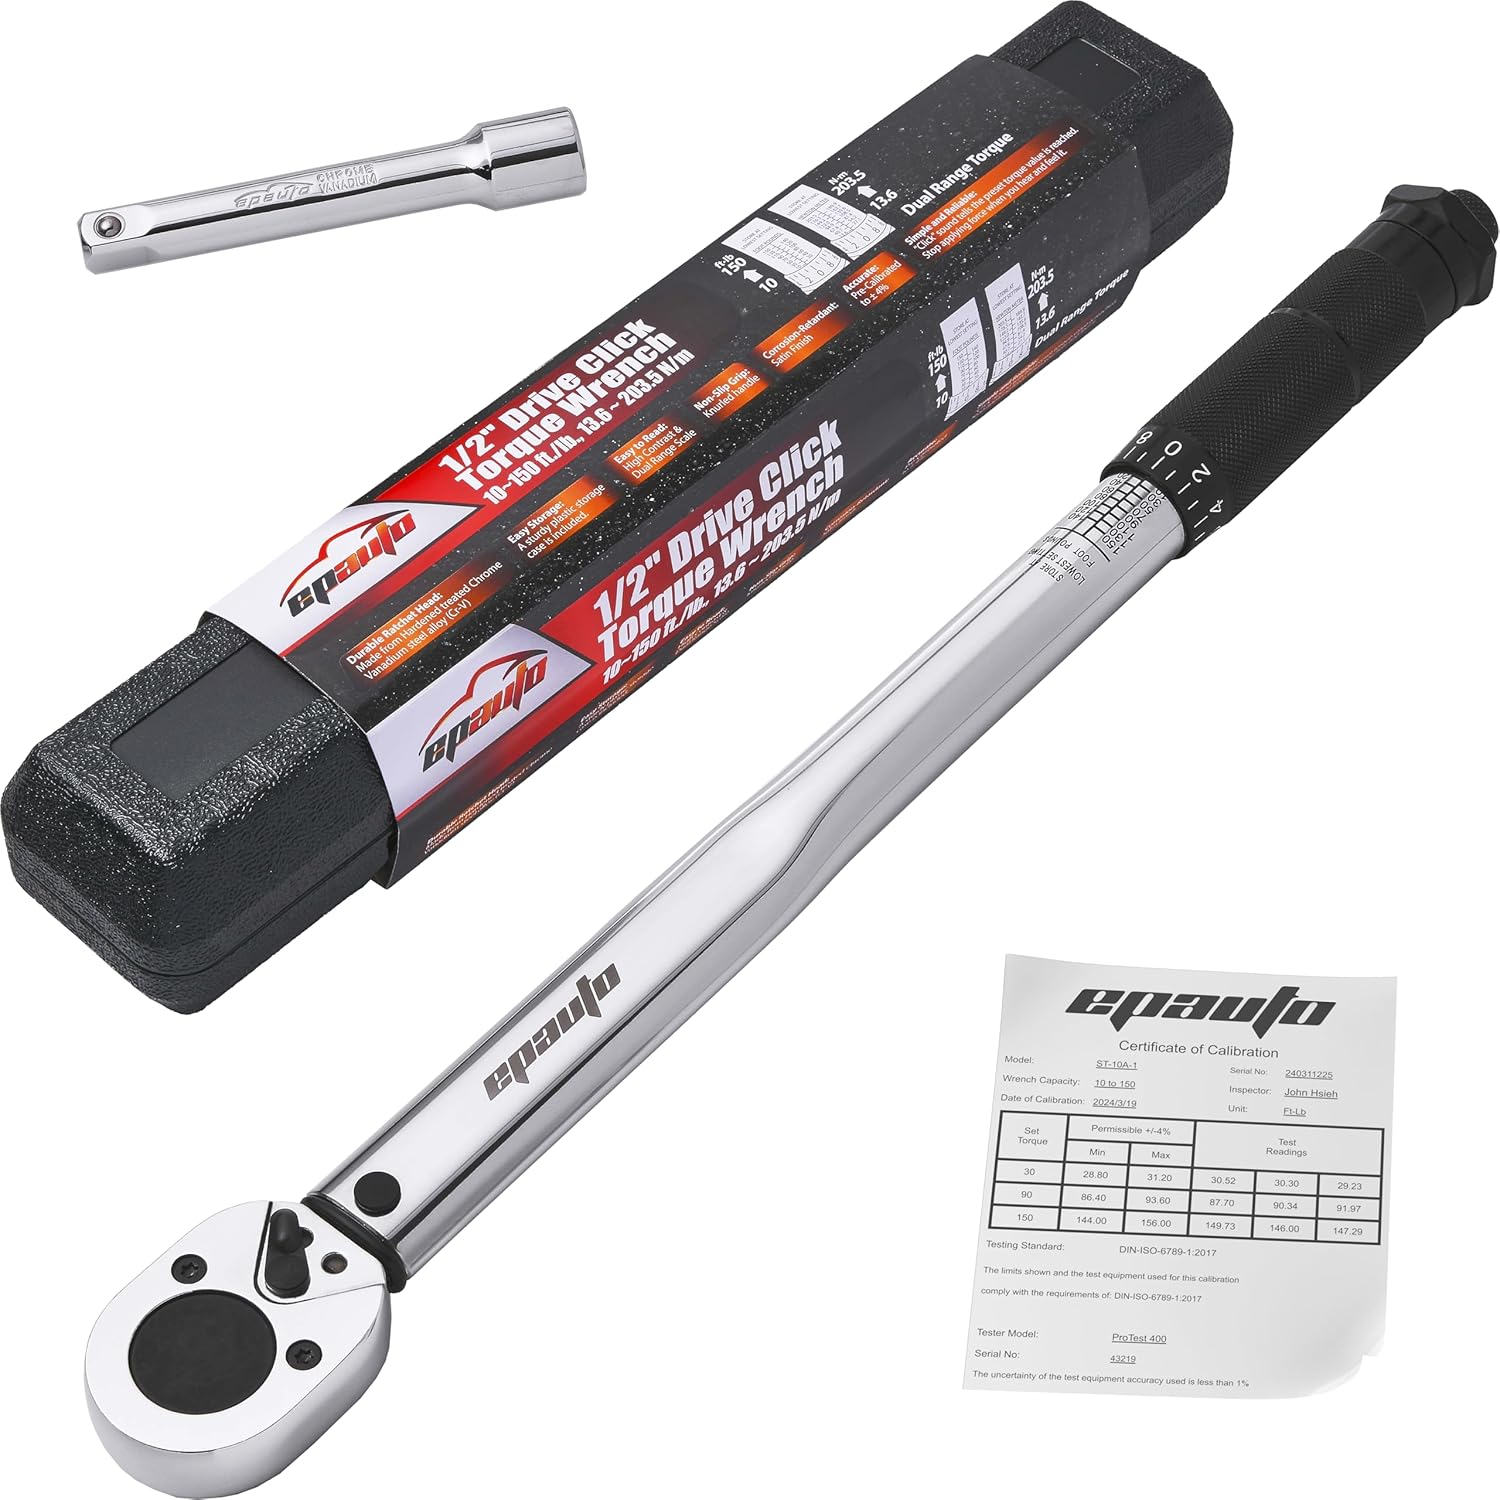
EPAuto 1/2 in Click Torque Wrench
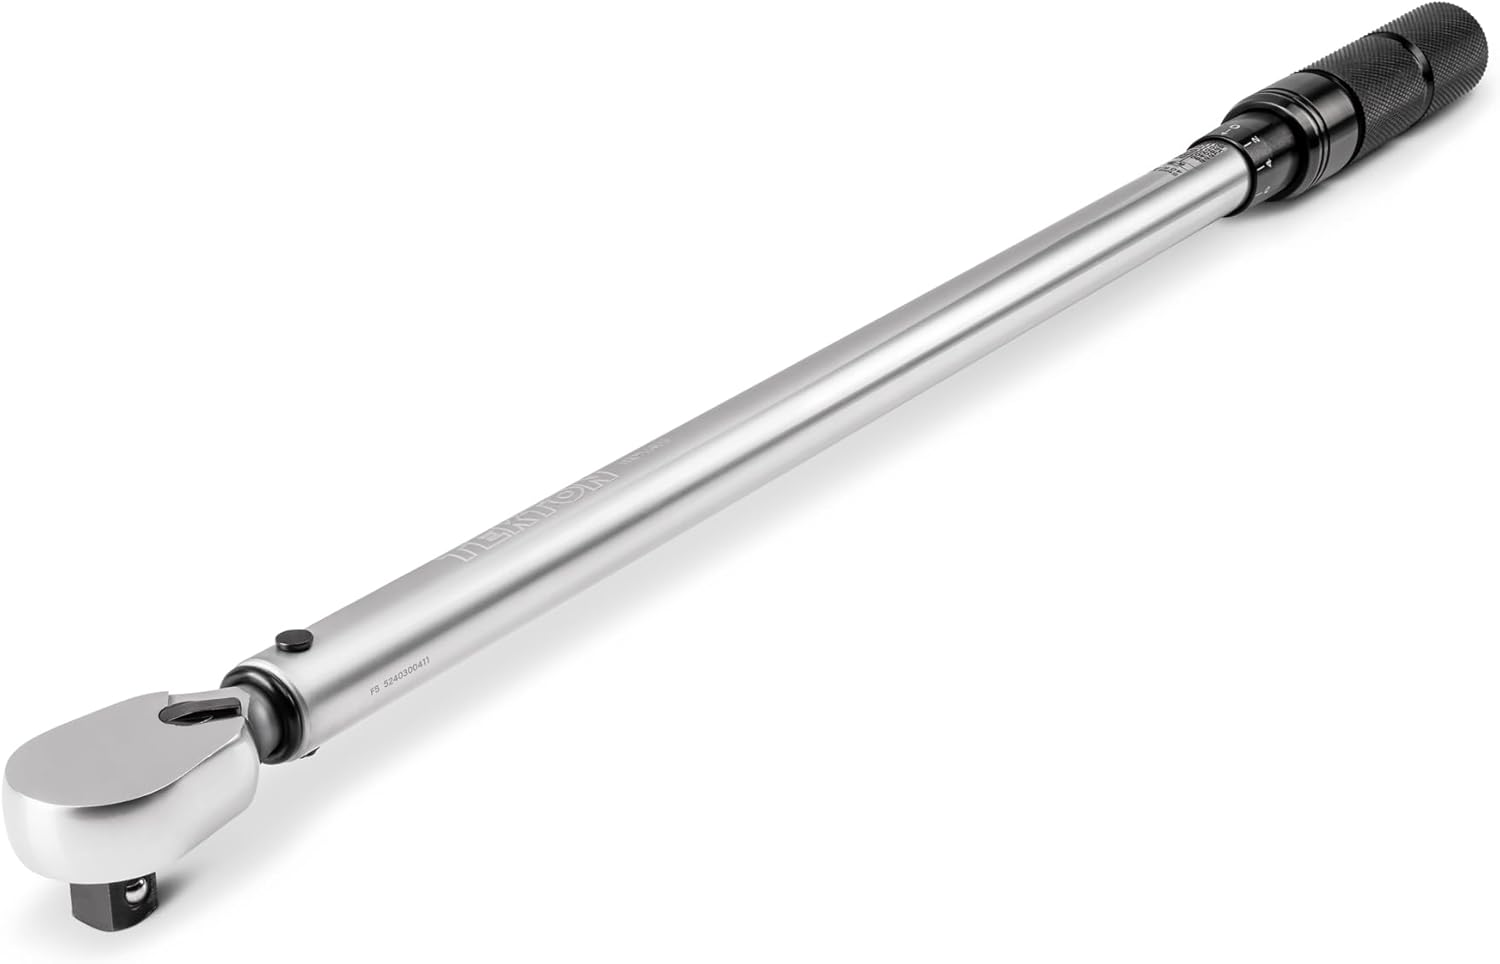
TEKTON 1/2 in Torque Wrench

CDI Pro 1/2 in Torque Wrench
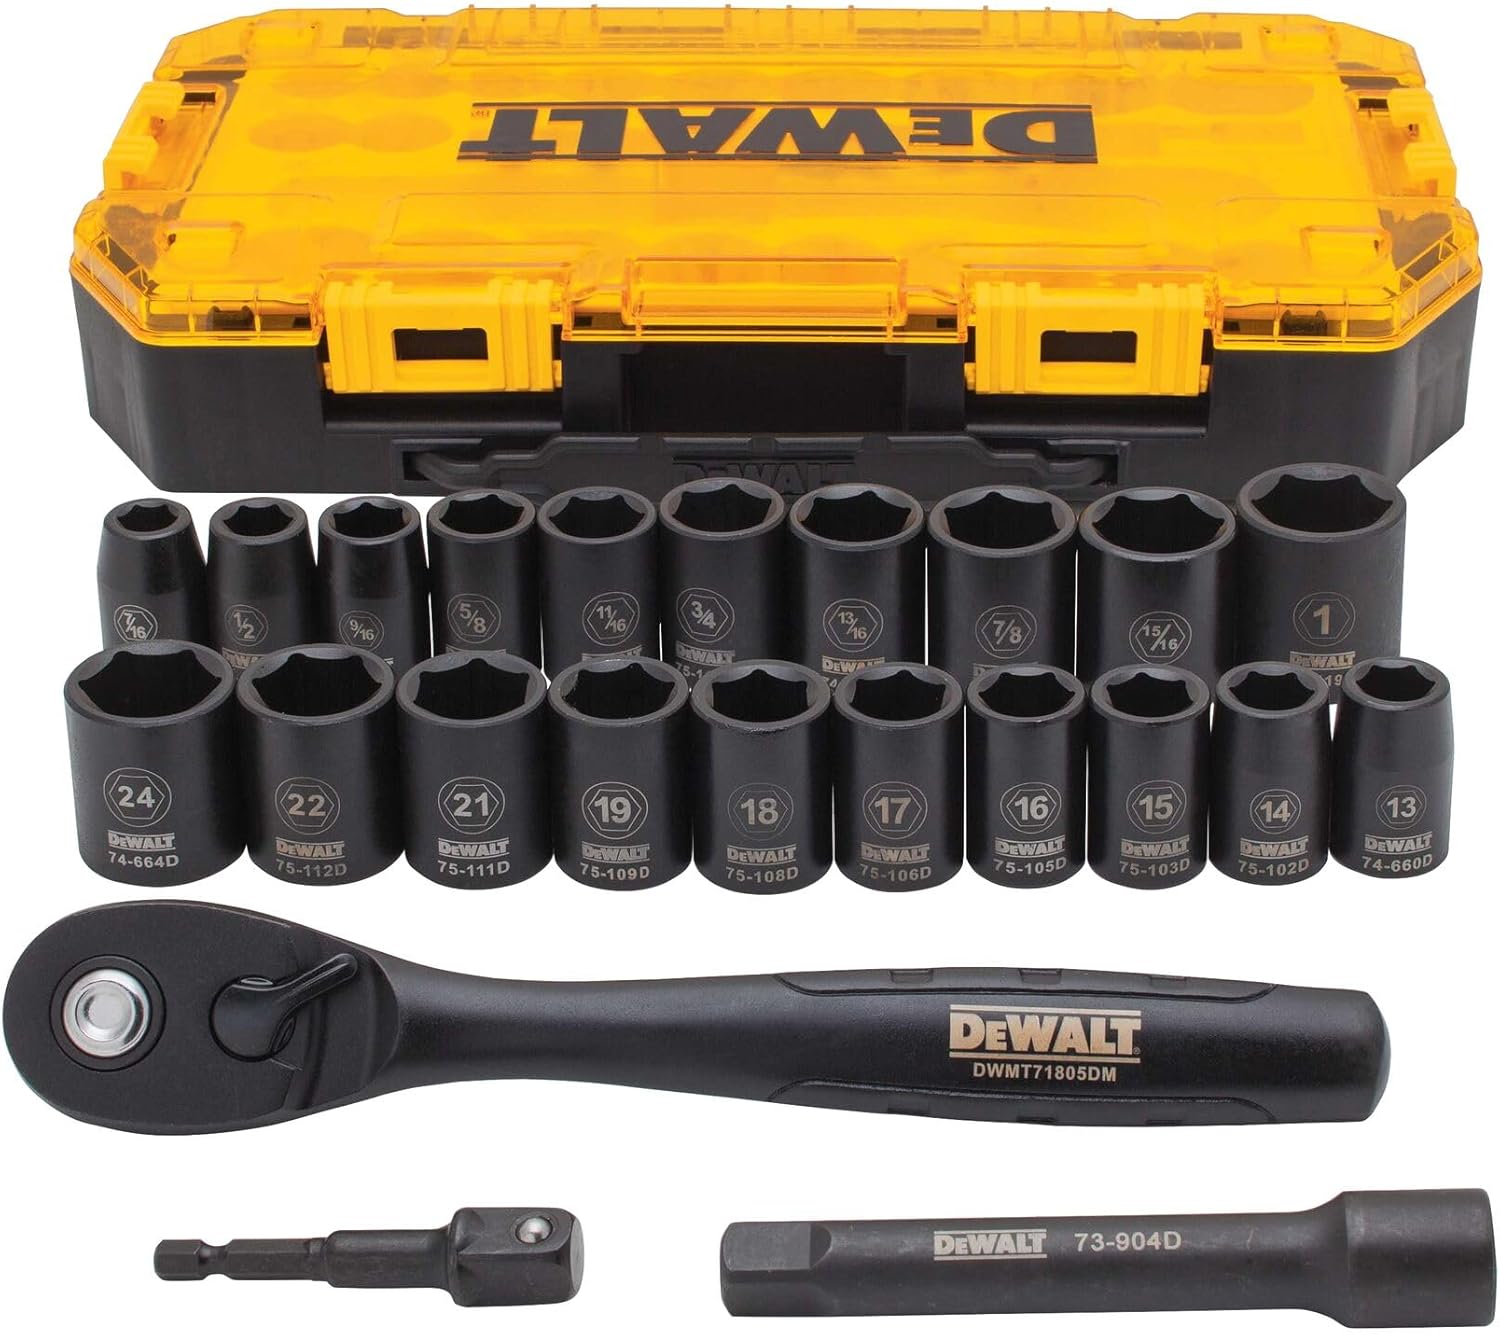
DEWALT 1/2 in Socket Set

Permatex Anti-Seize Lubricant
Understanding ISO 898 & SAE Bolt Grades
Quick class/grade map
How Bolt Torque Creates Clamping Force
The 10-50-40 reminder
Torque Calculation Formula Explained
Worked Example: M16 Grade 4.8 Calculation
Thread Engagement Rules
Material Pairing
Minimum engagement rule
Example
Steel into steel
1.0 × diameter
M10 -> ~10 mm engagement
Steel into aluminum/brass
1.5-2.0 × diameter
M10 -> ~15-20 mm
Steel into plastic
2.0-3.0 × diameter
M10 -> ~20-30 mm or inserts
Four Essential Bolt Sizing Thumb Rules
Critical Torque Mistakes to Avoid
Frequently Asked Questions
What torque should I use for a Grade 8 bolt?
What is the difference between dry and lubricated torque?
How much should I reduce torque when using anti-seize?
Is metric Class 10.9 the same as Grade 8?
Do stainless bolts need different torque?
Should I torque bolts dry or lubricated?
Why did my bolt snap before reaching torque?
Can I reuse torque specs for every application?
Conclusion: Torque Charts Are the Starting Point, Not the Whole Story
Any trade
Contractor Job Estimator
Bolt Torque Specifications Chart: Complete Guide for Metric & SAE Fasteners
Budget
Best Value
Premium
T = F × d × K
F = 0.75 × sigma_proof × A_stress (reusable joints)
A_stress = 0.7854 × (d – 0.9382 × p)^2