
Machining Speeds & Feeds Card
One page. Speeds, chip load and drill feed, imperial and metric.
$3.99
BuyDiagnose stick-out deflection, spindle RPM caps, flute-count mistakes, full-width slot overload, and climb crashes — when the calculator already “passed”
Not another SFM table and not a chip-load deep dive. Pair with the Milling Speed & Feed Calculator and Milling Speeds & Feeds Guide. IPT-specific failures: Chip Load Troubleshooting. Climb vs conventional: already covered. SFM/IPT tables live in the Milling Speeds & Feeds Guide (standalone chart merged there).

| Problem | Usually means | First fix |
|---|---|---|
| Walls taper / chatter on long tools | Stick-out deflection; RPM OK but rigidity not | Shorten stick-out; reduce DOC/WOC |
| Calculator RPM > spindle max | Small tool + high SFM; machine capped | Lower SFM or accept reduced surface speed |
| Flutes pack / screech in slot | Wrong flute count; full-width slot; chip evacuation | Fewer flutes Al; step-over; coolant/air |
| Manual mill climb crash | Backlash + climb with table pull | Conventional on worn knee mill |
| Breaks only in full-width slot | WOC = 100% while peripheral numbers used | Reduce AE; slot in passes |
What it looks like: Pocket walls lean; finish worse at the bottom; audible chatter on a long end mill even though the calculator RPM matched diameter and material.
Likely causes: Stick-out too long for DOC/WOC. Tool held in a flexible collet far from the spindle. Using finishing SFM on a roughing stick-out.
Fixes: Shorten projection; use a stub length mill; drop radial engagement before dropping RPM. Indicate runout with a dial indicator. Chip-load may be fine — rigidity is not an SFM problem (see chip-load troubleshooting only if IPT symptoms dominate).
What it looks like: 1/8" end mill in aluminum asks for 12,000+ RPM; Bridgeport tops out at 5,450. Operator runs max RPM and blames the chart when finish suffers.
Fixes: Accept reduced SFM on small tools; use sharper geometry; reduce chip load slightly for the lower surface speed; or move the job to a higher-speed spindle. Do not invent a fake diameter to “fix” RPM into range.
What it looks like: 4-flute packs in aluminum slots; 2-flute rubs in steel finishing; calculator used generic flutes field incorrectly.
Fixes: Re-enter actual flute count. Aluminum slots often want 2–3 flutes for evacuation. Steel finishing can use more flutes at lower IPT. Guide flute discussion: milling guide.
What it looks like: Peripheral side milling survived; first full-width slot snaps the mill. RPM matched the calculator.
Likely causes: Radial engagement (AE) = 100% of diameter while feed assumed light peripheral cut. Chip thickness changes with engagement — classic chip-load trap, but the milling-speed page is where operators start.
Fixes: Slot in multiple passes or reduce feed for full AE. Cross-check IPT math on Chip Load Calculator / troubleshooting.
What it looks like: Table jerks into the cut; bang; ruined cutter. Speeds were “right.”
Fixes: On worn backlash machines, prefer conventional milling. Decision content already lives on Climb vs Conventional Milling — do not re-litigate it here.
Choosing climb vs conventional?
Open Decision GuideClimb vs conventional is covered. SFM/IPR tables live on the Milling Speed & Feed Chart. This page stays on field diagnosis after the calculator numbers looked fine.
One page. Speeds, chip load and drill feed, imperial and metric.
$3.99
Buy
27 pages. Milling, drilling, tapping, turning and CNC routing.
$12.99
Buy
Quote shop work and check operations against your spindle's top speed.
Excel or Google Sheets. Best on a computer.
$29.00
Buy
Card, 27-page guide and the estimator workbook. All six files.
Excel or Google Sheets. Best on a computer.
$34.99
$45.98 if bought separately — save $10.99
BuyCheckout opens in a new tab.
Five CSV catalog picks — cut, measure, indicate, and finish holes after speeds/feeds are honest
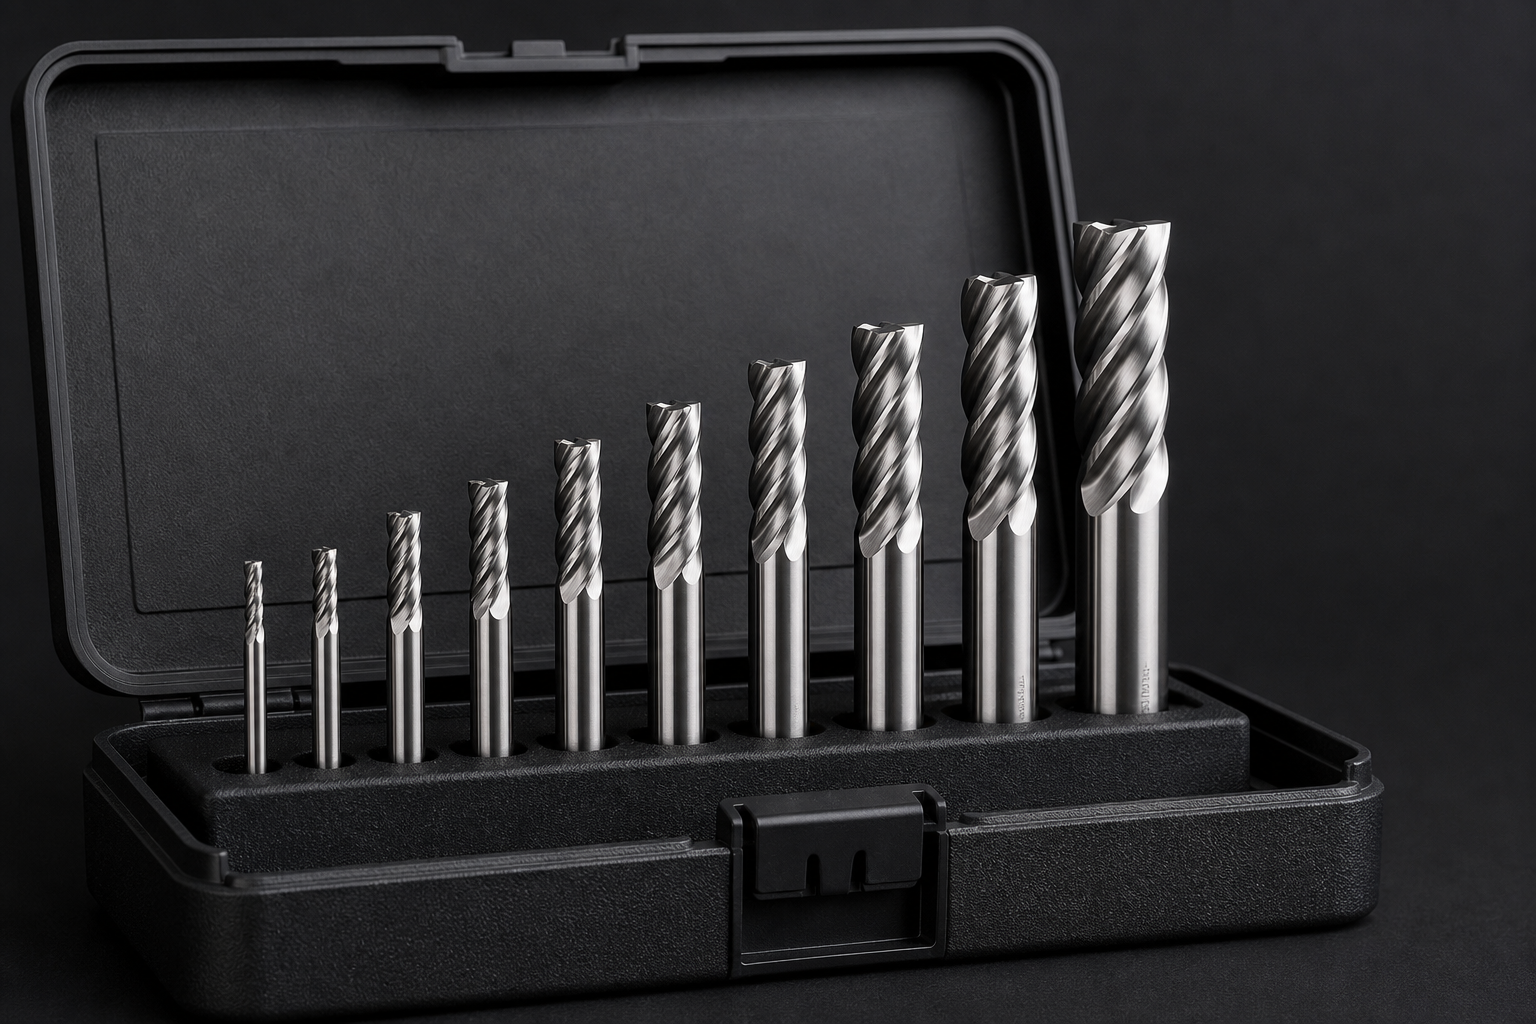

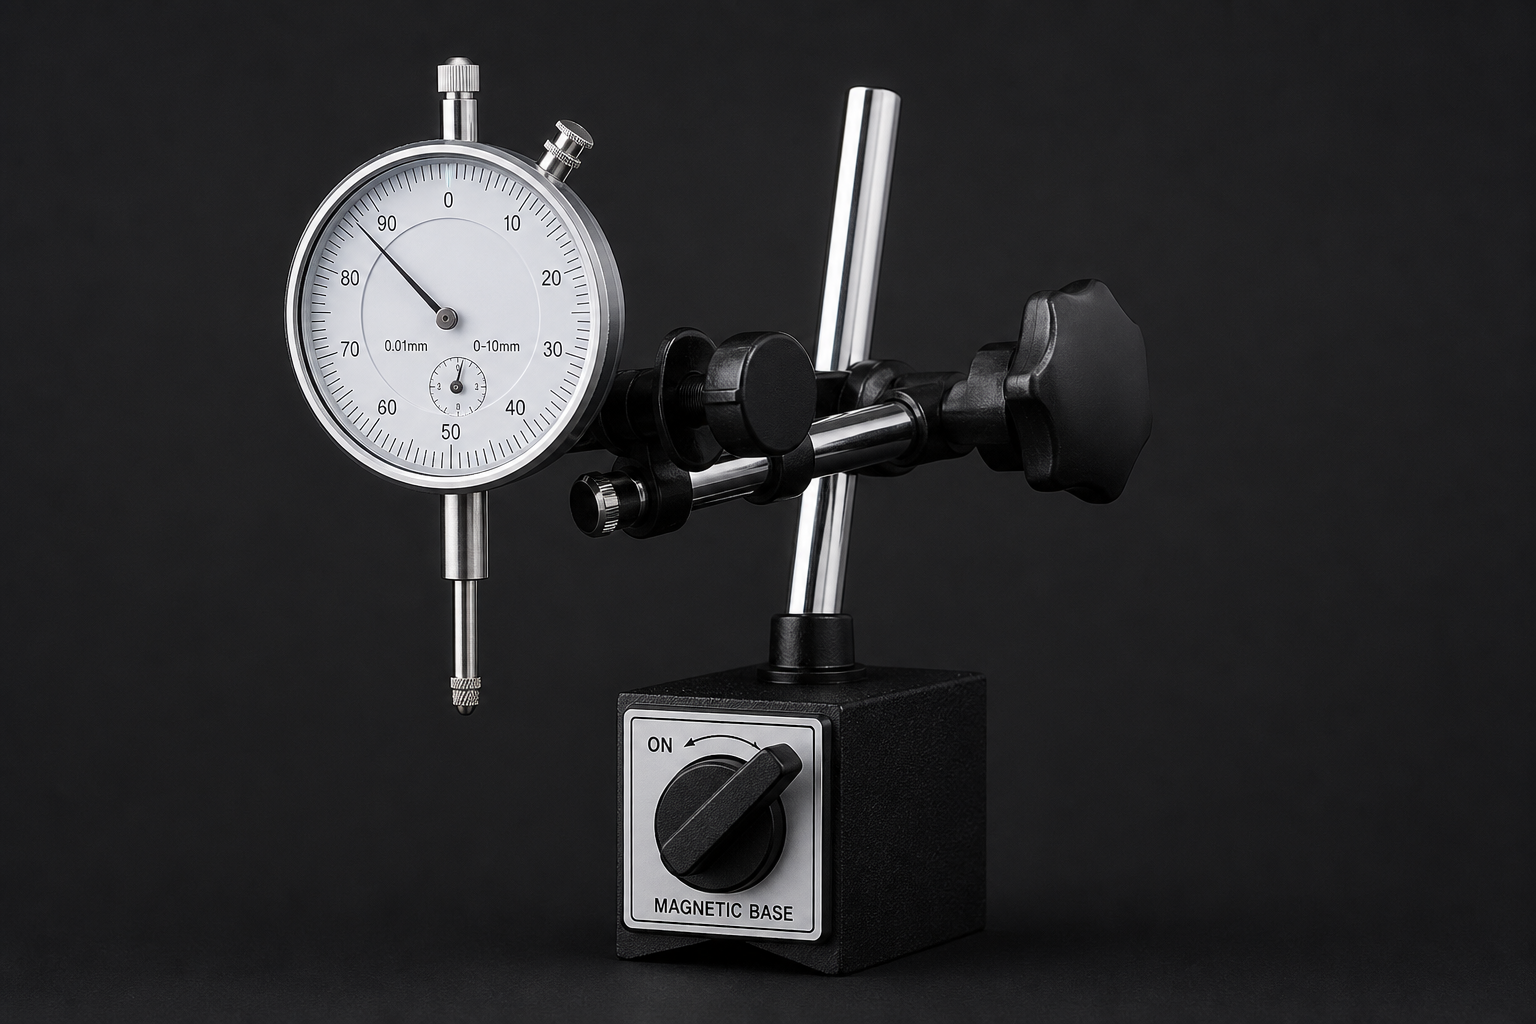
As an Amazon Associate, TestTalkHQ earns from qualifying purchases. All five cards sourced only from the affiliate CSV. Catalog gaps: stub-length end mills, collet chucks, edge finders (SHARS wiggler in CSV — image unavailable), coolant.
That page owns IPT/BUE/wear from chip thickness. This page owns milling setup failures after SFM/RPM looked right: stick-out, spindle caps, flute packing, full-width slots, climb crashes.
No — use the existing decision article.
No — use the existing milling speed/feed chart.
Reference only — prove cuts on scrap. WeldKit