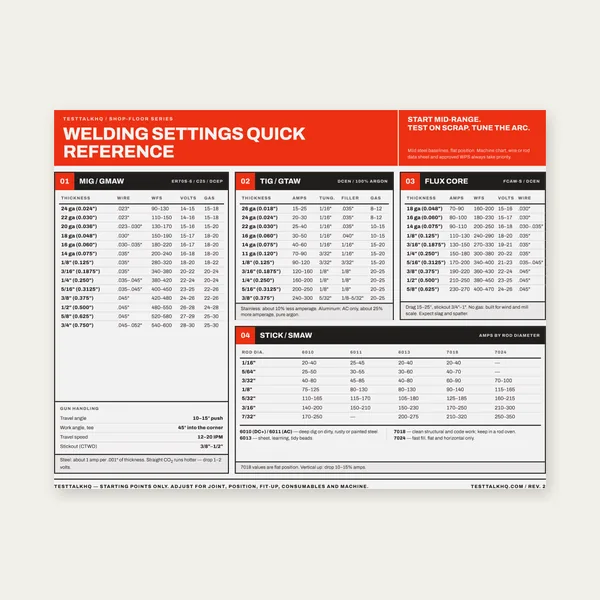
Welding Reference Card
One page. MIG, TIG, stick and flux core settings by thickness.
$3.99
BuyBurnback, birdnesting, inconsistent feed, and WFS-to-amperage mismatch on MIG/FCAW
Convert wire feed speed to welding amperage with the Wire Feed Speed to Amps Calculator. Browse welding tools on the Welding Hub.

Use this when the wire stubs, balls at the tip, nests in the drive, or the arc sounds wrong despite "correct" settings on the panel.
| Symptom | What it usually means | First fix | Next tool |
|---|---|---|---|
| Wire fuses to tip (burnback) | WFS too low or stick-out too long | Raise WFS or shorten stick-out | WFS to Amps Calculator |
| Stubbing / arc cuts out | WFS too high for voltage | Lower WFS or raise voltage | WFS to Amps Calculator |
| Birdnest at drive rolls | Tip blocked or liner kinked | Replace tip; check liner path | Welding Hub |
| Surging arc, uneven bead | Drive tension or liner wear | Tune roll tension; replace liner | WFS to Amps Calculator |
What it looks like: Wire welds itself to the contact tip (burnback), or the arc repeatedly extinguishes with a short stub (stubbing). Spatter balls on the tip.
Likely causes: Burnback: WFS too low for heat input, excessive stick-out, or pause at end of weld without crater fill. Stubbing: WFS too high for voltage — wire drives into the puddle faster than it melts.
Fixes: Balance WFS and voltage using the WFS to Amps Calculator; shorten stick-out; use crater fill/run-off tab. Match process to wire diameter and gas.
What it looks like: Wire bundles up at the drive rolls when the tip blocks; motor runs, wire doesn't advance. Often accompanied by a kinked liner or wrong tip size.
Likely causes: Blocked contact tip (spatter, burnback), liner too large/small for wire, sharp bend in torch cable, or drive tension too high crushing soft wire.
Fixes: Replace tip; trim liner; use correct roll groove; relieve cable bend radius. Lower tension until wire slips slightly under hand pull test, then tighten incrementally.
What it looks like: Arc surges and drops, bead width varies, WFS meter jumps if equipped. "Random" quality on long gun runs.
Likely causes: Worn liner, partial clog, drive rolls worn or wrong size, tension too low (slip) or too high (deformation). Cable overheated and liner swelled.
Fixes: Replace liner on schedule (wire pounds through liner); clean rolls; set tension per manufacturer. For aluminum, U-groove rolls and Teflon liner — standard steel setup causes slip.
What it looks like: Panel says 300 IPM but weld looks like 200 IPM heat; ammeter (if used) doesn't match calculator; different reels same setting feel different.
Likely causes: Slip not visible on meter; wire diameter wrong (0.035 setting on 0.030 wire); voltage drop in long leads affecting arc balance; metric/IPM display confusion.
Fixes: Enter actual wire size and WFS in the Wire Feed Speed to Amps Calculator; verify drive roll size matches wire; measure stick-out consistently.
Most feed problems are mechanical (liner, tip, tension) or WFS/V balance — use the calculator to confirm amperage matches intent.
One page. MIG, TIG, stick and flux core settings by thickness.
$3.99
Buy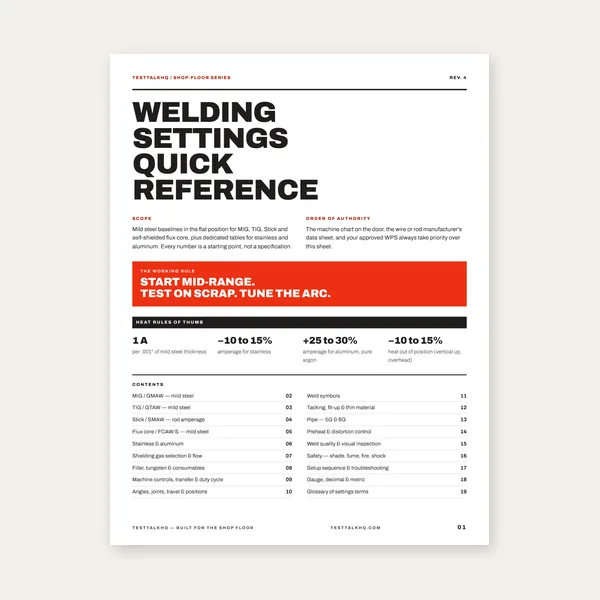
19 pages. Four processes, stainless and aluminum, symbols and inspection.
$12.99
Buy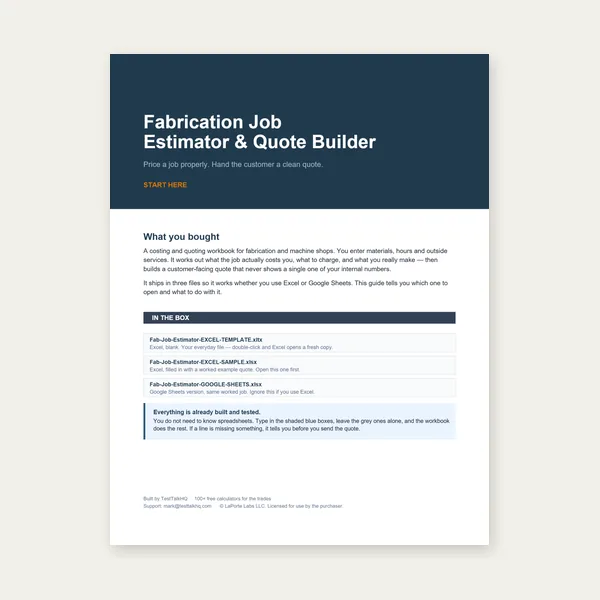
Price the job, then hand over a quote with no internal numbers.
Excel or Google Sheets. Best on a computer.
$29.00
Buy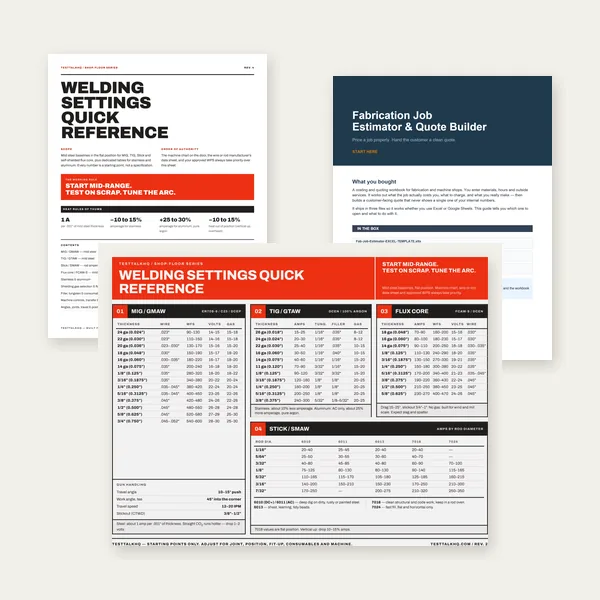
Card, 19-page guide and the estimator workbook. All six files.
Excel or Google Sheets. Best on a computer.
$34.99
$45.98 if bought separately — save $10.99
BuyCheckout opens in a new tab.
Five CSV catalog picks with verified images — flowmeters, regulators, torch accessories, and PPE
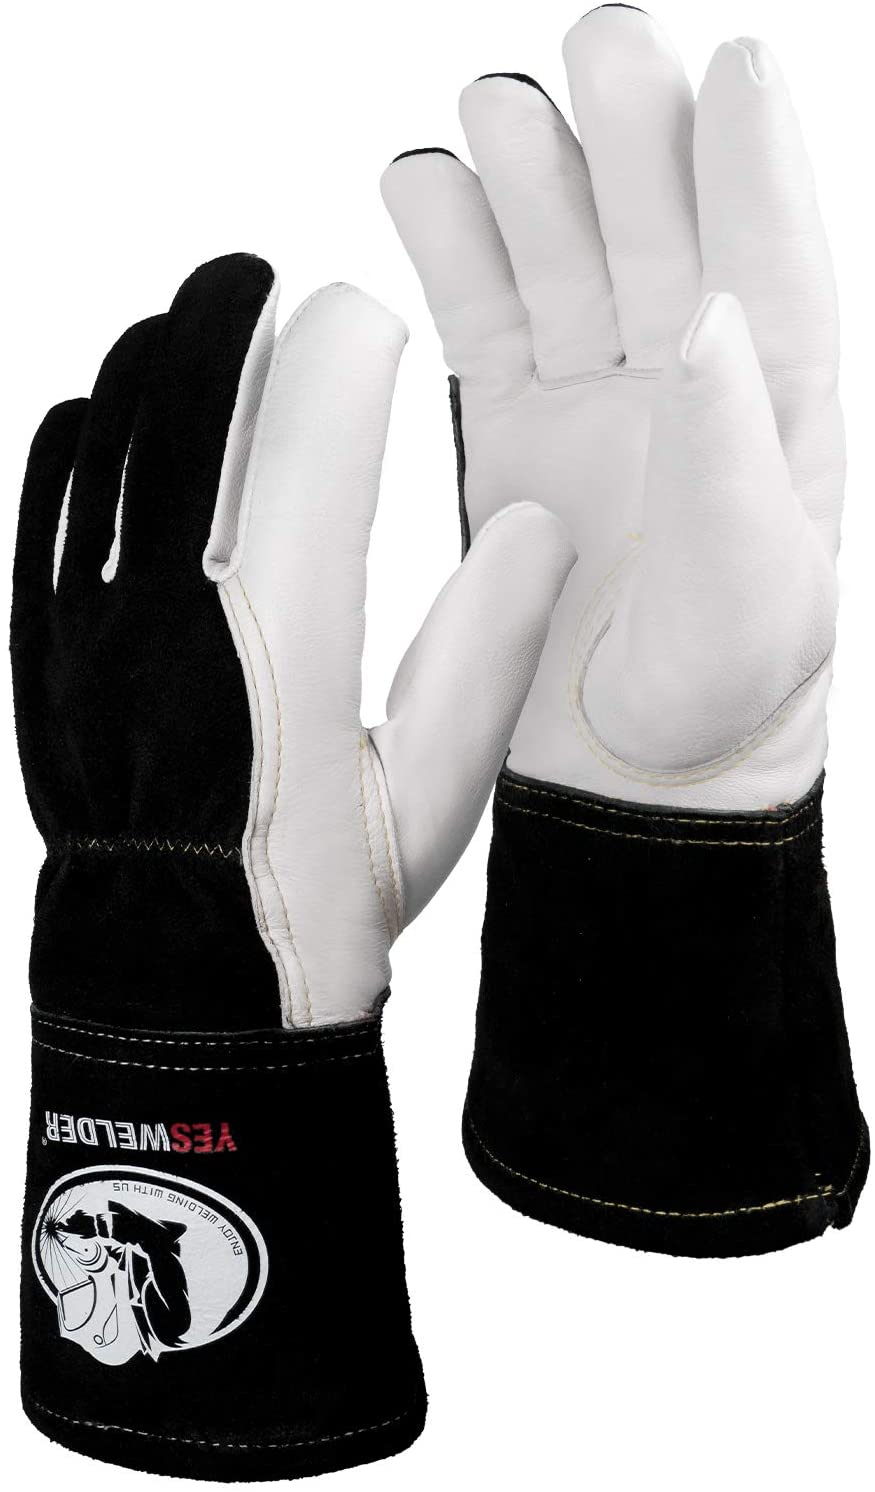
As an Amazon Associate, TestTalkHQ earns from qualifying purchases. All five cards are sourced only from the affiliate CSV with verified product images.
Burnback fuses wire to tip (often low WFS/long stick-out). Stubbing is wire jamming into cold puddle (often high WFS/low voltage).
Tip blocked — wire can't exit, motor keeps feeding. Clear tip/liner, don't just increase tension.
Tight enough to feed without slip; loose enough that wire doesn't deform — hand-pull slip test.
Yes — same IPM on wrong diameter gives wrong amperage. Match rolls, tip, and calculator input.