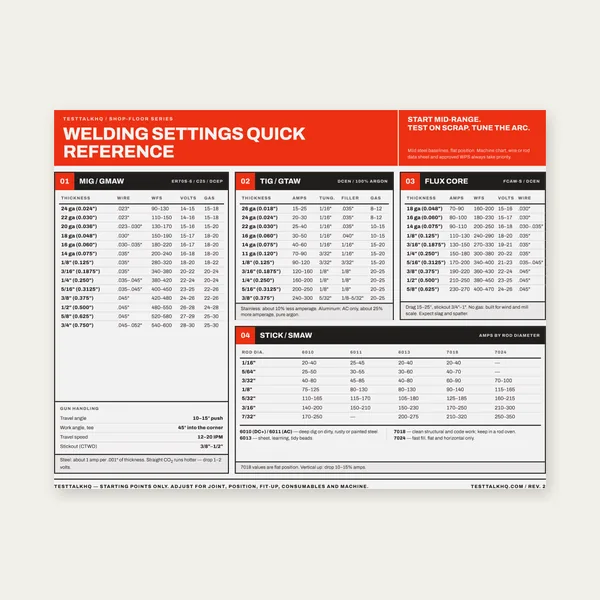
Welding Reference Card
One page. MIG, TIG, stick and flux core settings by thickness.
$3.99
BuyDiagnose early thermal shutdowns, hot-shop derates, cord sag, dirty vents, amp confusion, and multi-pass heat — when the calculator already “passed”
Not another definition of duty cycle. Pair this with the Duty Cycle Calculator when weld/cool math looks right and the machine still trips. For what 20% / 60% / 100% means when buying, use the Duty Cycle Explained Guide. This page stays on diagnosis.

Use this when calculated weld time is green but the thermal LED hits early, the machine runs hotter than the plate suggests, amps were confused across ratings, multi-pass work piles heat, or shop reality does not match the NEMA test sticker.
| Problem | What it usually means | First fix | Next tool |
|---|---|---|---|
| Shuts down before calculated weld time | Shop hotter than 104°F rating; voltage sag raising real current; blocked airflow | Derate for ambient; shorten/upsize cord; clear vents | Duty Cycle Calculator |
| Hotter / trips more often at “rated” duty | Extension-cord drop; dirty filters/fans; machine against a wall | Fix input voltage; blow out intakes; give clearance | Welding Cable Size Calc |
| Confused by % at different amps | Treating duty as one fixed number instead of % @ amps | Read the plate at the amps you actually run | Duty Cycle Guide |
| Multi-pass job outruns cool-down math | Cumulative heat across passes; calculator assumes a fresh cold start each cycle | Add rest between passes; lower amps; sequence fit-up into cool windows | Duty Cycle Calculator |
| Spec sheet ≠ shop performance | NEMA 40°C / clean power / open air vs hot garage + long cord | Treat plate as best-case; derate 20–40% in hostile shops | Extension Cord V-Drop |
What it looks like: Calculator says 6 minutes weld at 60% of a 10-minute cycle; thermal trip at 3–4 minutes. Same sticker, same dial amps.
Likely causes: Ambient above the 104°F / 40°C NEMA test point — summer garages and closed trailers derate hard. Voltage sag so the inverter draws more internal current to hold the set output. Poor ventilation — machine boxed in, intakes against a wall, no fan clearance.
Fixes: Derate weld time 20–40% when the shop is hotter than the rating room. Measure plug voltage while welding; if it sags, shorten or upsize the extension cord (or eliminate it). Pull the machine into open air; never block rear fans. Leave the power on during cool-down so the fan runs.
What it looks like: You stay inside calculated weld time but the machine still feels hotter each cycle, trips more often as the day goes on, or fans scream constantly.
Likely causes: Extension-cord voltage drop forcing higher input current for the same arc. Dirty intake filters, packed heat sinks, or metal dust on fans. Undersized welding leads adding heat and machine stress at the same set amps — see Welding Cable Size Calculator.
Fixes: Use a short, heavy cord (or none). Blow out intakes and filters on a schedule — especially flux-core and grinding shops. Size power leads for peak welding amps, not average duty. If voltage at the plug sags under load, that is an input problem, not a “bad duty cycle.”
Suspect cord sag? Long thin extension cords are a classic reason “correct” duty still trips early.
Extension Cord V-Drop CalcWhat it looks like: Operator treats “60% duty cycle” as a single machine constant, then welds at higher amps than the rating line and wonders why the calculator’s 6-minute window fails.
Likely causes: Duty cycle scales with amperage. A machine might be 60% @ 180A and ~100% @ 90–120A. The calculator only knows the % you typed — if you type 60% while welding at a higher amp than the plate’s 60% line, the math is for the wrong condition.
Fixes: Read the nameplate (or manual table) at the amps on your dial. Re-run the Duty Cycle Calculator with that pair. Lower amps often buys more continuous time without buying a new machine.
What it looks like: First pass fits the weld/cool math; by pass 4–6 the machine trips mid-bead even though each individual arc-on time was “within limits.”
Likely causes: Simple duty-cycle calc assumes a cold start each 10-minute window. Multi-pass work leaves residual heat in the inverter, torch, and workpiece. Fit-up pauses that are shorter than the required cool window never fully reset the thermal mass.
Fixes: Treat cool-down as mandatory between heavy passes, not optional. Sequence grinding, clamp changes, and inspection into cool windows. Drop amps on fill passes when possible. On long seams, plan stitch or back-step patterns that create natural rest. Water-cooled torches help TIG heat at the torch — they do not erase machine duty limits.
What it looks like: Marketing and NEMA sticker promise X%; your shop never sees that window at the same dial setting.
Likely causes: Manufacturer tests use controlled ambient, clean power, open airflow, and the exact amp line on the plate. Real shops add heat, dust, long cords, generators, and higher duty from continuous fit-up. IEC 5-minute vs NEMA 10-minute ratings also confuse cross-brand comparisons.
Fixes: Treat the sticker as best-case. Derate for your worst day (hot + long cord). Compare brands only when cycle period (5 vs 10 min) and amp lines match. Use the calculator to plan work rhythm — then verify with a scrap run in your actual environment before promising production rates.
Hobby and light fab often thrive on 20–35% machines; prosumer shops want ~60%; production wants near-100%. That buying fork already lives in the complete guide — use it before upgrading hardware for “more duty.”
One page. MIG, TIG, stick and flux core settings by thickness.
$3.99
Buy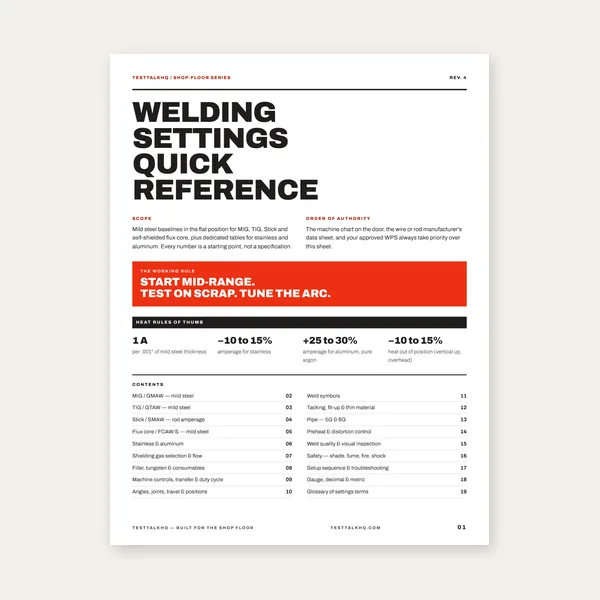
19 pages. Four processes, stainless and aluminum, symbols and inspection.
$12.99
Buy
Price the job, then hand over a quote with no internal numbers.
Excel or Google Sheets. Best on a computer.
$29.00
Buy
Card, 19-page guide and the estimator workbook. All six files.
Excel or Google Sheets. Best on a computer.
$34.99
$45.98 if bought separately — save $10.99
BuyCheckout opens in a new tab.
Five CSV catalog picks — machines with different real-world duty envelopes plus helmet gear for productive cool-down windows
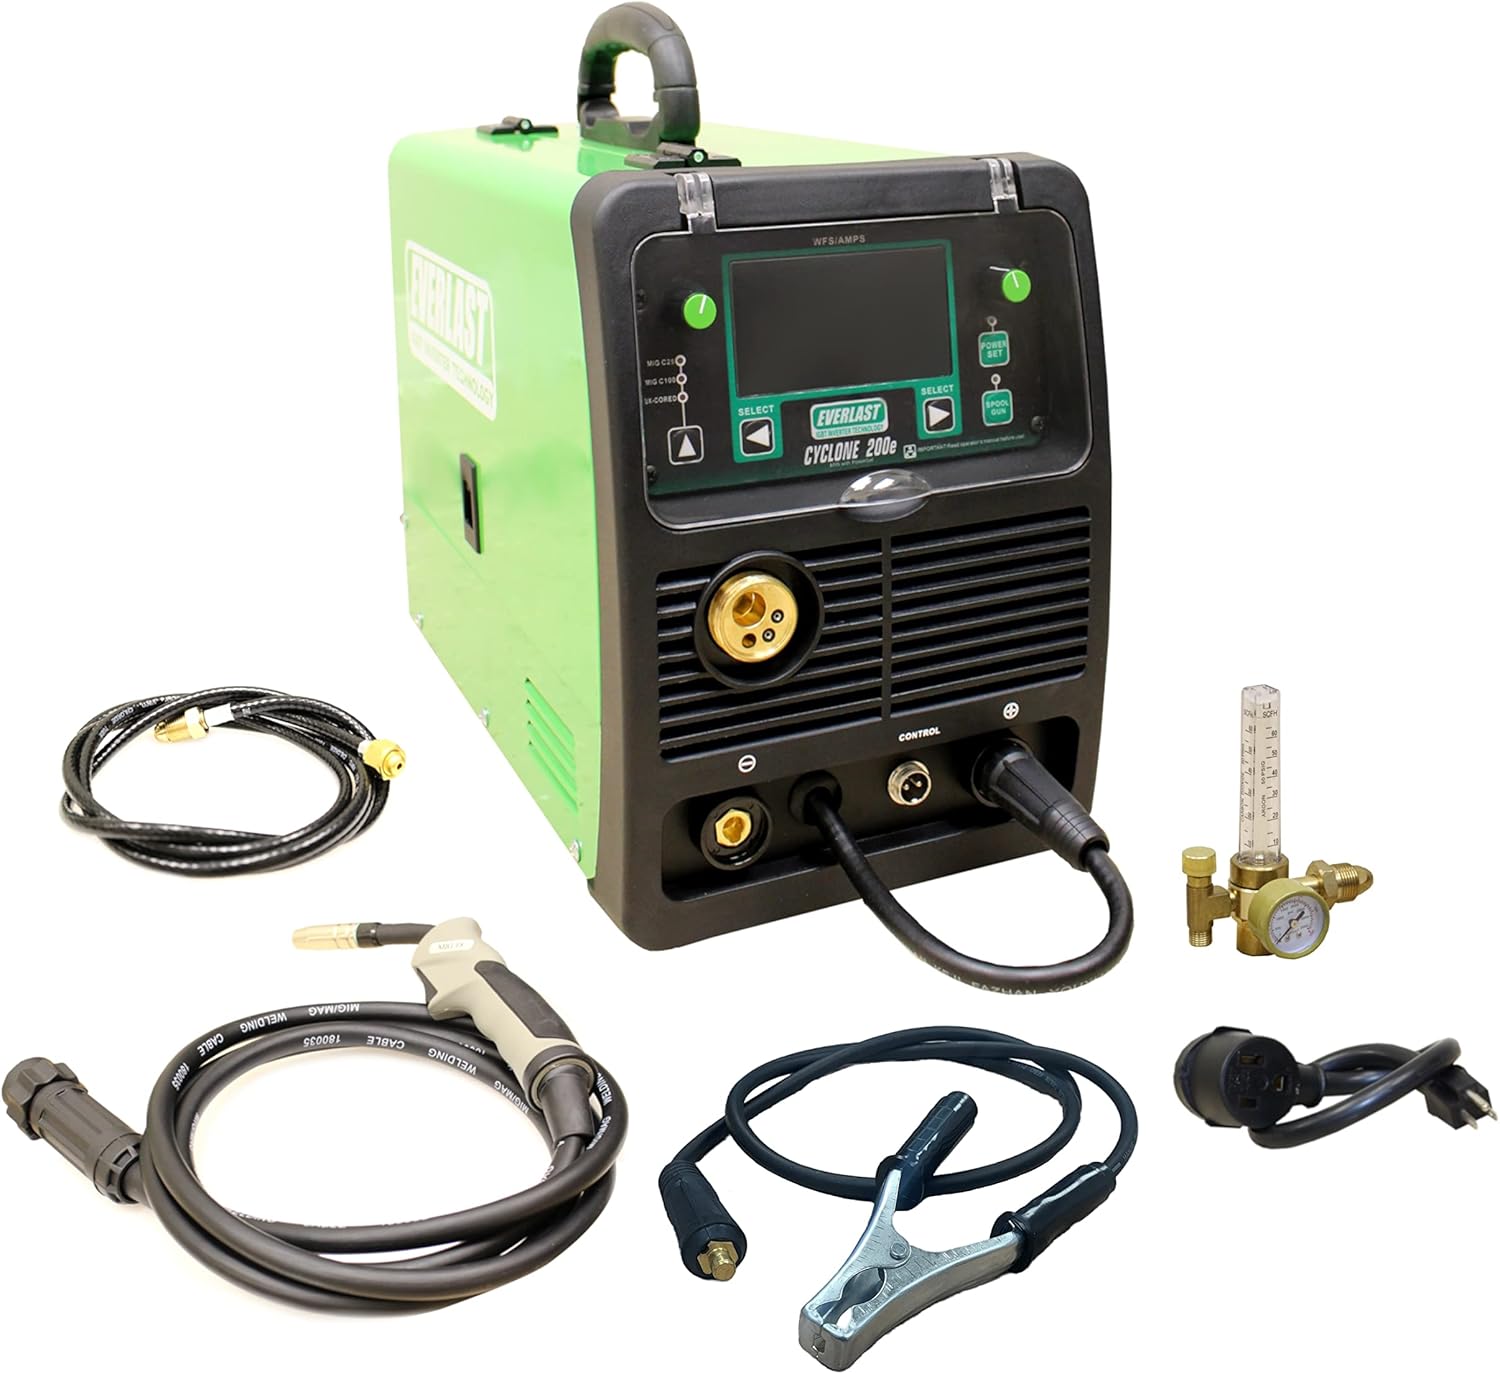
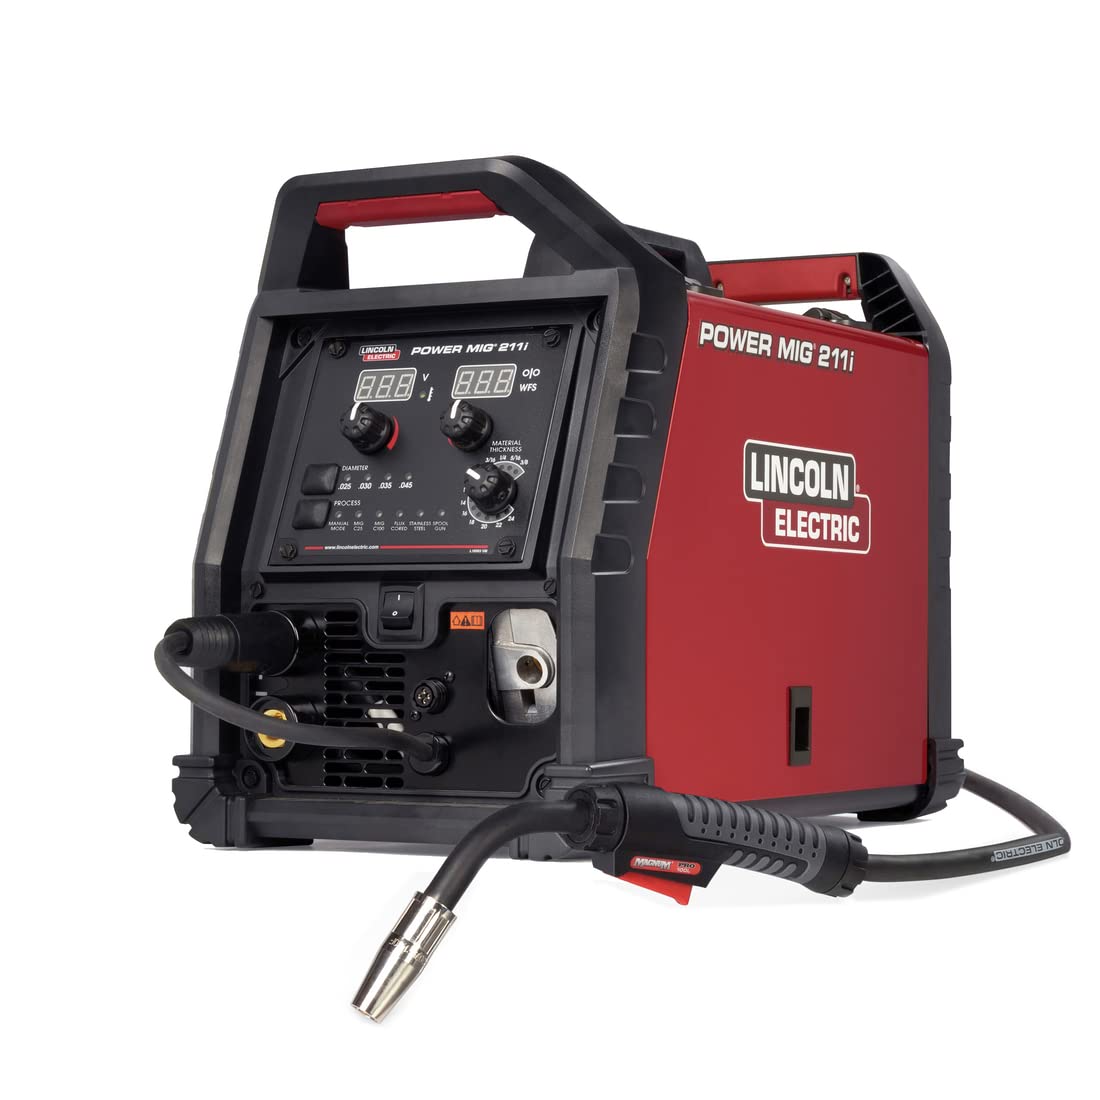
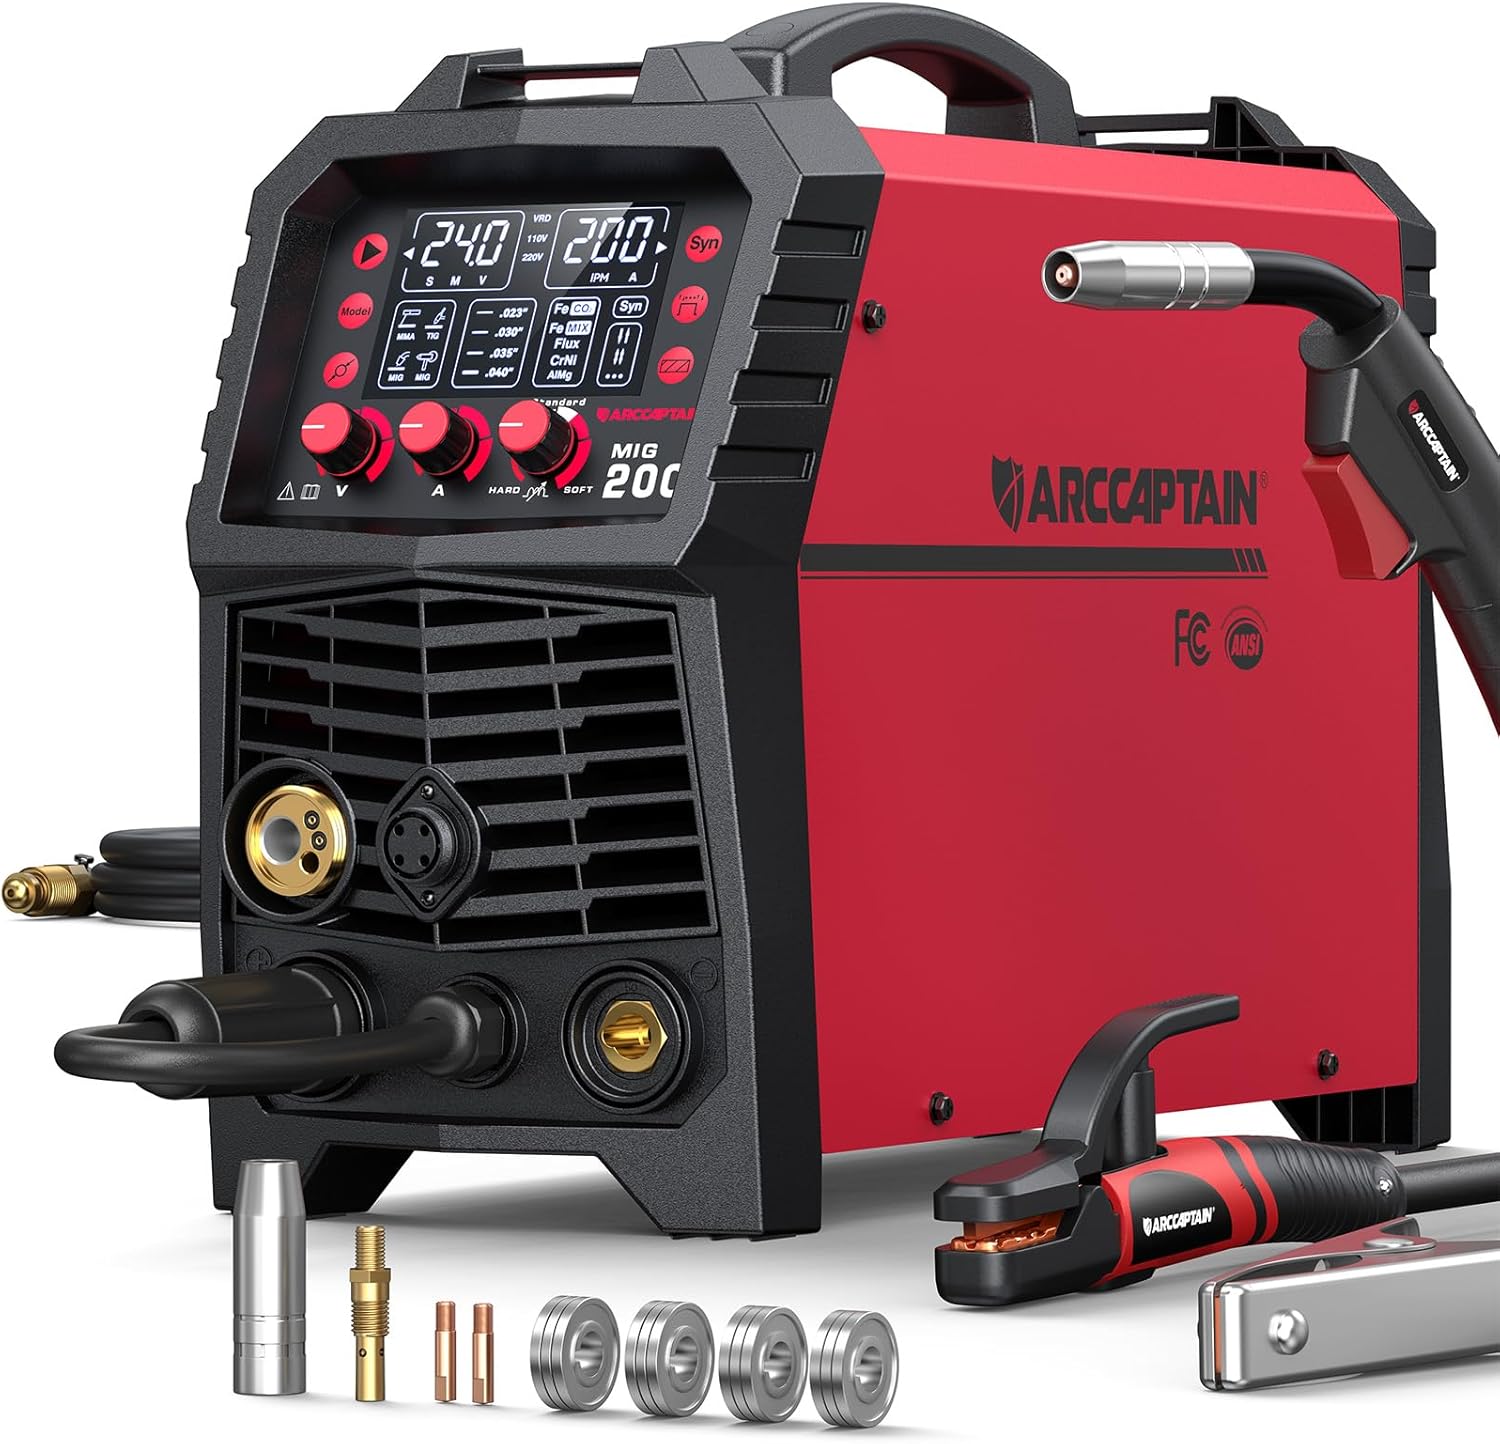
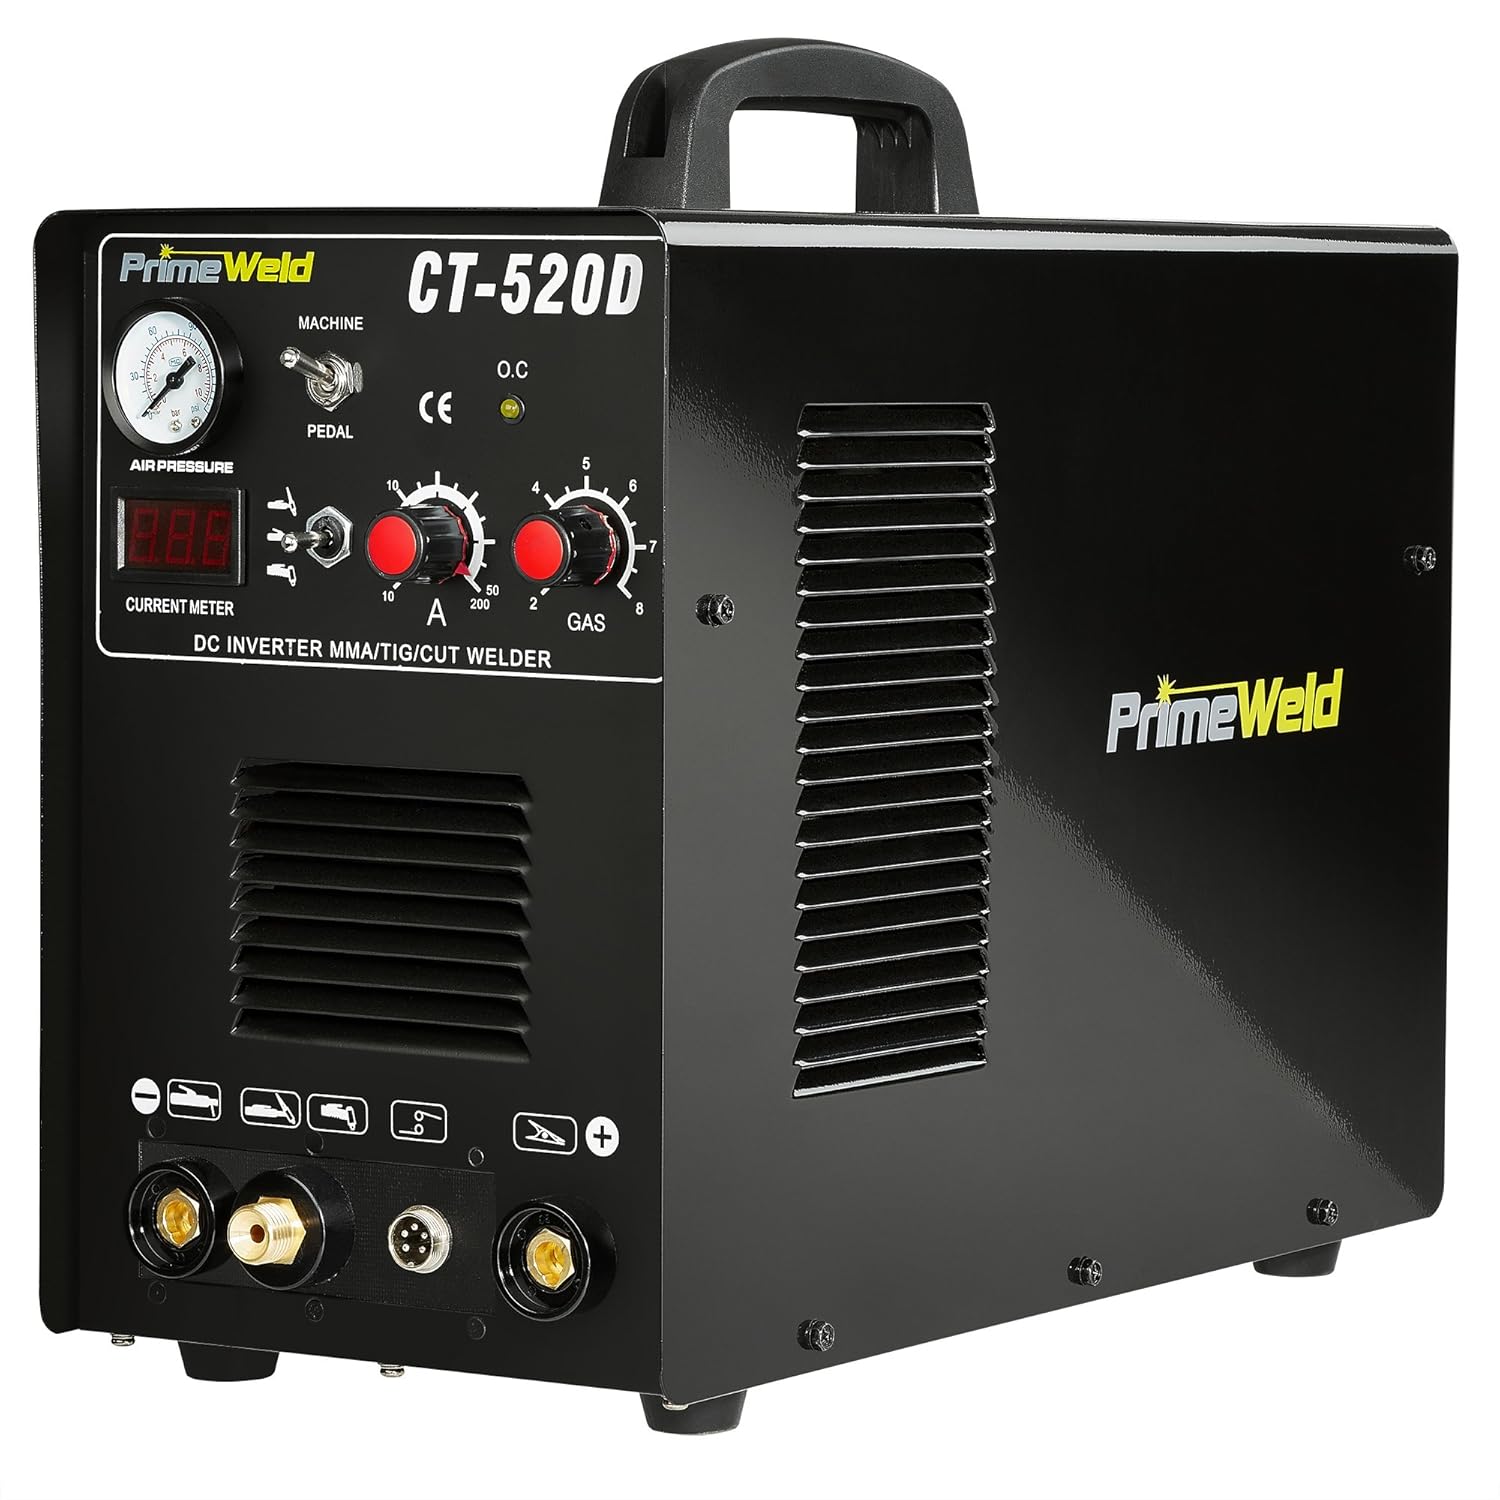
As an Amazon Associate, TestTalkHQ earns from qualifying purchases. All five cards are sourced only from the affiliate CSV (Welding Machines / Welding / Fab).
Ambient heat, cord sag, blocked vents, wrong amp line, or stacked multi-pass heat. The calculator trusts the % you entered; it cannot see your shop.
Yes — the fan needs power. Killing the breaker right after a trip often slows cooling.
Only for a 10-minute NEMA cycle at the amp line that 60% is rated for. Different amps or a 5-minute IEC cycle change the window.
It can restore the machine’s intended input voltage so internal current (and heat) drop. It does not rewrite the nameplate — it removes a common fake “duty” failure.
No. The guide teaches definitions, 20/60/100% buying classes, and amp relationships. This page diagnoses failures when the calculation already looks correct.