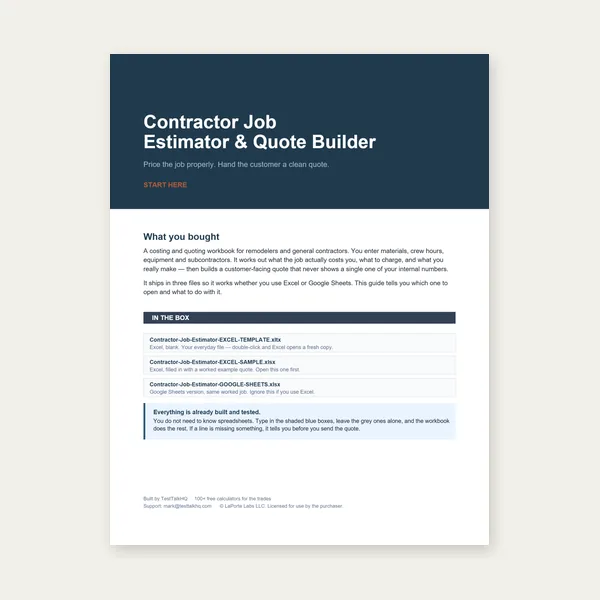
Contractor Job Estimator
Price remodels and GC work, then send a quote with no internal numbers.
Excel or Google Sheets. Best on a computer.
$29.00
BuyPrinter scaling · height vs slant · throat closure · seam shortfall
Diagnose templates that won’t roll true, mixed-up height inputs, lobster-back throat closure, and blanks that come up short without seam allowance.

Most “won’t roll true” failures are printer scaling — measure the reference square before blaming the math.
Open the Generator →Likely cause: The PDF was scaled by the printer (“Fit to page” / “Shrink to fit”). The reference square on page 1 must measure exactly 1 in or 50 mm. If it doesn’t, every radius and arc is wrong. Re-print at 100% / Actual Size, verify the square, then cut.
Vertical height is the standing height of the cone/frustum. Slant height is the distance along the side from apex (or between ends on a frustum). Entering one when you meant the other changes L and θ and the blank will be the wrong size even though the preview “looks fine.” Check which toggle is active under “Specify by,” and open Show the math to confirm.
If centerline bend radius is too close to the pipe radius, the inside (throat) of the elbow collapses toward zero width. Increase CLR (long-radius elbows are often ~1.5× diameter) or reduce segment angle / change gore count. The tool requires bend radius > pipe radius so the throat stays open.
The exported pattern is finished surface only. If you cut on the line and then try to lock-seam or lap without extra stock, the joined circumference comes up short. Add allowance before cutting — see seam allowance by joining method.
Development is taken at one surface. On thick plate, decide whether diameters are ID, OD, or mean, and expect a neutral-axis correction the flat pattern does not apply. Dry-fit and adjust before final weld — same discipline as the Tube Notch Troubleshooting guide for thick-wall tube.
Walk through each mode in the Cone / Transition Flat-Pattern Guide. For related sheet work, see the Sheet Metal Bending Guide and Sheet Metal Gauge Chart.
Price remodels and GC work, then send a quote with no internal numbers.
Excel or Google Sheets. Best on a computer.
$29.00
BuyCheckout opens in a new tab.
Cut the developed pattern, then form and join — products from the TestTalkHQ affiliate catalog
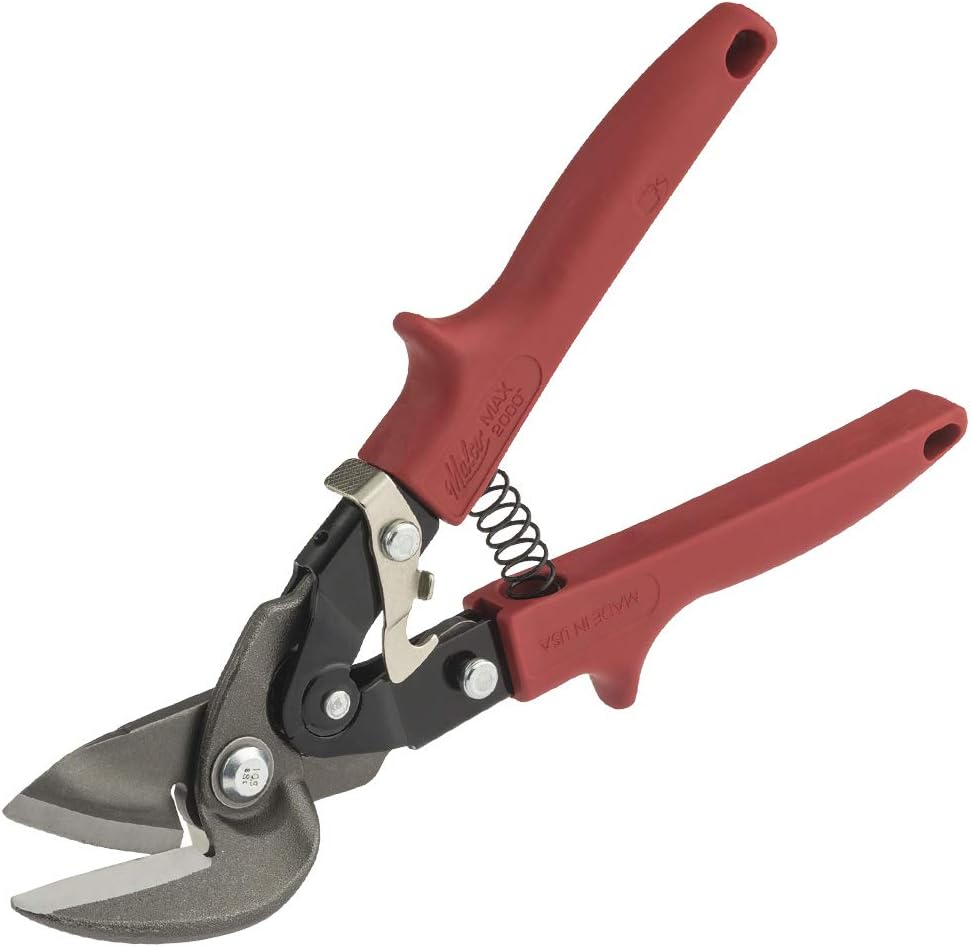
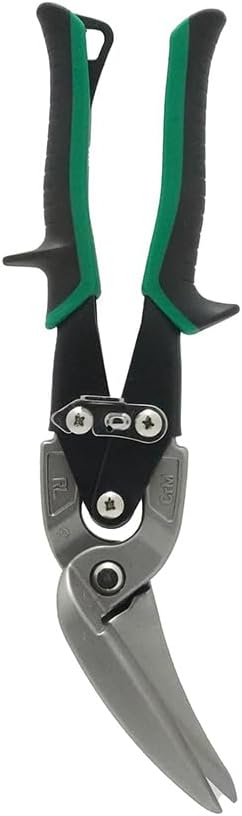
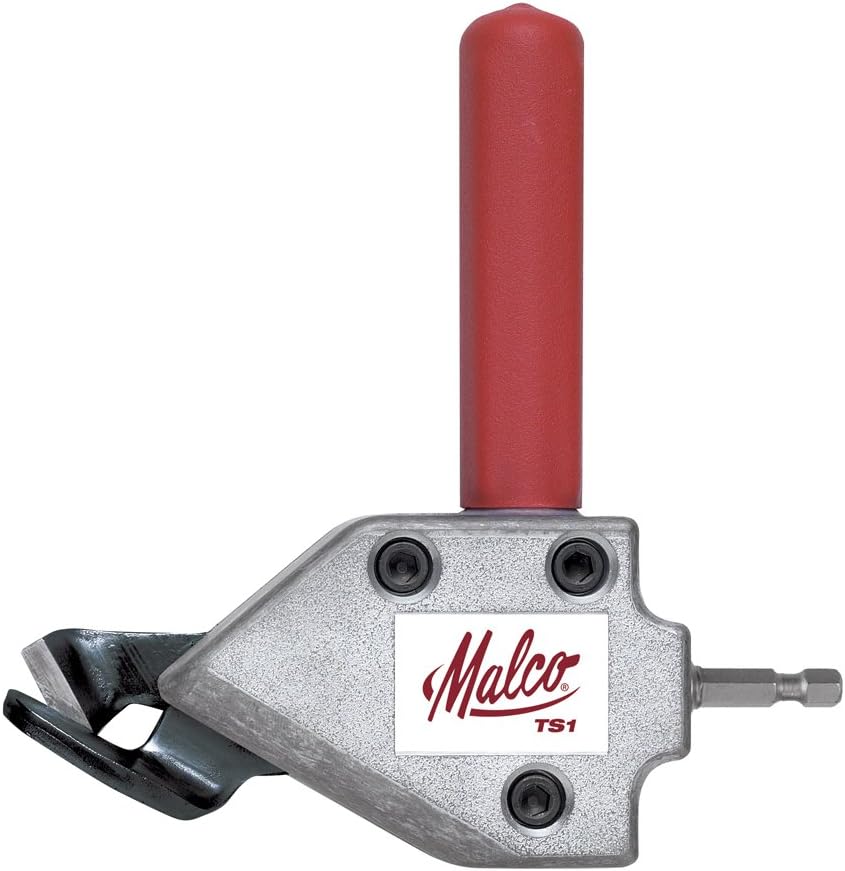
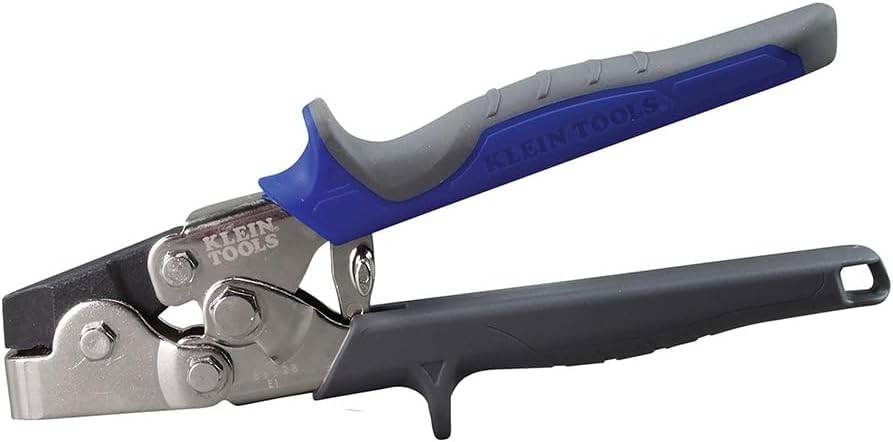
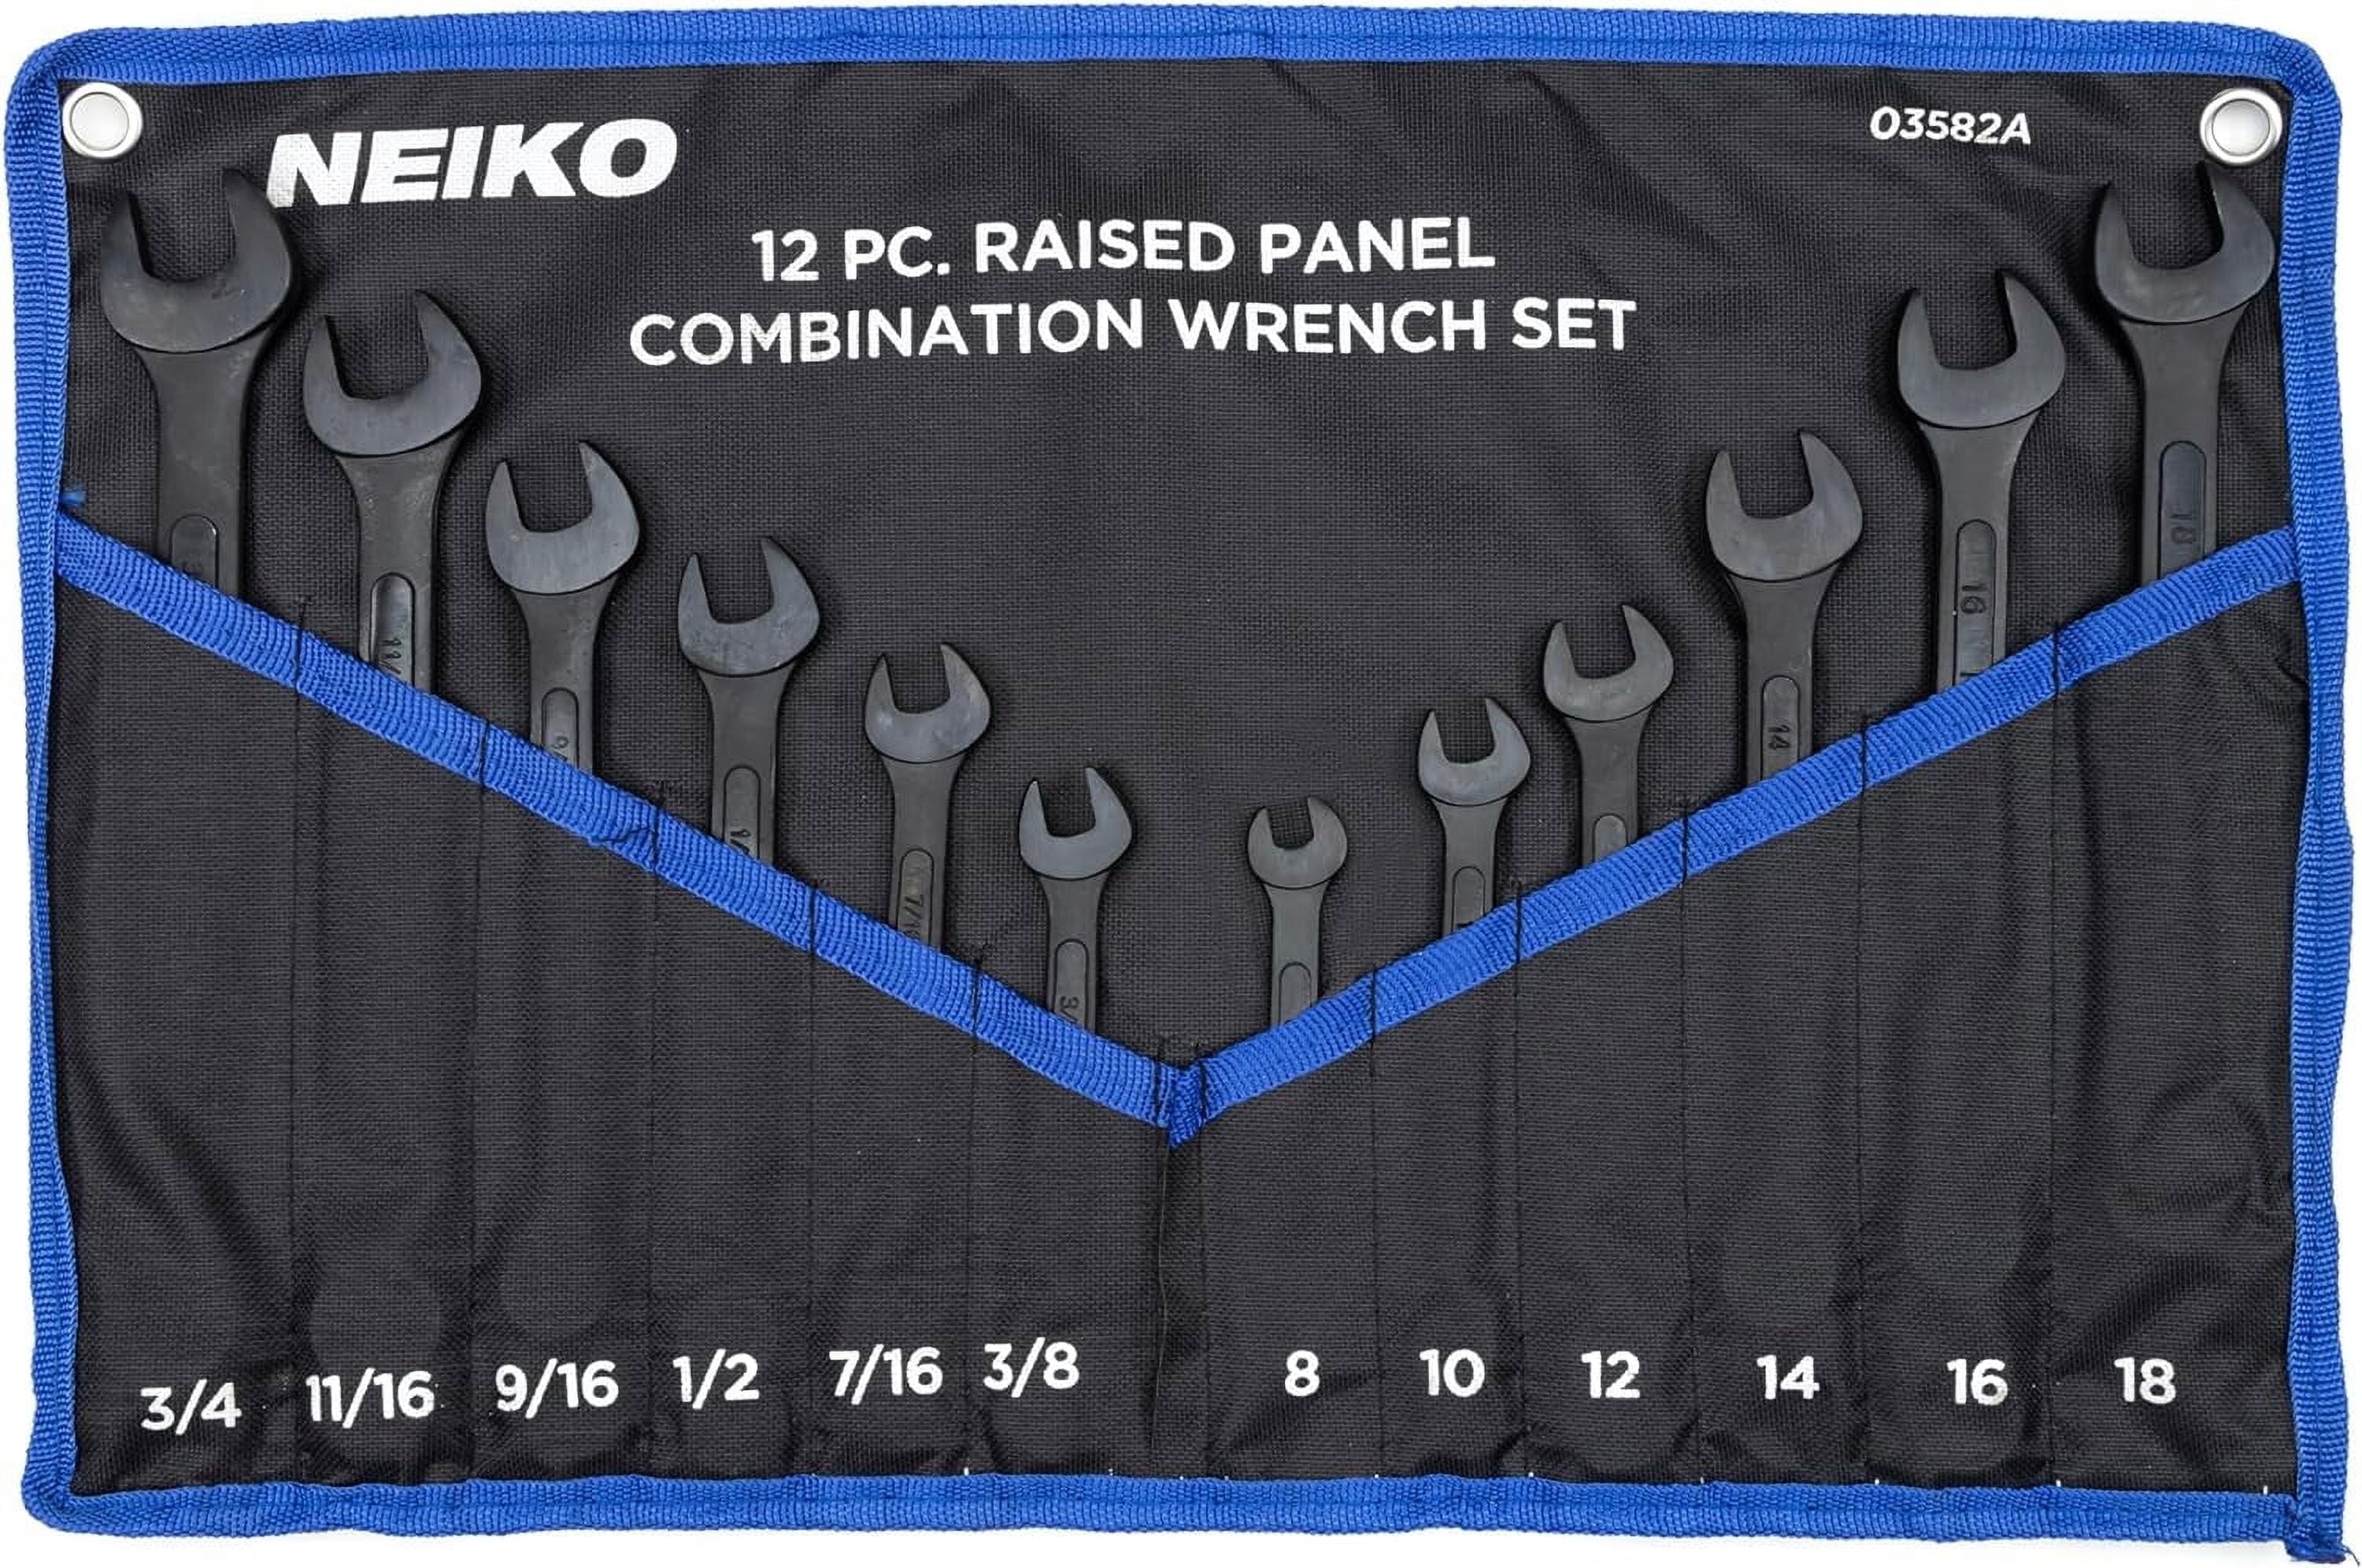
As an Amazon Associate, TestTalkHQ earns from qualifying purchases.