Parting & Cutoff Troubleshooting
Diagnose blade breaks, chatter, rubbing, and pip leftovers when the calculator RPM already looked correct
Not a restatement of setup theory. Pair this with the Parting & Cutoff Calculator when speed/feed looked green but the blade still failed. For blade selection, height setup, and SFM basics, use the Parting Off Guide. This page stays on field diagnosis forks the guide only sketches.

Parting Problems Quick Answer
Use this when the calculator RPM matched the guide SFM table and you still broke a blade, squealed without a chip, or left a center pip that ruins the face.
| Problem | What it usually means | First fix | Next tool |
|---|---|---|---|
| Blade snaps at first engagement | Height off center, toolpost loose, or overhang too long | Stop; re-set center height; shorten stick-out; re-torque post | Parting Off Guide |
| Blade breaks mid-groove in steel/SS | Heat + low feed rubbing; fluid starved deep in cut | Flood fluid; raise feed slightly; drop RPM 25% | Parting Calculator |
| Squeal, smoke, no chip | Rubbing — height, dull edge, or feed too low | Verify height; sharpen/replace; increase IPR | Parting Off Guide |
| Chatter that speed changes won’t kill | Rigidity: overhang, loose post, or wrong blade type | Shorten blade; tighten; consider rear toolpost / HSS | Lathe Turning Troubleshooting |
| Center pip / uneven face | Height high/low or feed dies near center | Re-set height; keep feed into center; face pip off | Parting Calculator |
1. Blade Breaks at First Engagement — Height and Rigidity, Not RPM
What it looks like: You dial the calculator RPM, start the cut, and the blade snaps or chips before a groove forms. Scrap piece shows a nick, not a parted face.
Likely causes: Tool above/below center so the clearance face hits first and side-loads the blade. Toolpost or compound not locked — the post nods under load. Blade overhang far past the holder. Carbide insert on a flexible manual setup that digs then fractures. Starting feed slammed in instead of eased to establish a chip.
Fixes: Re-set height against a dead center or known center reference before chasing SFM. Shorten stick-out to the minimum that clears the stock. Torque the toolpost. On manual lathes with any flex, prefer HSS until the setup proves rigid. Ease into the cut, then hold steady IPR. Re-check numbers in the Parting & Cutoff Calculator only after height and overhang are fixed — RPM will not save a crooked setup.
2. Blade Breaks Mid-Groove — Heat, Rubbing Feed, and Fluid Starvation
What it looks like: Groove starts fine. Halfway to center the blade squeals, tip glows, then snaps — classic in stainless and alloy steel.
Likely causes: Feed too low so the edge rubs and work-hardens the groove floor. Cutting fluid brushed once at the start, then dry at depth. RPM still near turning SFM for the diameter. Chip welded to the rake face. Pecking never used on deep grooves.
Fixes: Stop before another blade dies. Reduce RPM ~25% from the calculator start point on deep steel/SS. Raise feed slightly so you see a continuous chip. Flood or squirt fluid into the groove for the whole cut. Peck: advance, retract a few thousandths to clear chips/heat, advance again. If stainless already work-hardened, you may need to skim the groove wall or start a new groove beside it — do not force the glazed face.
Numbers first, then heat management. Recalculate for diameter, then cut RPM further for deep grooves.
Parting Calculator3. Squeal, Smoke, No Chip — Rubbing Diagnosis
What it looks like: Spindle turning, blade in contact, noise and heat, but no chip curl. Surface glaze appears fast on stainless.
Likely causes: Off-center height. Dull HSS or chipped carbide. Feed so light the edge burnishes. RPM so high the edge never bites. Wrong rake for the material after a bad grind.
Fixes: Back out immediately on stainless — rubbing creates a hardened skin. Verify height. Sharpen or replace the edge. Increase IPR into the recommended band (HSS steel often ~0.001–0.003 IPR). Confirm calculator RPM is parting SFM, not turning SFM. Only then re-enter the cut with fluid.
4. Chatter That Won’t Die — Rigidity Loop
What it looks like: Harmonic buzz in the groove; finish shows regular ridges; blade edges freckle or crack. Changing RPM up or down only moves the pitch.
Likely causes: Overhang, loose post, skinny blade in large diameter, carbide on a flexible machine, or workpiece sticking too far from the chuck jaws. Increasing RPM to “get past chatter” makes it worse.
Fixes: Shorten blade and workpiece stick-out. Tighten everything. Drop RPM; keep or slightly raise feed. Switch to HSS if carbide keeps chipping. Rear toolpost (inverted blade, reverse spindle) changes force direction — use when your lathe supports it. For general lathe vibration outside parting, see Lathe Turning Troubleshooting rather than duplicating turning diagnosis here.
5. Center Pip and Bad Cutoff Face — Height and Feed Fade
What it looks like: Part drops with a nipple at center, or the face is concave/convex. Micrometer on the face shows a high spot.
Likely causes: Tool high or low so geometry leaves a pip. Feed lightened near center out of fear of grabbing. Blade flexed and walked. Stopping short and breaking the last web by hand.
Fixes: Re-set on-center height. Keep steady feed into the center; support the free end with a cloth catch so you are not yanking the cut. Face the pip off as a second operation if needed. Measure with a micrometer when the face is a sealing or bearing surface — do not assume “it parted” means “it is square.”
6. Chip Packing and Grab Near Breakthrough
What it looks like: Groove fills with stringy chips; blade binds; parting piece grabs and spins in the chuck or bends the blade at breakthrough.
Likely causes: No pecking on deep grooves. Wrong chipbreaker geometry on insert blades. Part not supported/caught at breakthrough. Spindle speed still high when the web is thin.
Fixes: Peck to clear chips. Brush chips out of the groove. Slow RPM for the last 1/8 in. Catch the part — do not let a long cutoff whip. If diameter or material keeps packing despite good technique, saw-to-length may be the safer fork (already covered in the guide).
Decision Forks Already Covered — Cross-Link
Article 3 SKIPPED for this cluster. HSS vs carbide insert blades and parting-vs-sawing already live in the Parting Off Guide and on the calculator page. Use those instead of a duplicate comparison post. Chart SKIPPED — SFM/IPR tables already sit in the calculator and guide without unique standalone chart data.
Parting Off Guide → Parting Calculator → Lathe Turning Troubleshooting →
Recommended Tools for Parting Diagnosis
Five CSV catalog picks with verified images — fluid, measurement, height checks, and PPE
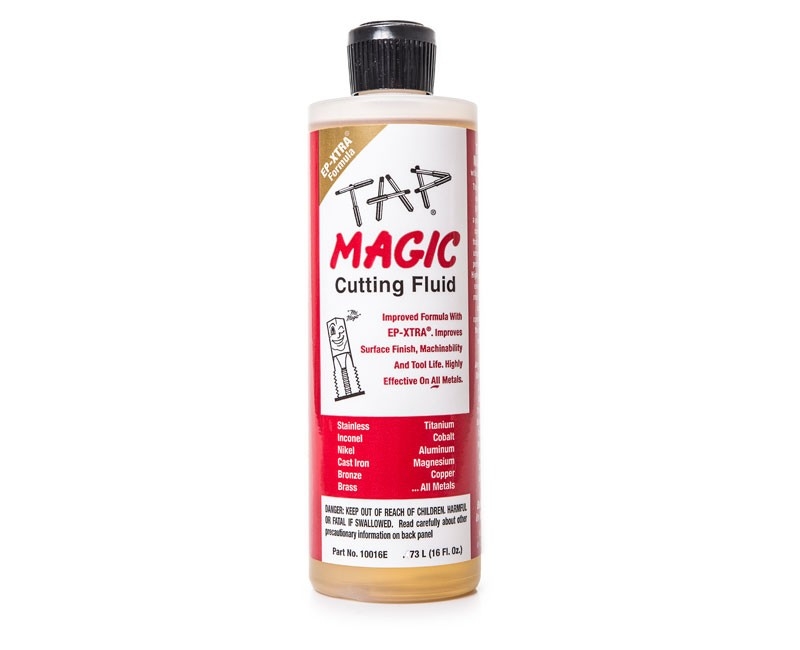
Tap Magic EP-Xtra Cutting Fluid
- Keep steel/SS parting grooves wet
- Cut heat that causes mid-groove snaps
- Brush or nozzle into deep cuts
- Cutting Tools / Machining catalog
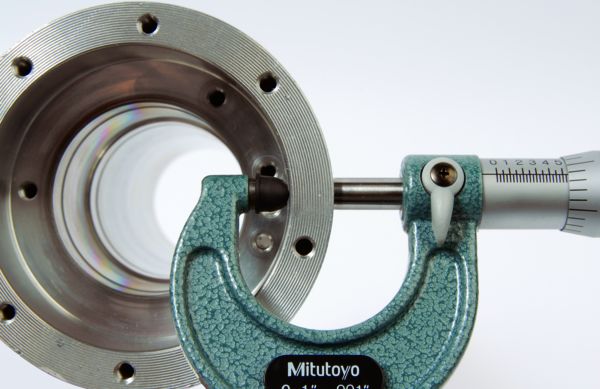
Mitutoyo 103-177 Outside Micrometer, 0–1"
- Check pip height and face thickness
- Confirm parted length before release
- 0–1" shop standard
- Cutting Tools / Machining catalog
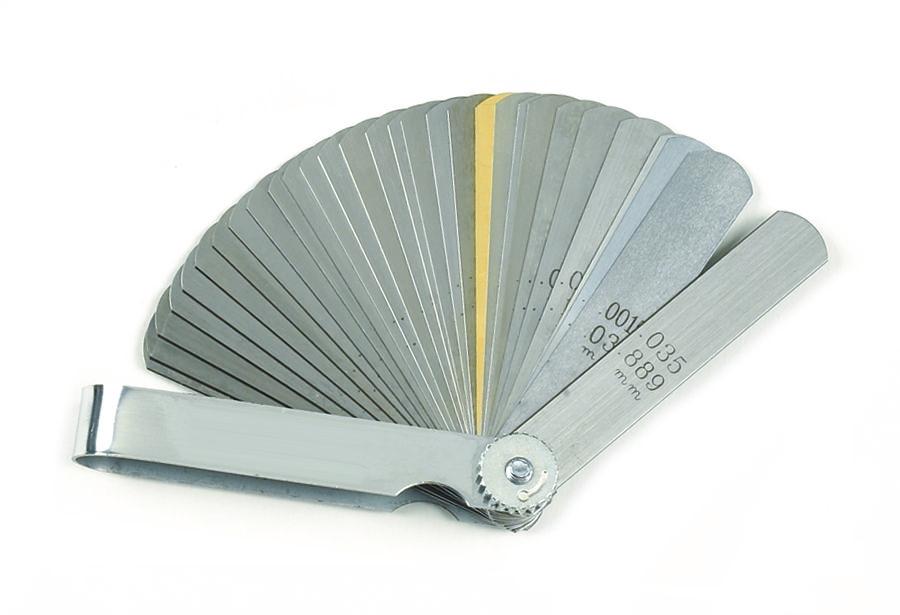
GEARWRENCH 161D 32-Blade Feeler Gauge Set
- Shim/check tool height vs center
- Quantify “a little high/low”
- Useful before blaming RPM
- Hand tools catalog
Klein Tools 60171 Safety Glasses Anti-Fog 2-Pack
- Chip and fluid splash protection
- Anti-fog for wet parting cuts
- Keep a spare pair at the lathe
- Safety catalog
Mechanix Wear The Original Hi-Viz Work Gloves
- Safer part catch at breakthrough
- Grip on oily stock
- Hi-viz around rotating work
- Safety catalog
As an Amazon Associate, TestTalkHQ earns from qualifying purchases. All five cards are sourced only from the affiliate CSV with verified images. Catalog gaps flagged by name: Lathe Grooving/Parting Tool Holder MGEHR1212-3 with 10 Carbide Inserts (row 288) — no Product Image URL; AUNMAS MT2 Live Center (row 315) — no product image yet (skipped); Starrett Electronic Slide Caliper EC799A (row 100) — no Product Image URL; Permatex Anti-Seize (row 139) — no Product Image URL. Note: Tap Magic CSV lists 16 oz while the hosted image shows a 4 oz EP-Xtra bottle of the same product line — confirm size on the live Amazon listing.
Frequently Asked Questions
The calculator RPM matched the guide — why did the blade still break?
RPM assumes height, overhang, fluid, and feed are already correct. Start-of-cut snaps are usually setup; mid-cut snaps are usually heat/rubbing. Diagnose when it failed before changing SFM again.
Should I always drop RPM 25% from the calculator?
Use the calculator as the start point. Drop further for deep steel/SS grooves, large diameters, or chatter. Do not drop RPM to mask an off-center tool.
Is this the same as the parting guide troubleshooting section?
No. The guide summarizes common causes. This page splits failures by when/how they present and gives field differentials (start vs mid, chip vs no chip, pip vs chatter).
When should I saw instead of part?
Large diameter, chronic chatter, or stock that work-hardens under any rub — see the parting-vs-saw section in the Parting Off Guide rather than a new comparison article.
Why no dedicated parting blade product card?
The best CSV match (MGEHR1212-3 parting/grooving holder) has no product image URL yet — flagged as a catalog gap instead of shipping a mismatched photo.