
Welding Reference Card
One page. MIG, TIG, stick and flux core settings by thickness.
$3.99
BuyWall thinning, ovality, inside-radius wrinkling, springback errors, and mandrel/die mismatches
Estimate bend allowance, springback, and wall stress with the Tube Bending Calculator. Learn mandrel selection and D/t ratios in the Tube Bending Guide. Shop and fab tools: Shop Safety & Tools Hub.

Use this when bends collapse, wrinkle on the inside, spring open past layout, or wall thickness fails inspection after bending.
| Symptom | What it usually means | First fix | Next tool |
|---|---|---|---|
| Outside flat, inside wrinkled | Compression on ID — no mandrel or tight CLR | Add mandrel; increase centerline radius | Tube Bending Calculator |
| Wall thin at extrados | Excessive stretch for D/t ratio | Larger bend radius or thicker wall tube | Tube Bending Guide |
| Tube oval after bend | Insufficient wiper or wrong die groove | Match die to OD; check pressure die | Tube Bending Calculator |
| Angle opens after release | Springback underestimated | Over-bend or apply correction factor | Tube Bending Guide |
What it looks like: Outside wall of the bend thins measurably (ultrasonic or cut section), tube goes oval instead of round, or pressure rating drops below spec after forming.
Likely causes: Stretch on the extrados exceeds material limit — tight bend radius relative to OD (low D/R), thin wall (high D/t), or over-clamping without mandrel support. Aluminum and copper thin faster than steel at the same D/t.
Fixes: Increase centerline radius, step up wall thickness, or use a mandrel/wiper stack sized for the tube. Verify predicted thinning in the Tube Bending Calculator before cutting production lengths.
What it looks like: Ripples or folds on the intrados (inside) of the bend, sometimes visible only after paint. Bend may kink instead of flowing smoothly.
Likely causes: Compressive instability on the inside — bending without mandrel on thin-wall tube, CLR too tight, or insufficient pressure-die force. Material buckles instead of flowing.
Fixes: Use a mandrel with correct ball count and linkage for the CLR, add wiper die if needed, increase bend radius. The Tube Bending Guide maps D/t to mandrel requirement.
What it looks like: Bend opens 2–15° after removing from the machine; fixtures don't fit; opposite bends don't mirror. Repeat bends drift angle batch to batch.
Likely causes: Elastic recovery depends on yield strength, bend radius, and wall thickness. Using a steel springback factor on stainless or aluminum guarantees error. Over-bend amount not validated on scrap.
Fixes: Apply material-specific springback from the calculator, trial on coupon, record machine-specific correction. Heat on some alloys changes springback — keep process consistent.
What it looks like: Mandrel sticks or drags, scratches ID, leaves witness marks, or tube slips in groove — combined with wrinkling or flattening depending on which component is wrong.
Likely causes: Die groove too wide (slip) or too narrow (pinch/oval). Mandrel ball count too few for CLR — can't reach tangent point. Plug mandrel used where linked ball mandrel is required for thin wall.
Fixes: Match die groove to actual measured OD (not nominal), select mandrel type per D/t table in the guide, lubricate ID appropriately. Measure tube OD with calipers — mill tolerance affects fit.
Wall thinning, wrinkling, and springback interact — fix mandrel/die first, then refine springback on coupons.
Tube Bending Calculator → Tube Bending Guide → Shop & Fab Hub →
One page. MIG, TIG, stick and flux core settings by thickness.
$3.99
Buy
19 pages. Four processes, stainless and aluminum, symbols and inspection.
$12.99
Buy
Price the job, then hand over a quote with no internal numbers.
Excel or Google Sheets. Best on a computer.
$29.00
Buy
Card, 19-page guide and the estimator workbook. All six files.
Excel or Google Sheets. Best on a computer.
$34.99
$45.98 if bought separately — save $10.99
BuyCheckout opens in a new tab.
Five CSV catalog picks with verified images — controlled torque, cutting fluid, quality taps, and precision measuring
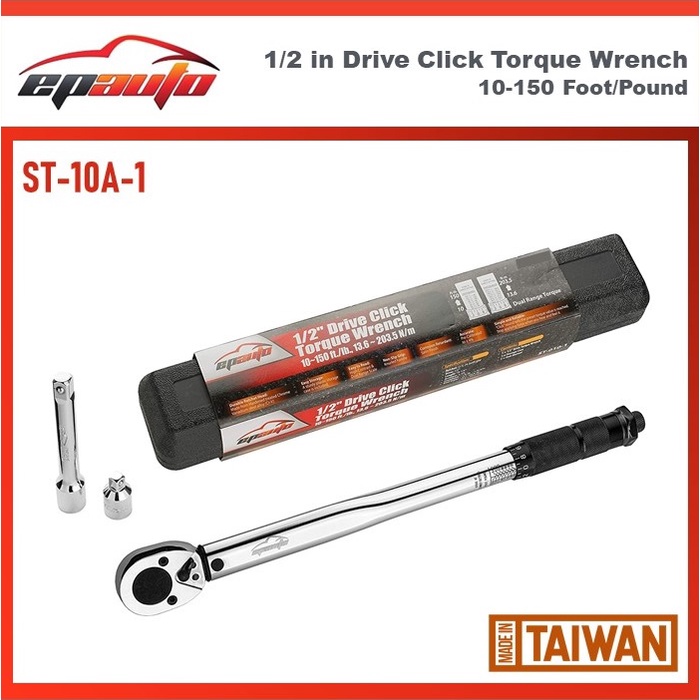
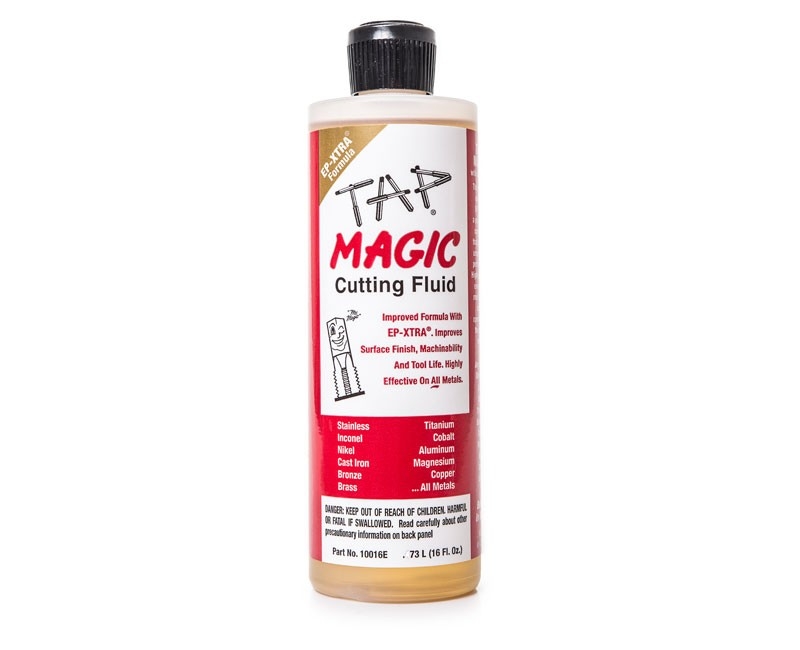
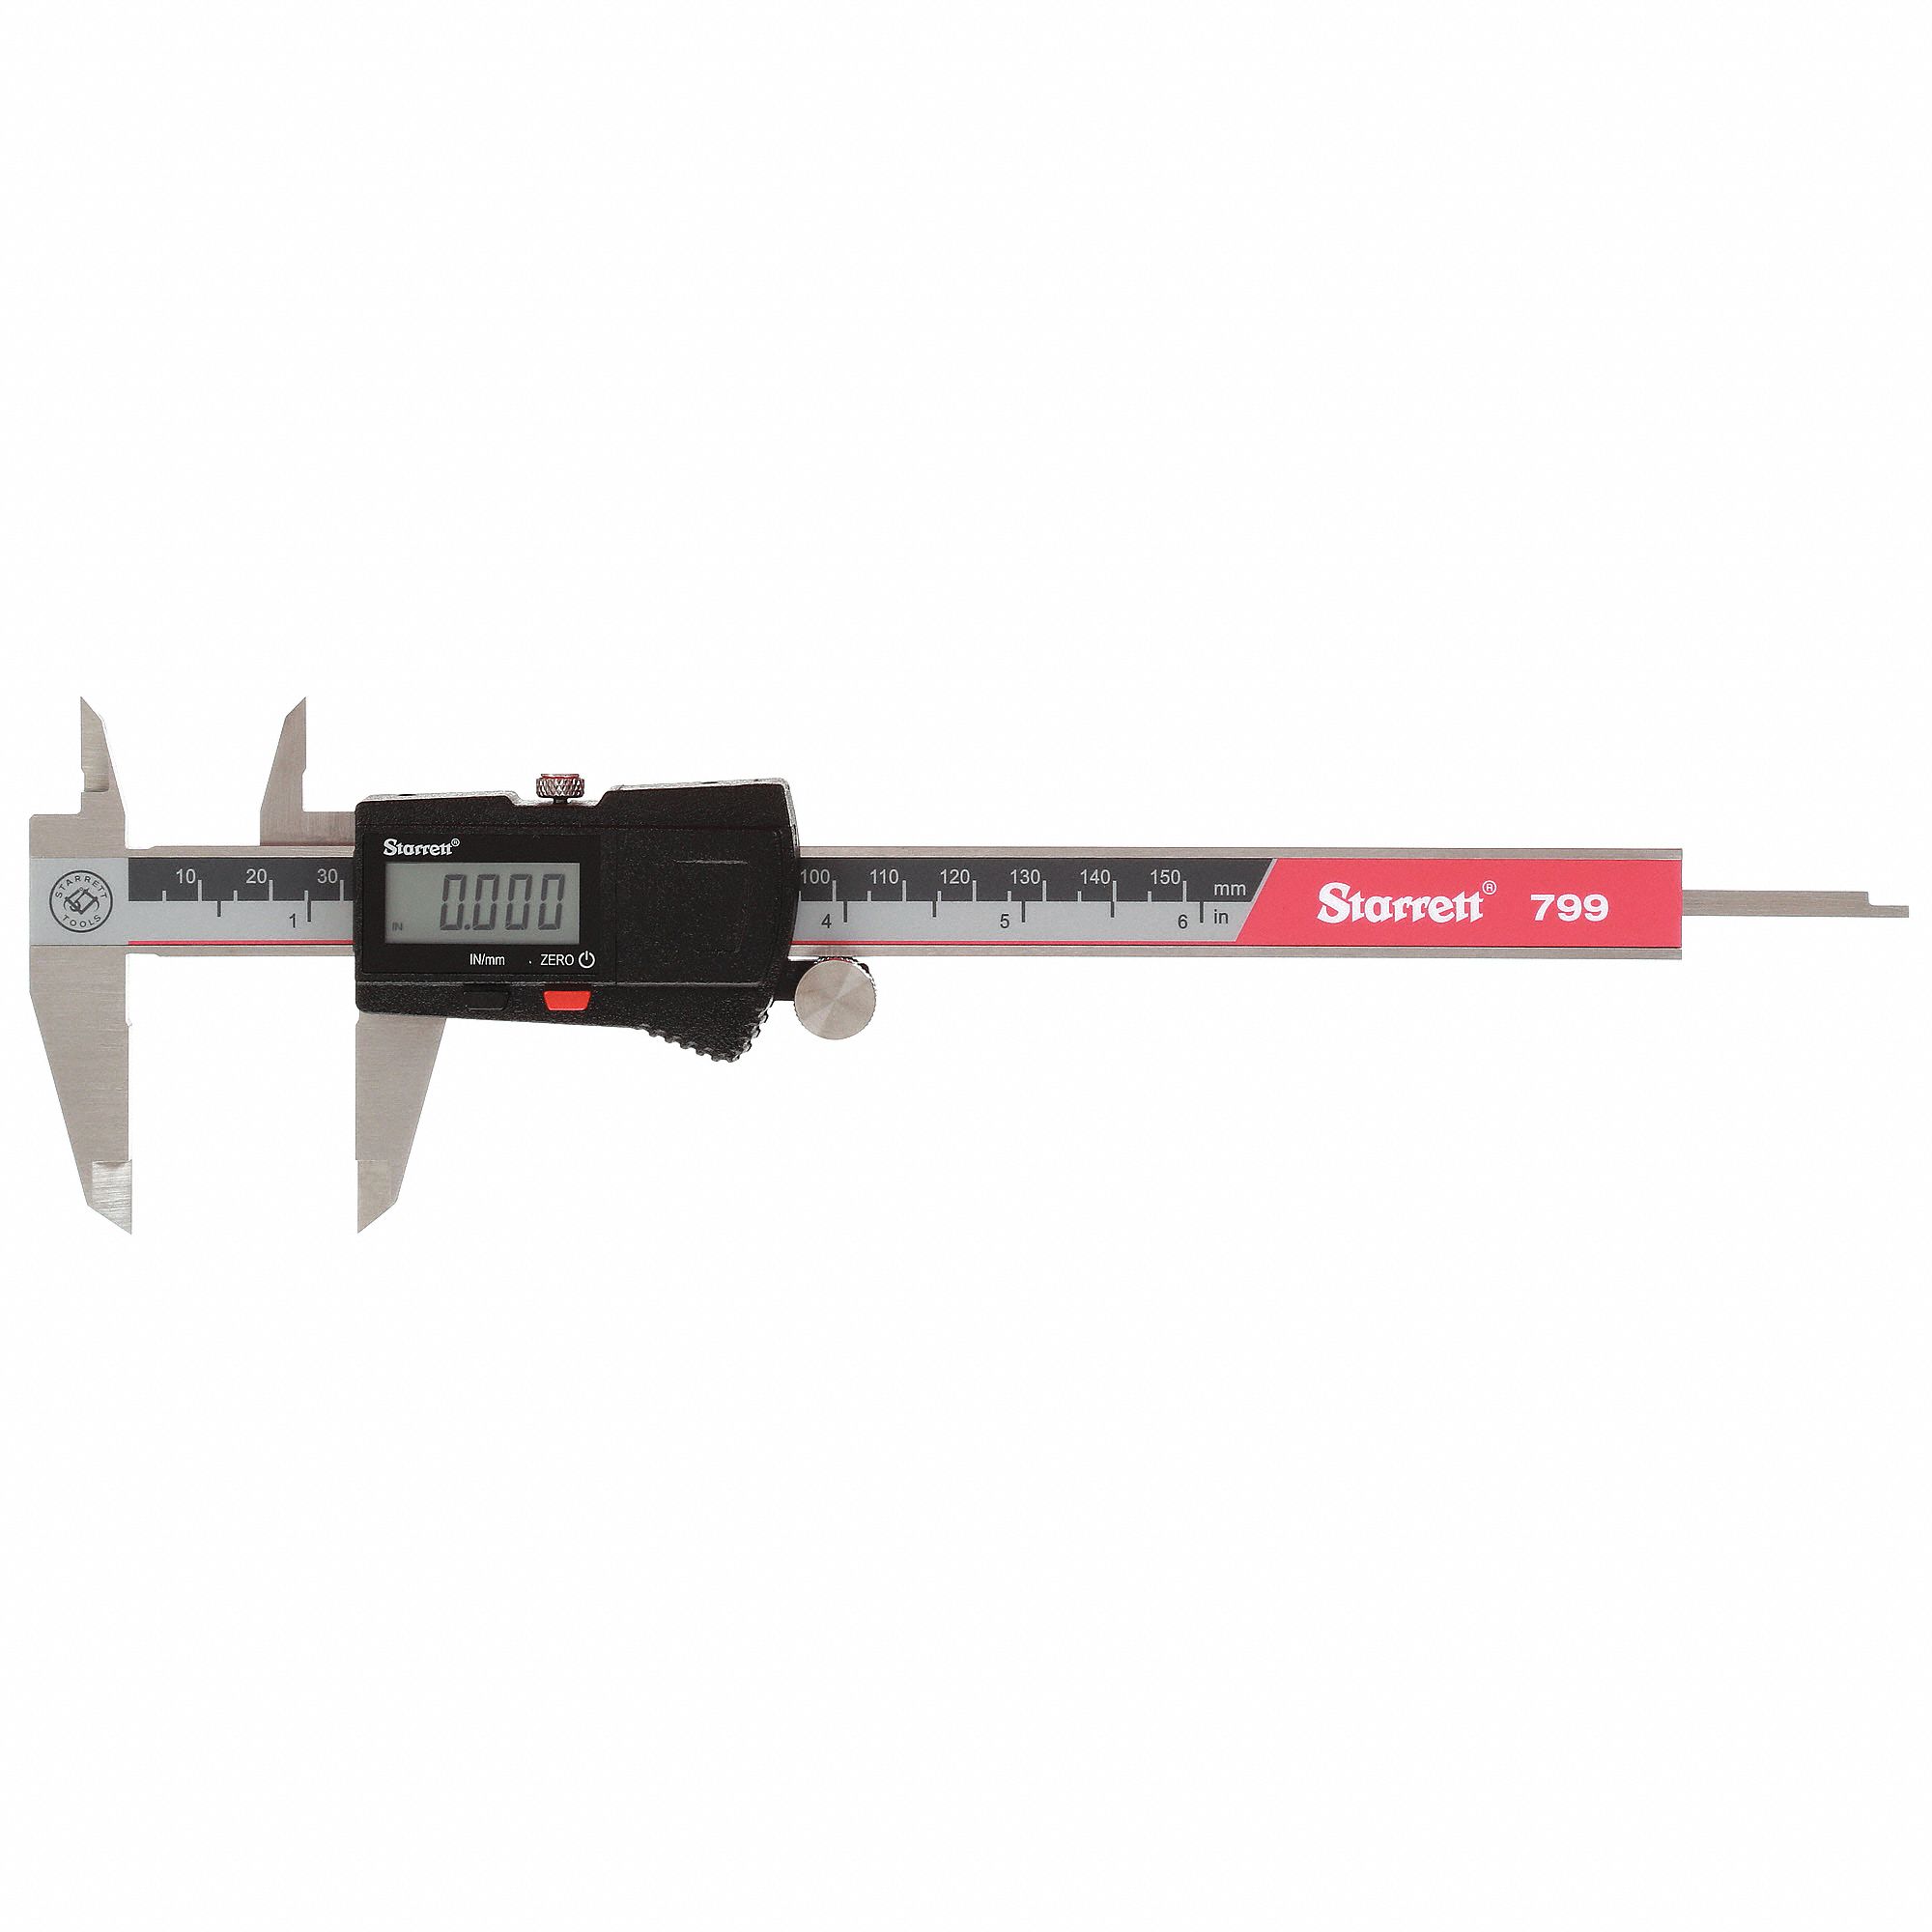
As an Amazon Associate, TestTalkHQ earns from qualifying purchases. All five cards are sourced only from the affiliate CSV with verified product images.
Generally when D/t exceeds practical limits for the bend radius — thin wall and tight radius almost always need mandrel support.
Springback — elastic recovery. Over-bend by a material-specific correction.
Annealing lowers yield and changes springback; recalculate and re-qualify on scrap.
Wrong die groove, insufficient pressure die force, or wall thinning without ID support.
Ultrasonic wall gauge on the extrados, or destructive section on first article.