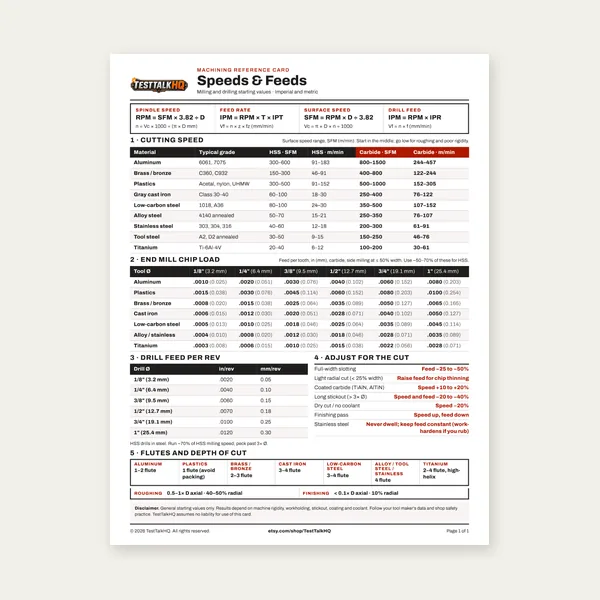
Machining Speeds & Feeds Card
One page. Speeds, chip load and drill feed, imperial and metric.
$3.99
BuySolid carbide vs indexable vs boring head vs anti-vibration (damped) bars — rigidity, adjustability, cost, and when each wins
The guide names the types. This page is the decision fork: which class to buy or pull from the cabinet for a bore diameter, depth, and tolerance. Pair with the calculator after you pick the tool.

Best for: Small bores, short-to-medium overhang, high stiffness per diameter, shops that want a simple one-piece tool.
Pros: Maximum rigidity for a given shank size; excellent for miniature and precision short bores.
Cons: Tip geometry is fixed or brazed; less economical when edges die often; not the first pick for frequent grade changes.
Best for: Everyday lathe boring above roughly 0.5" where insert grades change by material.
Pros: Swap CCMT/DCMT/etc. without changing the bar; lower long-run insert cost; shop-standard tooling.
Cons: Pocket and clamp add a little compliance vs solid; still limited by L/D like any undamped bar.
One page. Speeds, chip load and drill feed, imperial and metric.
$3.99
Buy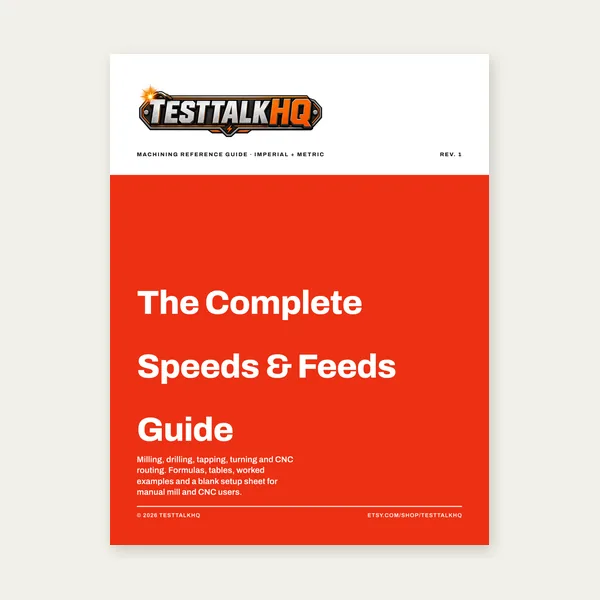
27 pages. Milling, drilling, tapping, turning and CNC routing.
$12.99
Buy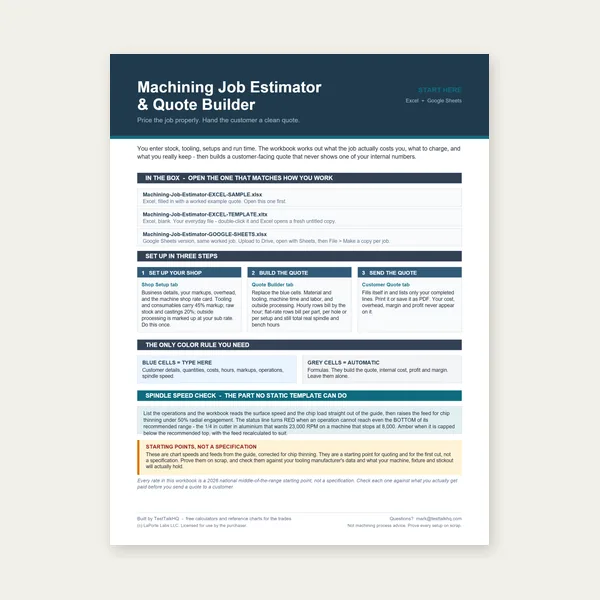
Quote shop work and check operations against your spindle's top speed.
Excel or Google Sheets. Best on a computer.
$29.00
Buy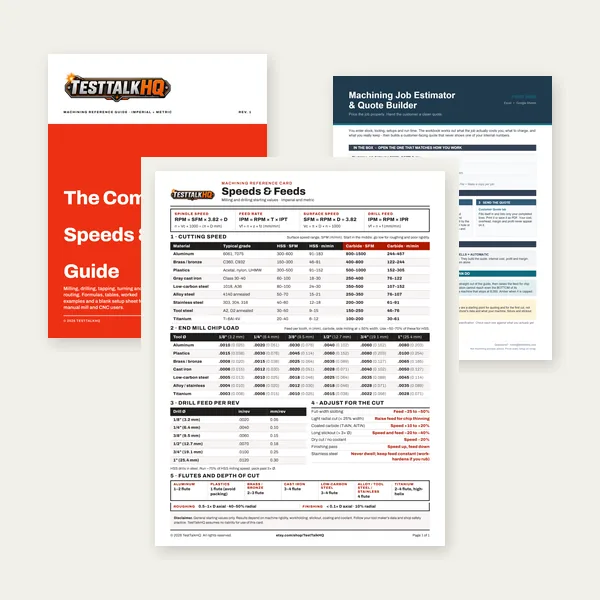
Card, 27-page guide and the estimator workbook. All six files.
Excel or Google Sheets. Best on a computer.
$34.99
$45.98 if bought separately — save $10.99
BuyCheckout opens in a new tab.
Five lathe/boring picks from the TestTalkHQ affiliate catalog — indexable sets and SCLCR bars matched to the type decision
As an Amazon Associate, TestTalkHQ earns from qualifying purchases. Indexable bars win on insert flexibility; damped bars still win when L/D must exceed ~4:1.
Best for: Work on a mill, offset holes, parts too large to chuck, or when you must dial diameter finely without changing inserts.
Pros: Micrometer-style diameter adjustability; flexible setups.
Cons: More joints → less rigidity than a short solid bar; not a substitute for a lathe boring bar on deep chucked work when a lathe is available.
FAQ crossover: mill vs lathe boring choice also appears in the guide FAQ.
Best for: Real deep bores where L/D must exceed ~4:1 and you cannot shorten stick-out.
Pros: Internal damper extends stable reach toward 7:1–10:1 class performance.
Cons: Cost; still fails if setup is loose, tip off-center, or DOC absurd; not magic for chip pack.
If the symptom is chatter at long overhang, diagnose first: Boring Bar Troubleshooting.
| Job signal | Lean toward | Why |
|---|---|---|
| Bore < ~0.5", short stick-out | Solid carbide | Stiffness per diameter |
| Production lathe, insert changes often | Indexable | Grade flexibility / cost |
| Mill, offset hole, dial diameter | Boring head | Adjustability on spindle |
| Depth forces L/D > 4:1 | Damped bar | Resonance control |
| Tight IT grade on shallow bore | Solid or quality indexable + spring passes | Fewer joints, better repeatability |
Only if you can shorten stick-out or upsize diameter. Undamped indexable bars still obey L/D physics.
Usually no — heads belong on mills. Use a lathe boring bar when the work swings in a chuck.
For tiny stiff setups, often yes. For production insert economy above mid sizes, indexable usually wins.
Calculator and chart — type choice does not replace SFM/IPR setup.